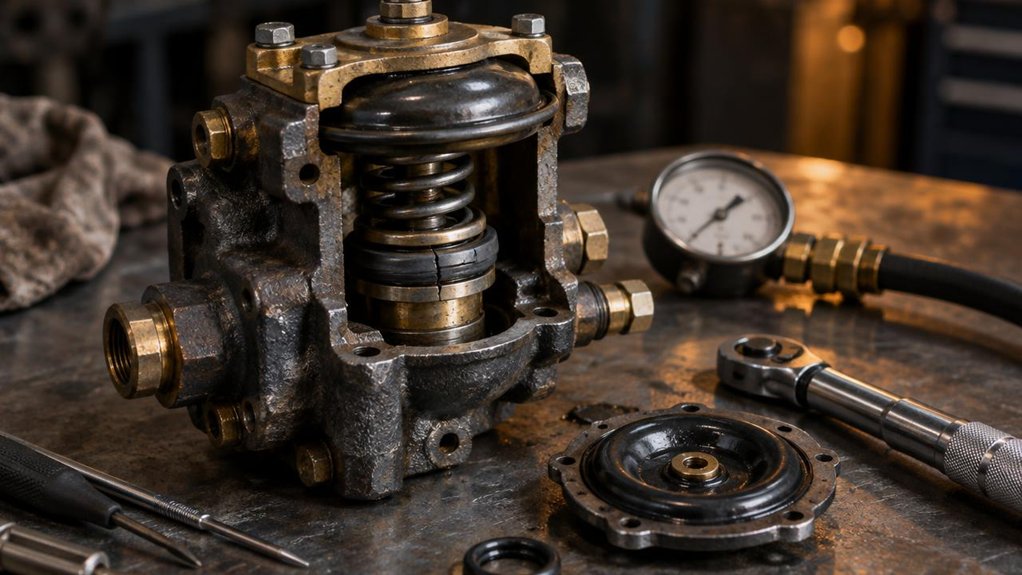
Locomotive Brake Valve Assembly Diagnostic Steps and Failure Modes

Locomotive Brake Valve Assembly Diagnostic Steps and Failure Modes

Locomotive crews and maintenance teams often struggle to find the source of brake valve faults.

Symptoms like slow application, sluggish release, and gradual pressure loss can mimic each other.

Guessing wastes time and risks running with a compromised brake system.

A disciplined, step-by-step approach isolates the fault faster.

Common problems in brake valve diagnosis:

  • Brake application is slow or uneven across the consist.
  • Brake release is sluggish after a full application.
  • Brake pipe pressure drops faster than the allowable limit.
  • Small air leaks are difficult to locate by sound alone.
  • Solenoid valves fail to energize or remain stuck.
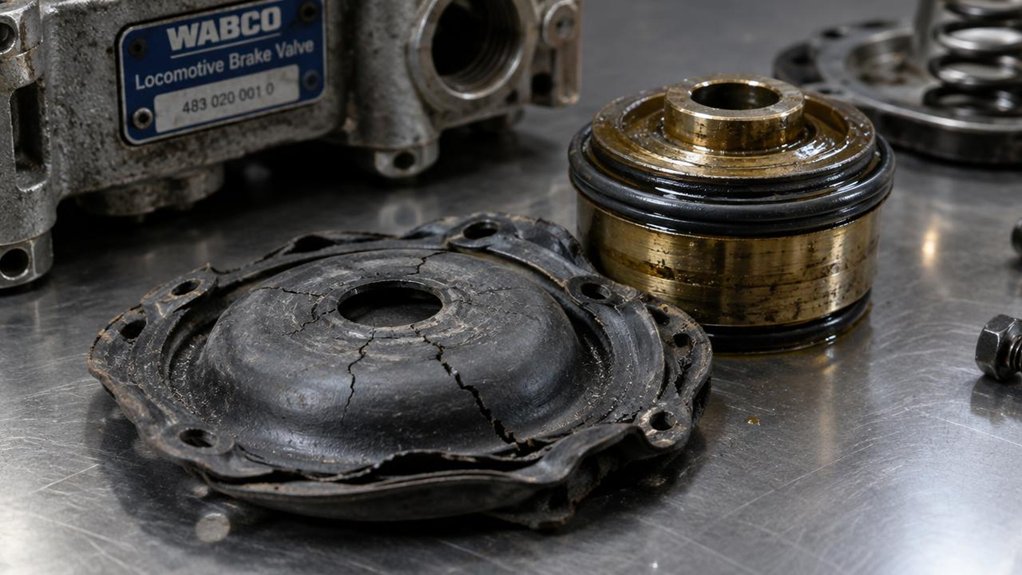
  • Diaphragms show hardening, cracking, or swelling.
  • Gauge readings change after the system is charged.
  • The decision to rebuild or replace the assembly is unclear.

Symptom-to-cause reference table:

SymptomLikely CauseFirst CheckCorrective Action
Slow applicationRestricted supply passage or worn diaphragmReservoir pressure and diaphragm conditionClean passages; replace diaphragm
Sluggish releaseSticky solenoid or restricted exhaust pathSolenoid response and exhaust flowClean or replace solenoid
Excess brake pipe leakageLoose fitting or damaged gasketSoapy water test on all jointsTighten or replace fitting or gasket
Gauge reading mismatchFaulty gauge or leaking gauge lineCompare against a calibrated reference gaugeReplace gauge or repair line
Repeated pressure lossSeat or seal damage inside the valveLeak test under full chargeRebuild with genuine kit or replace assembly

Step-by-Step Diagnostic Sequence

Follow this sequence to avoid misdiagnosis.

Each stage depends on the one before it.

Step 1: Drain the reservoirs.

Drain both main reservoirs completely.

Confirm that both gauges read zero.

Step 2: Charge and test the brake pipe.

Charge the brake pipe.

Run an air leak test against the allowable drop limit in the maintenance specification.

Step 3: Inspect every fitting.

Apply soapy water to every fitting, joint, and gauge connection.

Small seepage often stays silent until tested.

Step 4: Run application and release checks.

Perform application and release checks only after all leak tests pass fully.

Step 5: Evaluate the failure mode.

Worn diaphragms and sticky solenoids cause most symptoms.

Inspect these components first.

Rebuild or Replace Decision

Rebuild the assembly when the body is sound.

Wear limited to seals, diaphragms, and gaskets usually justifies a rebuild.

Replace the assembly when the casting is cracked.

Replace it when the bore is scored or the valve fails after repeated rebuilds.

Use genuine rebuild kits for consistent fit and performance.

Mikura International supplies genuine WABCO locomotive brake valve parts, rebuild kits, and complete assemblies. We also supply genuine locomotive parts for ALCO, EMD, and GE platforms.

Key Takeaways

  • Perform the residual pressure check first and drain main reservoirs until both gauges read zero.
  • Run the air leak test at specified brake pipe pressure, then isolate leaks with soapy water on every fitting.
  • Common failure modes include worn or ruptured diaphragms, leaking graduating or relay valve seats, and contaminated passages.
  • Sticky solenoid valves holding exhaust or supply paths open are a high-frequency cause of brake malfunctions.
  • Rebuild worn pistons or cracked diaphragms, but replace valves with housing cracks, warped surfaces, or repeated failures.

Warning Signs of a Failing WABCO Brake Valve
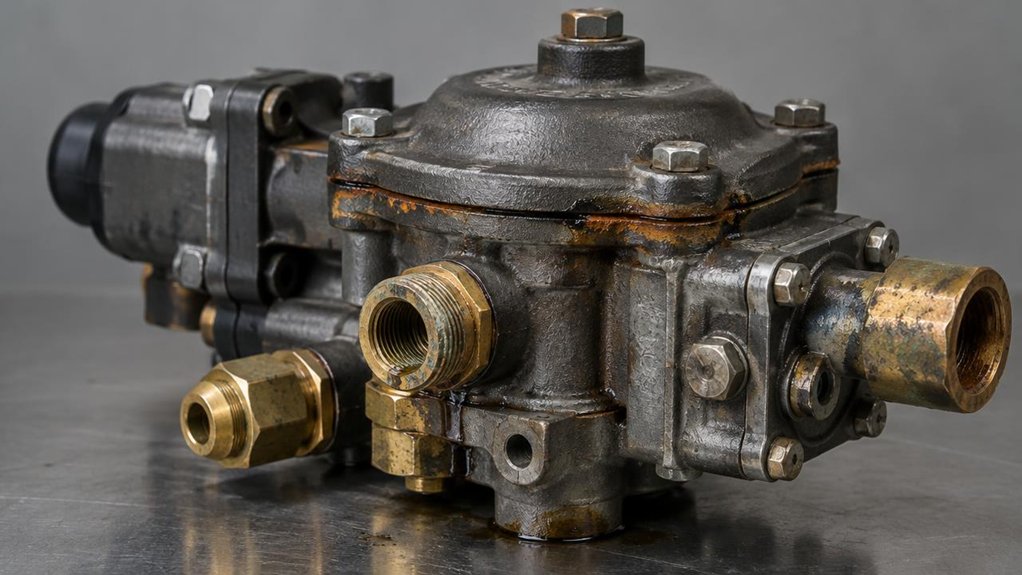
Warning Signs of a Failing WABCO Brake Valve

Before a WABCO brake valve fails outright, it usually shows measurable symptoms during a routine brake test. You’ll spot the earliest clues during the locomotive’s service application. Watch the brake pipe gauge closely. If it drops faster than the specified rate, suspect air pressure loss at the valve or its connections. Don’t dismiss it as a gauge fault until you’ve verified it.

Next, check for intermittent brake behavior across the train. Brakes that apply on one stop but fail to release on the next need immediate attention. A sticking relay valve or a worn graduating piston seal is a likely cause. Listen for exhaust hissing from the valve body during release. Any audible leak at the exhaust port is a serious defect. Do not defer the repair.

Log each occurrence with the time, speed, and brake pipe pressure reading. This record makes patterns easier to identify. Compare those entries against the previous test to confirm a developing trend. Mikura International supplies genuine WABCO brake valve parts for locomotive operators.

How the WABCO Valve Assembly Works

Your locomotive’s WABCO valve assembly converts brake pipe pressure changes into a proportional brake cylinder response. Its operation is rooted in basic air system principles. Compressed air from the main reservoir charges the brake pipe. Brake pipe pressure sets the control state of the system.

Your locomotive’s WABCO valve assembly converts brake pipe pressure changes into a proportional brake cylinder response. Compressed air from the main reservoir charges the brake pipe, and that pressure sets the system’s control state.

When you reduce brake pipe pressure, the equalizing portion senses the drop. It then shifts the relay valve, which routes reservoir air to the brake cylinders. Larger reductions produce greater brake cylinder pressure. The feed valve restores brake pipe pressure once the reduction stops.

Understanding valve operation principles helps you interpret gauge readings during testing. Stay alert. A sluggish response or uneven braking usually signals internal leakage or a worn diaphragm.

You will verify each function during diagnostics by comparing gauge readings against specification. Check that brake cylinder pressure matches the size of the reduction. Never skip the final release check before returning the locomotive to service.

Common Failure Modes Behind These Symptoms
Common Failure Modes Behind These Symptoms

When locomotive brake response lags or varies between applications, most faults trace to four sources. These are worn or ruptured diaphragms, leaking graduating and relay valve seats, contaminated passages, and sticking pistons or slides. Trace each symptom to its source before replacing any parts. Start with a static leakage test. It separates external leaks from internal ones. This isolates the faulty component quickly.

Focus on these three high-frequency culprits:

  • Sticky solenoid valves in electropneumatic brake control that hold exhaust or supply paths open
  • Internal air leaks past graduating valve seats in the distributor valve
  • Ruptured brake cylinder diaphragms that bleed pressure under load

Do not ignore contamination. Sludge and scale restrict passages in valves, brake pipe connections, and cylinder ports. Clean these passages with an approved solvent. Blow them dry with clean, dry air before reassembly. Verify each repair with a full brake cycle test. Confirm consistent response across service and emergency applications. Check that brake pipe pressure and cylinder pressure respond in step. Replace components only after confirming the fault. Unnecessary part swaps waste shop time and increase maintenance costs. Document every reading you record, including leakage rates, pressures, and timing.

Walk Through These WABCO Brake Valve Tests

WABCO brake valve tests on locomotives follow a fixed sequence. Run them in order instead of jumping to the test that matches the symptom. Start with the residual pressure check, because stored air in the main reservoirs and brake pipe skews every reading that follows.

Drain the main reservoirs fully and confirm both gauges read zero. Then perform the air leak test with the brake pipe charged to specification. Watch the gauge for a drop beyond the allowable limit, and note the rate.

Isolate leaks by applying soapy water to each fitting, since audible hissing misses small seepage. Finish with the application and release checks only after both tests pass.

Record every reading on the test sheet, because the sequence matters when you troubleshoot later. Don’t skip ahead, even when the symptom points to one valve. Skipping steps hides the fault you’re chasing and wastes time you cannot recover.

Should You Repair or Replace the Valve?
Should You Repair or Replace the Valve?

A failed test sequence does not automatically condemn the locomotive valve. You still need a clear basis for choosing between a field repair and replacement.

Start by identifying the failure mode. Internal leakage, worn graphite pistons, and cracked diaphragms often justify a rebuild. Housing cracks, warped mating surfaces, or repeated failures after service generally call for replacement.

Base your decision on three factors:

Weigh failure scope, repair turnaround, and certification status before committing a locomotive valve to a field rebuild or an exchange unit.

  • Failure scope: isolated seal or gasket fault versus multiple failed functions
  • Repair turnaround: rebuild time against the locomotive’s scheduled availability
  • Certification status: whether the rebuilt unit meets the original specification

Weigh cost against downtime for each option. A cheaper rebuild can cost more than an exchange unit. A rebuild that idles the locomotive for days can lose to an exchange unit fitted in hours.

Document every decision, because consistent criteria across the fleet strengthen your repair strategy and simplify warranty tracking. Don’t skip the teardown findings in your records.

Frequently Asked Questions

Does FRA Regulation Require a Specific Test Interval for Locomotive Brake Valves?

Yes, FRA regulations under 49 CFR Part 229 set specific test intervals for locomotive brake valves. You must complete the annual regulatory test of locomotive brake equipment, including brake valves, within 368 days. The previous test date sets the deadline for the next one. Periodic maintenance inspections under §229.29 add 92-day checkpoints to your schedule. Because these intervals overlap, a tracking system helps your locomotive fleet stay compliant. Do not skip interval compliance. Document each test date, inspector, and result for every locomotive. Accurate records help you avoid costly civil penalties during routine FRA compliance audits.

Can a WABCO Brake Valve Be Safely Installed on a Non-Wabco Locomotive?

You cannot safely install it based on assumption alone. Compatibility depends on port sizing, pressure ranges, and control logic. These must match the host locomotive’s brake system. Written approval is required from the original equipment manufacturer. The railroad’s mechanical department must also approve the installation. Mikura International recommends this review before any installation begins.

Before the valve enters service, perform OEM calibration verification. Check application timing, equalizing pressures, and emergency response. Confirm each result against the manufacturer’s specifications. Then verify FRA compliance under 49 CFR Part 232. Do not place the locomotive in service until this process is complete.

Mikura International supports locomotive operators with technical guidance on brake system components. Contact our team to discuss your locomotive’s requirements.

Are Rebuilt Brake Valves Covered by Warranty, and How Long Does Coverage Last?

Yes, rebuilt locomotive brake valves are often covered by warranty. You’d think a part that has already failed once would earn a shorter leash, not a longer one. Coverage periods vary by product line, so review the written terms before installation. Read the warranty exclusions carefully. Coverage is typically voided by improper installation or use in non-approved locomotive applications. Start claim processing immediately after a failure. Gather the warranty documentation: purchase invoice, serial number, and a detailed failure report.

What Tools and Training Are Required to Certify a Brake Valve Technician?

Certifying a locomotive brake valve technician requires specific tools and structured training.

You will need calibrated pressure gauges for accurate brake system measurements.

A torque wrench ensures valve fasteners meet manufacturer specifications.

A brake pipe leakage tester helps identify leaks in train brake piping.

A bench test stand allows technicians to evaluate valves outside the locomotive.

A digital multimeter is needed for diagnosing electronic control modules on locomotives.

Certification also requires manufacturer-specific classroom instruction.

Supervised hands-on practice builds the skills needed for real locomotive repairs.

Candidates must pass both a written exam and a practical assessment.

The practical assessment tests troubleshooting skills through simulated brake valve faults.

Training should cover safety compliance, including lockout/tagout procedures and PPE requirements.

Technicians must renew their credentials on the schedule required by their railroad.

How Do I Record and Report Brake Valve Defects in the Maintenance Log?

Ironically, the defect you’re tempted to skip deserves the first entry. Log it immediately in the locomotive maintenance log. Record the locomotive number, date, brake valve position, and symptom. Include visual inspection notes describing leaks, cracks, or worn seals. Reference any fault code documentation from the locomotive event recorder. Tag the defect for immediate supervisor review. Do not close the entry until you have logged the repair, retest results, and final sign-off initials. Mikura International recommends complete records for every locomotive brake valve defect.
Why Locomotive Valve Calibration Settings Go Out of Spec?

Why Locomotive Valve Calibration Settings Go Out of Spec?

Locomotive crews and maintenance teams often see brake valve pressures drift outside specification without an obvious cause.
Readings look normal one week and fail inspection the next.

Unexpected calibration drift causes brake response delays, uneven braking, and costly unscheduled downtime on the line.
Finding the root cause early saves time and protects train operations.

Common symptoms that signal calibration drift:

  • Brake cylinder pressure readings fall outside the specified range.
  • Application or release times slow down during brake tests.
  • Moisture or oil residue appears inside valve passages.
  • Hissing or leakage occurs at diaphragm or seal interfaces.
  • Pressure sensor readings disagree with reference gauges.
  • Mounting hardware loosens or valve bodies show vibration wear.
  • Valve behavior changes noticeably after temperature swings.
  • Repeated recalibration fails to hold the setting.
Observed SymptomLikely ContributorVerification Step
Slow brake releaseSpring relaxationMeasure spring preload against OEM specification
Pressure drift at steady stateDiaphragm fatigueInspect diaphragm for hardening, cracks, or permanent set
Erratic pressure readingsAged pressure sensorCompare output against a calibrated reference gauge
Sluggish response in cold weatherSeal stiffening from thermal cyclingCheck seal compliance at operating temperature
Contaminated or restricted passagesMoisture, oil aerosols, pipe scaleFlush and inspect passages and valve seats
Gauge reading jumpsVibration-loosened hardwareTorque-check all mounting hardware

Why Drift Builds Over Time

You will rarely trace an out-of-spec locomotive valve to a single failure.
Drift builds over thousands of brake cycles.

Diaphragm and seal fatigue change elastomer compliance.
Spring relaxation reduces preload.

Moisture, oil aerosols, and pipe scale contaminate passages and seats.
Pressure sensors age.

Vibration loosens hardware.
Thermal cycling stresses seals.

Verify Each Contributor Before Adjusting

Verify each contributor before making any adjustment.
Recalibrating without verification often hides the real problem.

Start with contamination and mechanical condition.
Then check sensor accuracy against a reference gauge.

Adjust calibration only after the physical condition is confirmed.
Understanding these contributors helps crews spot symptoms early and recalibrate correctly.

Sourcing Genuine Locomotive Parts

Mikura International supplies genuine locomotive engine parts from ALCO, EMD, GE, and WABCO.

Replacing worn diaphragms, seals, springs, and sensors with genuine components helps restore calibration stability and extends valve service life.

Key Takeaways

  • Diaphragm and seal fatigue alter elastomer compliance, changing the actuation pressure the valve responds to.
  • Spring relaxation after thousands of brake application cycles reduces preload, shifting the valve’s regulation setpoint.
  • Particulate contamination and rust or pipe scale lodge between moving parts, increasing friction and causing sluggish response.
  • Temperature cycling expands and contracts dissimilar materials, loosening fits, stressing seals, and altering internal force balance.
  • Continuous track vibration loosens mounting hardware and fatigues seals, while aging pressure sensors add reading drift.

What Are the Signs a WABCO Valve Is Off?

What Are the Signs a WABCO Valve Is Off?

Your locomotive’s air brake system usually reveals a drifting WABCO valve well before it fails outright. Watch for slow brake application and release times, which signal sluggish valve response. Time each application against your railroad’s standard, since a lagging valve stretches the cycle. You’ll often notice pressure readings that wander between service reductions, even when you hold the handle steady. Check the brake pipe gauge during a full service application. If brake cylinder pressure overshoots or undershoots the target, the valve’s regulation has shifted.

Don’t ignore intermittent hissing near the valve body, since it points to a worn seat or diaphragm. Compare every reading against the calibration sheet at each scheduled inspection. Record every deviation, and you’ll spot the trend before it becomes a stopped train. Pull the valve for bench testing and recalibration if readings stay out of tolerance after cleaning. Act promptly. For genuine replacement parts and recalibration support, contact Mikura International’s technical team.

What Causes WABCO Valve Calibration to Drift?

Calibration drift in a WABCO valve usually traces to mechanical wear and contamination that build up over service life. You’ll notice the setpoint shifting gradually, not all at once. That pattern points to slow physical change rather than a sudden fault.

Calibration drift in a WABCO valve usually comes from slow wear and contamination over time. The setpoint shifts gradually, pointing to physical change rather than a sudden fault.

  • Diaphragm and seal fatigue: Elastomers in locomotive brake control valves harden and lose compliance, altering the actuation pressure.
  • Spring relaxation: Calibration springs take a permanent set after thousands of brake application cycles, reducing preload.
  • Particulate contamination: Moisture and oil-carrying debris from the air supply lodge between the piston and bore, increasing friction.
  • Temperature cycling: Repeated heating and cooling expand and contract dissimilar materials, loosening fits and stressing seals.
  • Sensor aging: Pressure transducers lose accuracy over time, so the valve may respond correctly while the reading drifts.

Don’t assume the valve itself is failing. Verify the reference gauge first, then compare readings against the manual’s spec. You’ll isolate mechanical causes from sensing faults faster that way.

Does Vibration and Wear Shift WABCO Calibration?

Does Vibration and Wear Shift WABCO Calibration?

Why would a valve that passed calibration last month read differently today? Vibration and wear often explain the change. Continuous track vibration loosens mounting hardware over time. It also fatigues diaphragm seals, shifting the reference pressure that calibration depends on. Check torque on bracket bolts first. Then inspect elastomer seals for compression set before you adjust anything.

Thermal cycling deserves equal attention. Locomotive engine compartments heat and cool with every duty cycle. Repeated expansion and contraction changes the valve body and spring. This alters the force balance inside the valve. You will notice drift that follows compartment temperature rather than elapsed time.

Connector corrosion often mimics mechanical drift. Locomotive environments expose harness connectors to moisture, dust, and constant vibration. Corrosion raises contact resistance and causes voltage drops across the sensor harness. These drops skew the electronic readout. Clean pins with an approved contact cleaner. Reseat each connector firmly. Verify continuity against the specification.

Retest at the calibration bench. If the reading returns to specification, you have isolated a wear or connection issue. If it does not, investigate a setpoint error. At Mikura International, we recommend logging readings after each inspection to track these trends.

How Does Air Contamination Throw Off Valve Calibration?

How does contaminated air shift a locomotive valve’s output before any mechanical wear appears? The answer lies in what travels inside the air stream. Moisture entering the system condenses inside passages and changes pilot pressure response. Particulates settle on seats and diaphragms. Contamination-induced leakage then bleeds pressure you did not account for. The valve reports a setpoint it never actually holds.

Moisture and particulates shift a locomotive valve’s output before mechanical wear ever appears. The valve reports a setpoint it never actually holds.

You will typically find these contaminants in locomotive air systems:

  • Water condensate pooling in control volumes and reservoirs
  • Oil aerosols swelling elastomer seals in distributing and control valves
  • Rust and pipe scale abrading seat surfaces along the brake pipe
  • Desiccant dust migrating from the air dryer into the main reservoir
  • Compressor lubricant carbonizing in discharge passages

Check the air dryer purge cycle and drain the main reservoirs before you recalibrate. If you adjust the setting while moisture remains, the reading will drift again within days of service. Isolate the air supply, purge the lines, and verify dew point with a calibrated hygrometer before adjusting.

How to Recalibrate a WABCO Valve Step by Step?

How to Recalibrate a WABCO Valve Step by Step?

When you start recalibrating a WABCO locomotive brake valve, pull the service data for that exact part number and revision. Adjustment specifications vary across locomotive models, so never rely on memory or older manuals.

Before you begin, make sure the locomotive is secured and shut down. Then isolate the main reservoir air supply and bleed the reservoirs to zero pressure.

Connect your diagnostic tool to the valve controller and confirm the pressure sensor reads zero. Next, run the initial diagnostic steps to capture fault codes and baseline readings.

Then perform a calibration check at each specified test pressure. Compare every reading against the tolerance band in the service data. If a reading falls outside tolerance, adjust the setting in small increments.

After each adjustment, allow the system to stabilize before repeating the calibration check. Once readings hold within specification, start valve learning through the diagnostic interface. This allows the controller to store the new values.

Finally, clear stored fault codes, perform a full brake test, and document every setting. Keep detailed records of all settings for future locomotive maintenance reference.

Frequently Asked Questions

Does WABCO Valve Calibration Drift Affect Fuel Consumption on Long-Haul Locomotives?

Yes, valve calibration drift raises fuel consumption on long-haul locomotives, though the effect is indirect. The first symptom usually appears in brake response accuracy.

When misadjusted relay or distributing valves delay application and release, the locomotive over-brakes. The crew must then re-accelerate with extra throttle, which burns more fuel.

Air leakage from drifted settings forces the main reservoir compressor to cycle more often. That added cycling increases engine load and diesel draw.

Benchmark each valve against the manufacturer’s specification during scheduled maintenance. Regular checks protect long-haul reliability and help control fuel burn. Mikura International can help locomotive operators review valve calibration as part of their maintenance planning.

How Often Do FRA Regulations Require Brake Valve Inspections on Locomotives?

Locomotive operators must perform a time-based inspection of brake equipment at least every 92 days.

Under 49 CFR 229.29, this periodic inspection keeps locomotive brake equipment in compliance.

The annual test under 49 CFR 229.27 must be completed within 368 days.

Brake valves do not wait for a calendar date to misbehave.

When a valve misbehaves, do not wait for the next scheduled check.

FRA incident-based checks apply after a brake-related failure, accident, or FRA directive.

Document every finding and complete a retest before returning the locomotive to service.

Mikura International offers locomotive brake valve components and guidance to help operators stay compliant.

Can WABCO Valves Be Calibrated Using Test Equipment From Other Manufacturers?

Yes, locomotive brake valves can be calibrated with test equipment from other manufacturers. Compatibility must be confirmed before relying on that equipment.

Start by checking that gauges, transducers, and test fixtures meet WABCO’s published accuracy tolerances. Confirm that every fixture matches the port configuration of the locomotive valve under test. Verify that the equipment carries NIST-traceable certification and that its calibration dates are current. Run a known-good reference valve through the setup before testing production units. Document every result so that performance can be traced during audits or railway inspections. If the equipment cannot cover the required pressure ranges, stop testing and use OEM calibration equipment instead.

Mikura International supplies genuine WABCO locomotive valves and can guide buyers on suitable calibration practices.

When Should a Faulty WABCO Valve Be Replaced Instead of Recalibrated?

Replace the valve when recalibration cannot restore specification on a locomotive. This is especially true when the same fault returns at the next check. Review inspection intervals closely. Cracked diaphragms, worn seals, or internal scoring often appear alongside drift that no adjustment corrects. These findings point to physical damage inside the valve body. Recalibration cannot repair mechanical wear, so replacement becomes the only sound option. Log every failure in the locomotive’s compliance documentation. Record the new valve serial number before returning the unit to service. Verify the replacement’s function under load before closing the work order. Perform a full brake application and release cycle during this test. Confirm that brake cylinder pressure response matches the locomotive manufacturer’s specification. Mikura International supplies genuine WABCO replacement valves for locomotive brake systems.

What Certification Do Technicians Need Before Adjusting Locomotive Brake Valve Settings?

Before adjusting locomotive brake valve settings, you need documented qualification under your railroad’s written program. The program must align with 49 CFR Part 232 brake system requirements. You cannot adjust any setting until you complete manufacturer-specific instruction. Passing a practical evaluation is also required before you adjust any setting. Once qualified, you will attend periodic training to refresh your skills. Refresher sessions typically cover calibration procedures, gauge verification, and test protocols. Keep your certification records current and easily accessible at all times. Federal inspectors routinely request these records during audits and inspections, so organized documentation saves time.

Why Choose Professional Air Brake Seal Kits for Your Locomotives?

Why Choose Professional Air Brake Seal Kits for Your Locomotives?

The Most Common Problem: Brake Leakage and Unplanned Downtime

Locomotive operators often face air brake leaks, slow brake response, and unplanned removals.
Worn or mismatched seals cause pressure loss during critical operations.

Pressure loss reduces braking force, extends train stopping distances, and raises safety risks across the fleet.
Mismatched kits also lead to repeat failures and costly yard delays.

Choosing the right seal kit prevents these problems before they start.

Common warning signs include:

  • Gradual brake cylinder pressure drop during extended standby periods
  • Slow brake release times affecting train handling
  • Air leakage during brake applications
  • Dirt or moisture entering the cylinder past worn rod wipers
  • Oil or air seepage at cylinder head gasket surfaces
  • Repeated seal replacements within a short service interval
  • Extended out-of-service time while waiting for correct parts

Symptom-to-solution reference:

SymptomLikely Seal CauseRecommended Action
Gradual pressure dropWorn piston cup sealReplace cup seal and verify bore dimensions
Slow brake releaseSwollen or hardened elastomerInstall a kit rated for your operating temperature range
Contamination in cylinderFailed rod wiperReplace rod wiper and inspect rod surface finish
Air or oil seepage at headDegraded gasketReplace gasket and check groove profile
Repeat failures within monthsMismatched kitConfirm bore, stroke, and model stamp before installation

Why Professional Air Brake Seal Kits Protect Your Locomotive

You protect your locomotive’s braking performance when you match the seal kit to your cylinder’s bore, stroke, and model stamp.
Choose OEM-matched dimensions, verified groove profiles, and elastomers rated for your operating temperature range.

Verify quality through AAR or equivalent certification, batch traceability, and clean, flash-free molding.
Professional kits do not skip parts.

Each kit includes piston cup seals, gaskets, rod wipers, and lubricant.

Mikura International supplies genuine locomotive engine parts from ALCO, EMD, GE, and WABCO.

Our sourcing focuses on parts that meet these specifications.
Keep reading to uncover the inspection steps that stretch service intervals further.

Key Takeaways

  • Professional kits are matched to the locomotive cylinder’s bore, stroke, and groove profile, eliminating trimming or fitting.
  • Components are manufactured to original equipment dimensions and durometer, restoring factory-level sealing performance.
  • Validated elastomers and heat resistance testing help seals withstand constant pressure cycling and temperature swings.
  • Complete kits with matched cup seals, gaskets, rod wipers, and lubricant reduce repeat removals and unplanned downtime.
  • Traceable AAR-compliant certification and batch numbers provide verified quality and clear records for tracking seal degradation.

Which Brake Cylinder Seal Kit Fits Your Locomotive?

Which Brake Cylinder Seal Kit Fits Your Locomotive?

Which Brake Cylinder Seal Kit Fits Your Locomotive?

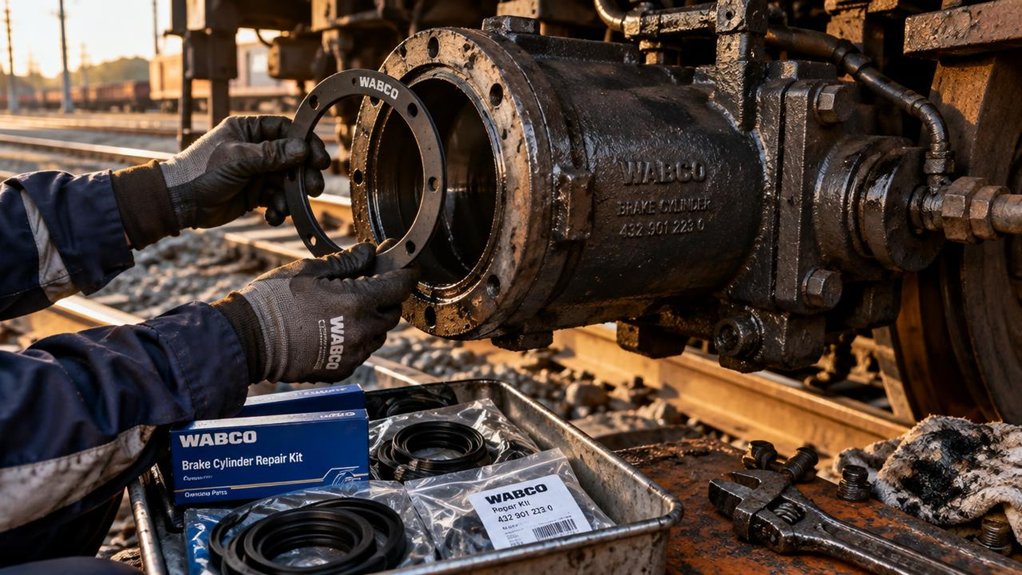
How do you determine which seal kit matches your brake cylinder? Start with compatibility identification. Locate the cylinder’s model stamp, bore diameter, and piston stroke. Cross-reference these figures against the manufacturer’s parts catalog. You will find the part number on the cylinder body or its nameplate.

Begin with compatibility identification. Locate the model stamp, bore diameter, and piston stroke, then cross-reference them against the parts catalog.

Next, verify the kit’s dimensional specifications against your measured values. Confirm that the groove profile, ring cross-section, and gasket material match the original equipment. Never substitute a seal based solely on visual resemblance. Even minor dimensional deviations can cause leakage and erratic brake response.

Finally, evaluate pressure rating considerations. Your locomotive’s operating pressure, typically 90 psi in standard systems, must fall within the kit’s rated limit. Allow a safety margin for peak pressure surges. Check that the elastomer’s temperature range suits your operating environment. Do not rely on the cylinder’s original rating if the kit’s specifications differ. Verify this before installation.

For help matching your cylinder to the right kit, contact the Mikura International technical team.

What Each Locomotive Brake Cylinder Seal Kit Includes

Every Mikura International locomotive brake cylinder seal kit replaces the components that wear or leak inside the cylinder. You rarely need to source parts separately.

You will find piston cup seals, the gasket set, rod wipers, and the lubricant packet. Each component is matched to your locomotive cylinder’s bore and stroke specifications.

Brake kit components are machined to original equipment dimensions, so you will not spend time trimming or fitting. Check the packing list against your work order before you begin disassembly.

Seal material quality determines service life, so verify the compound before installation. Mikura International kits use nitrile or fluorocarbon elastomers designed for locomotive service. These compounds handle continuous exposure to compressed air and petroleum-based lubricants. They also withstand temperature swings from subzero to 250°F.

Inspect each seal for flash, cracks, and dimensional consistency. Reject any component that fails these checks, because a single defective ring compromises the entire assembly. Store unused components in a sealed container away from direct sunlight and ozone.

How to Spot a Quality Locomotive Seal Kit?

How to Spot a Quality Locomotive Seal Kit?

Where does a quality locomotive seal kit separate itself from a substandard one? The answer lies in documentation, materials, and fit.

Start by verifying the manufacturer’s certification to AAR or equivalent standards.

Then examine each component: cup seals, piston packings, gaskets, and O-rings. Confirm each carries a part number matching your brake cylinder model.

Inspect kit compatibility before ordering. Cross-reference the locomotive’s make, model, and cylinder diameter against the kit’s specification sheet.

Mismatched dimensions cause leakage and premature wear. Do not accept “close enough.”

Next, check material quality. Look for NBR or fluorocarbon elastomers rated for your operating temperature range. Confirm that the packaging states the compound.

Verify the elastomer’s durometer hardness against the original equipment specification. Softer compounds extrude under sustained brake pressure.

Smooth, uniform molding signals disciplined production. Reject any kit with flash, voids, or uneven cross-sections.

Why Professional WABCO Kits Outlast Generic Seals

Locomotive brake cylinder seals endure constant pressure cycling, temperature swings, and contamination. You cannot treat them as interchangeable commodities. Professional WABCO kits deliver a durability overhaul, not a cosmetic refit. Mikura International supplies kits engineered for locomotive brake service. Each kit matches OEM compatibility down to durometer and groove tolerances. The seal seats correctly and holds under full brake pressure. Generic seals often miss those specifications.

The difference shows clearly in service life:

FactorOutcome
CompoundCertified OEM elastomer resists swelling
DimensionsMatches original drawings exactly
Heat resistanceVerified across full operating temperature range
Pressure cyclingValidated through endurance testing
Service intervalExtended, with fewer removals

Locomotive operators avoid premature leakage, repeat removals, and unplanned downtime. Documented testing protects braking performance where it matters most. Long-term fleet reliability depends on verified performance, not the lowest unit price.

Keep Your Brake Cylinder Seals Running Longer

Keep Your Brake Cylinder Seals Running Longer

Once a locomotive brake cylinder seal is installed correctly, its life depends on the surrounding system. Protect that investment by verifying the basics during every service interval. Follow strict installation practices: clean the cylinder bore, lubricate with manufacturer-approved grease, and seat the seal without twisting it. Check that the groove is free of burrs and debris before fitting anything into place.

Confirm seal material compatibility before every overhaul or rebuild. Mismatched elastomers swell, harden, or extrude when exposed to incompatible lubricants or contaminants. Match each compound to your locomotive’s fluids and operating temperatures, including the extreme heat of long mainline runs.

Schedule inspections based on operating mileage or service hours rather than waiting for failure. Record each seal replacement, note cylinder wear, and trend the data to spot degradation early. This approach reduces emergency repairs and keeps brake performance consistent across the fleet. Your maintenance logs become your most reliable diagnostic tool on the shop floor.

Frequently Asked Questions

Do These Seal Kits Comply With FRA and AAR Braking Regulations?

Compliance is not automatic, so verify it before purchase. Confirm that brake seal testing records demonstrate performance within locomotive air brake specifications. Check that installation timeframes align with your maintenance schedule and FRA inspection requirements. You remain ultimately responsible for final compliance. Keep all of these records readily available for FRA inspectors during routine audits.

How Long Does a Typical Brake Cylinder Seal Replacement Take?

A typical brake cylinder seal replacement takes two to four hours per cylinder. A full locomotive set can span one shift.

Start by isolating the air supply. Then bleed the reservoirs completely.

Remove the cylinder head with care. Protect the bore and piston surfaces during removal.

Schedule inspection timing during planned maintenance windows. This minimizes installation downtime.

Verify piston travel before reassembly. Confirm seal seating before returning the locomotive to service.

Corrosion or damaged bores will extend that timeline. Plan extra hours when these conditions appear.

Mikura International supplies locomotive-grade brake cylinder seal kits for planned overhauls.

Do I Need Special Tools to Install These Seal Kits?

Yes, locomotive engine seal kits require specialized tools. A standard toolbox will not be enough for this job.

Before you start, verify tool compatibility with your engine model. Mismatched seal pullers and torque wrenches can scratch cylinder bores and damage new seals.

Gather the following tools before beginning. You will need a calibrated torque wrench, snap-ring pliers, a seal installation sleeve, and lint-free cloths.

Check every specification against the locomotive engine manufacturer’s manual. Torque values and clearances vary between engine models.

Complete installation training before attempting the job. Proper technique prevents costly leaks and extends seal life.

Can I Order Bulk Seal Kits for an Entire Locomotive Fleet?

Yes, you can order bulk seal kits for an entire locomotive fleet through Mikura International. We offer several fleet procurement options to suit your operation. These include blanket purchase agreements, scheduled quarterly deliveries, and volume-tiered quotes. Request bulk pricing tied to your total annual quantity to maximize your savings. Verify part numbers against each locomotive’s brake equipment model before ordering. This step prevents fitment errors across mixed fleet configurations. Confirm lead times, shelf-life dates, and packaging quantities before you finalize your purchase order. Our team can help you align these details with your fleet maintenance schedule.

5 Tips for Locomotive Brake Cylinder Gasket Replacement

5 Tips for Locomotive Brake Cylinder Gasket Replacement

Brake cylinder gasket leaks are a common problem for locomotive maintenance crews. A worn or mismatched gasket causes air loss, slow brake response, and unexpected brake failure.

Many crews also struggle to identify the correct kit and complete the replacement without damaging the cylinder bore.

This guide addresses these pain points with practical steps and reference data.

Common problems:

  • Ordering the wrong kit number, which causes fitment failure
  • Residual air left in the reservoir during disassembly
  • Scored or out-of-round cylinder bores
  • Gasket pinched or unseated during assembly
  • Uneven bolt torque that causes air leaks
  • Leaks missed during post-installation testing

Troubleshooting reference:

ProblemLikely CauseCorrective Action
Air leak at cylinder headGasket not fully seatedRemove head, reseat gasket, and retest
Wrong gasket fitIncorrect kit numberVerify the WABCO kit number against the catalog before ordering
Slow brake applicationAir loss through worn gasketReplace gasket kit and inspect bore
Bubbles at joint during soap testUneven or insufficient torqueRetorque bolts crisscross in stages
Scoring marks on bore wallPiston or head damage during removalRepair or replace the cylinder per manufacturer limits

5 Tips for Gasket Replacement:

1. Match the WABCO kit number to the catalog.
Confirm the locomotive model and brake cylinder part number before ordering. Genuine kits ensure correct seal dimensions.

2. Confirm zero pipe pressure and bleed the reservoir.
Isolate the brake system first. Verify that the gauge reads zero pressure.

Bleed the reservoir completely. Lift the cylinder head straight off to protect the piston.

3. Inspect the bore under strong light.
Check the bore for ridges, scoring, and roundness.

Use a strong light source for accurate inspection. Repair or replace the cylinder if defects exceed manufacturer limits.

4. Seat the gasket fully and torque bolts crisscross.
Seat the gasket evenly in its groove.

Tighten bolts in stages using a crisscross pattern. Apply the torque value specified by the manufacturer.

5. Charge, hold, and soap-test every joint.
Charge the cylinder to 90 psi.

Hold the pressure for three minutes and watch the gauge.

Apply a soapy solution to every joint and check for bubbles.

Key Takeaways

  • Confirm the gasket kit’s part number matches the maintenance manual or WABCO catalog exactly, and return any mismatched kit to Mikura International.
  • Bleed all auxiliary reservoir air and crack the supply fitting slowly, then loosen head bolts in a crisscross pattern.
  • Clean the bore with a lint-free rag and approved solvent, never a wire brush, then check for scoring and roundness.
  • Seat the gasket fully in its groove and confirm it sits flush before torquing bolts in crisscross stages to specification.
  • Charge the cylinder to 90 psi, hold for 3 minutes, and soap-test all joints; a drop over 3 psi indicates a leak.

Match Your WABCO Gasket Kit Number First

Match Your WABCO Gasket Kit Number First

Confirm the kit number before you open the locomotive brake cylinder. Compare the kit label against the part number in your locomotive’s maintenance manual or the WABCO parts catalog. Do not rely on memory or previous orders.

Identify gasket compatibility issues by checking the cylinder model, bore diameter, and port configuration. Mismatched kits cause leaks, misapplied brakes, and costly locomotive downtime. You will find the kit number and cylinder model stamped on the cylinder nameplate. Verify correct WABCO fitment before installation by cross-referencing both against the packing slip. Reject any kit that does not match exactly.

Photograph the kit label and cylinder nameplate before disassembly. This record simplifies warranty claims and future troubleshooting. Keep the documentation with the locomotive’s service file for later reference.

Check the gasket’s material rating against brake fluid and operating temperature specifications. Never skip this check, even under schedule pressure.

Release Air and Remove the Cylinder Head

Before you loosen anything, secure the locomotive. Apply the independent and automatic brakes. Chock the wheels, then shut down the engine. Confirm the brake pipe pressure has dropped to zero on the gauge before you proceed.

Next, bleed the system safely by following this sequence:

  1. Open the bleeder valve on the auxiliary reservoir and let all air drain completely.
  2. Crack the cylinder supply fitting slowly so you do not trap pressure in the piston chamber.
  3. Watch the main reservoir and brake cylinder gauges until both read zero.
  4. Loosen the cylinder head bolts in a crisscross pattern.

Work methodically to prevent air lock in the lines. Keep the bleeder open during removal to avoid trapping pressure behind the piston. Lift the cylinder head straight off the studs. Keep the gasket surface clean and undamaged.

Store the head on a clean bench, face up, so its gasket seat stays protected.

Inspect the WABCO Bore for Scoring

Inspect the WABCO Bore for Scoring

With the cylinder cover removed, the bore is exposed for inspection. Clean it thoroughly before checking for scoring. Wipe away old gasket residue, carbon, and oil deposits with a lint-free rag and approved solvent. Never use wire brushes, since they can gouge the surface.

Once the cylinder cover is off, clean the bore thoroughly with a lint-free rag and approved solvent. Never use wire brushes, as they can gouge the surface.

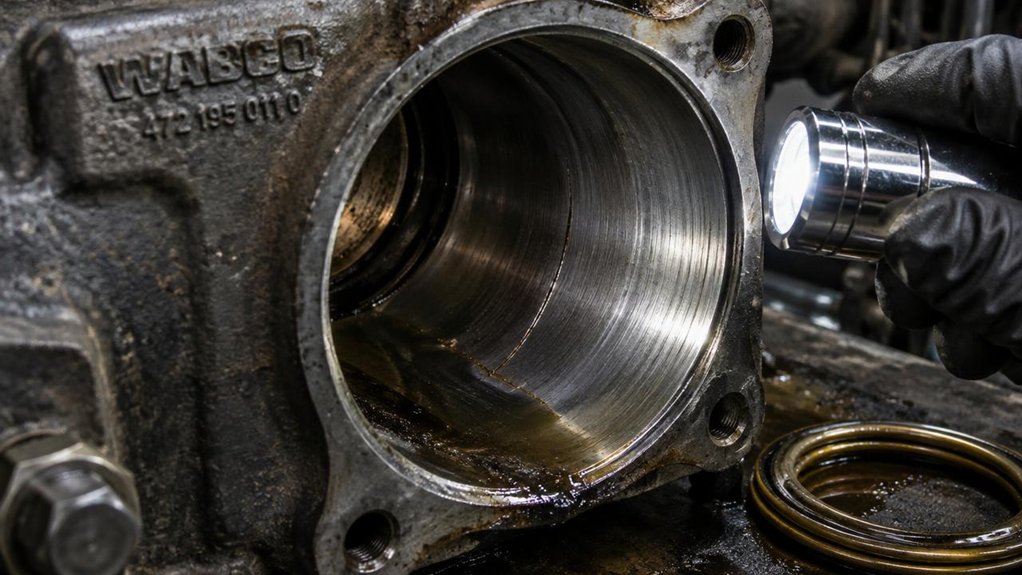
Examine the bore under a strong light. Rotate a flashlight to reveal shallow grooves. Run your fingernail across the wall. If it catches on a ridge, you have found scoring. Light scratches that do not catch are acceptable. Deep grooves, however, require bore replacement. They cause air leaks and erratic brake response on locomotives.

Check for scoring at multiple depths. Wear often concentrates near the piston’s travel limits. Confirm the bore is round using a bore gauge. Reject any cylinder that falls outside the manufacturer’s tolerances. Never install a new gasket over a damaged surface, or leakage will repeat. Dry the bore thoroughly before reassembly.

Seat the Gasket, Then Torque Bolts in Crisscross Order

Seat the Gasket, Then Torque Bolts in Crisscross Order

Seat the gasket fully in its groove before you touch the fasteners. You will prevent leaks and uneven loading by confirming the gasket sits flush around its full circumference. Check the gasket surface orientation against the engine manual. Installing the wrong side can compromise sealing under marine operating loads. Once the gasket is seated, tighten the cylinder head bolts in crisscross order, working in stages.

  1. Check bolt thread condition. Inspect threads for damage and clean them thoroughly. Replace any stretched or corroded fasteners before assembly.
  2. Verify even gasket seating. Press the gasket evenly and confirm no gap appears around the perimeter.
  3. Tighten in crisscross order. Work in stages, bringing each bolt to specification over multiple passes.
  4. Avoid over-tightening. Stop at the specified torque value. Excess torque distorts the cylinder head and damages the gasket.

Log each final torque value for your maintenance records. Recheck all bolts after the first heat cycle. Bolt relaxation often appears early in a marine engine’s service life. Catching it early prevents leaks. This routine helps maintain a reliable, leak-free seal under full operating pressure.

Leak-Test the WABCO Cylinder Before Returning to Service

Leak-Test the WABCO Cylinder Before Returning to Service

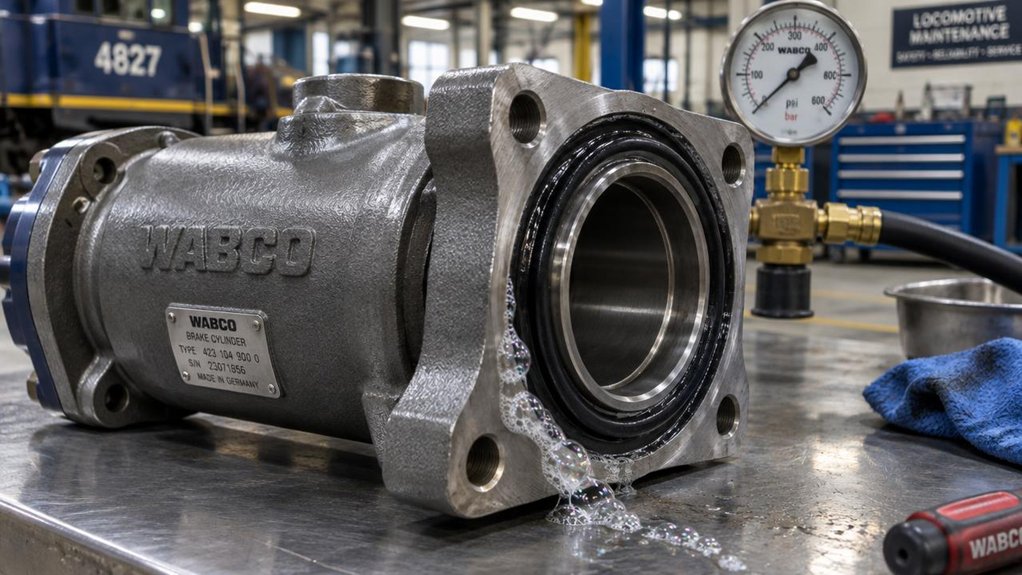
Once the cylinder head bolts are torqued, pressurize the WABCO brake cylinder to confirm the seal. Locomotive brake reliability depends on this check. Connect a regulated air supply and charge the cylinder to 90 psi. Close the supply valve, then watch the gauge. Pressure should hold steady. Any pressure drop signals a leak at the gasket or piston seal.

Test StepTarget ReadingFailure Action
Apply 90 psi airHold steady for 3 minTroubleshoot valve wear
Check gauge dropUnder 3 psiVerify air pressure at supply
Soap-test jointsNo bubblesRetighten or re-gasket
Cycle brake applicationSmooth piston travelInspect piston seal

Do not skip the soap test. Apply soapy water to every joint and fitting. Look for bubbles. If the gauge falls or bubbles appear, troubleshoot valve wear before the cylinder returns to locomotive service. Verify air pressure again after completing all repairs.

Frequently Asked Questions

How Often Should Locomotive Brake Cylinder Gaskets Be Replaced as Preventive Maintenance?

Locomotive brake cylinder gaskets should be replaced on a scheduled basis, not after leaks appear. Mikura International recommends replacing them at every major brake overhaul. Inspect the gaskets at every periodic service. Look for wear, hardening, and extrusion. Replace any gasket that shows these signs. Record every replacement promptly in the maintenance log.

Follow manufacturer specifications and AAR guidance when setting intervals. Adjust those intervals to match your fleet’s actual duty cycle. Consider the operating environment too. Heavy grades, extreme temperatures, and dusty yards accelerate gasket deterioration. Shorter intervals may be needed for these locomotives. Mikura International supports railway maintenance teams with dependable brake components. Check that every gasket meets the specifications for your locomotive model.

Can a Generic Gasket Be Used Instead of an OEM WABCO Gasket Kit?

Yes, you can use a generic gasket, but only if it matches OEM specifications. Verify material compatibility with compressed-air and lubricant exposure. Confirm the operating temperature range meets locomotive requirements. Check the durometer against the original WABCO specification. Check all dimensions against the original part number.

Mikura International recommends verifying every specification before purchase. You are responsible for pressure testing the assembly. Test to the specified brake cylinder leakage limits before returning the locomotive to service. Document all pressure test results. Retain these records for regulatory audits. If you cannot confirm compliance, do not install the gasket.

What Early Warning Signs Suggest a Brake Cylinder Gasket Is Failing?

Like a canary in a coal mine, your locomotive brake system signals trouble long before it fails. Listen for hissing near the brake cylinder during operation. Watch for slow brake release after each brake application. Check for gradual air pressure loss during static brake tests. Inspect for oil residue around the cylinder gasket and mating surfaces. Look for soap-bubble seepage around flanges during leak tests. Note any extended reservoir recharge times. Track rising pressure drop rates at every inspection interval. Catch these warning signs early. A failing gasket on a grade can lead to a runaway train.

Does FRA Regulation Require Records When a Brake Cylinder Gasket Is Replaced?

Yes, documentation matters when a locomotive brake cylinder gasket is replaced. FRA rules in 49 CFR Part 229 require railroads to keep records of locomotive brake inspections, tests, and repairs. Each gasket replacement falls under this recordkeeping framework. Do not rely on memory alone. Maintenance logs should capture the date, locomotive number, cylinder location, gasket part number, technician, and test results. Part 229 does not list every field for every component.

Confirm specifics with your railroad’s maintenance program. Verify retention periods and form requirements there as well. Auditors will check compliance, so complete records protect both your crews and your operation. Mikura International recommends a standard log template for all locomotive brake work. Consistent entries make inspections faster and audits easier to pass.

What Is the Typical Cost of a Locomotive Brake Cylinder Gasket Kit?

Like a compressed ring holding back air, a locomotive brake cylinder gasket kit is a small but vital part. Typical costs range from roughly $75 to $550. Pricing depends on whether the kit is OEM or aftermarket, and on what it contains. Mikura International supplies locomotive brake cylinder gasket kits for railroad maintenance teams. Before ordering, request a labor time estimate from your shop. Installation hours add substantially to the total. Confirm warranty coverage details with your supplier directly. Some locomotive manufacturers void coverage when non-approved parts are installed. Check approved part numbers before you buy.

What Locomotive Brake Gasket Parts Need Replacement?

What Locomotive Brake Gasket Parts Need Replacement?

Locomotive crews and maintenance teams often struggle to identify which brake valve gaskets must be replaced. Guessing wrong causes air leaks, brake response delays, and costly rework.

Clear rules for inspection, part matching, and soap testing solve this problem quickly and reliably. Mikura International supplies genuine locomotive brake parts for these repairs.

Common problems that lead to gasket failure:

  • Air leaks appear at the body joint after reassembly.
  • Gaskets flatten or harden from heat and age.
  • Gasket material extrudes into the air passage.
  • Cracks go unnoticed during visual inspection.
  • The wrong kit number is ordered for the valve model.
  • Reused gaskets fail after their seals were broken.
  • Soap test leaks exceed the specified limit.
  • Brake response slows during terminal tests.

Gasket replacement reference:

Joint or ItemWhat to CheckRequired Action
Body jointFlattening, cracking, extrusionReplace gasket
Cover jointHardening, seal distortionReplace gasket
Intermediate plate jointLeak above specification during soap testReplace gasket and retest
Valve nameplateModel numberMatch kit to locomotive parts catalog
Any previously opened jointBroken sealReplace gasket, do not reuse

Replacement Requirements

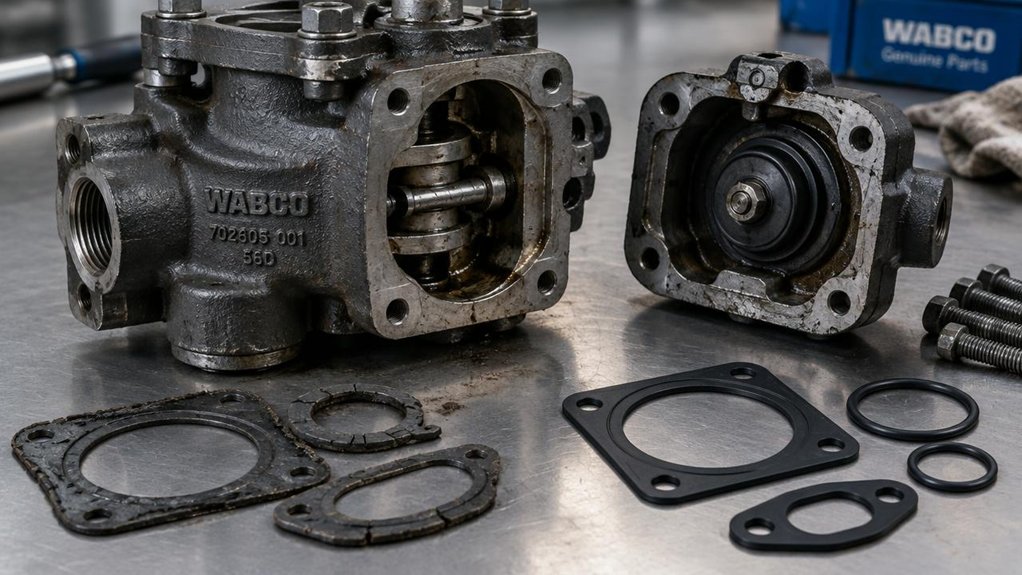
You’ll need to replace every gasket at the body, cover, and intermediate plate joints of the Wabco brake valve. Check the valve nameplate model first.

Match the gasket kit part number to the locomotive parts catalog. Do not reuse any gasket once its seal has been broken, even if it appears serviceable.

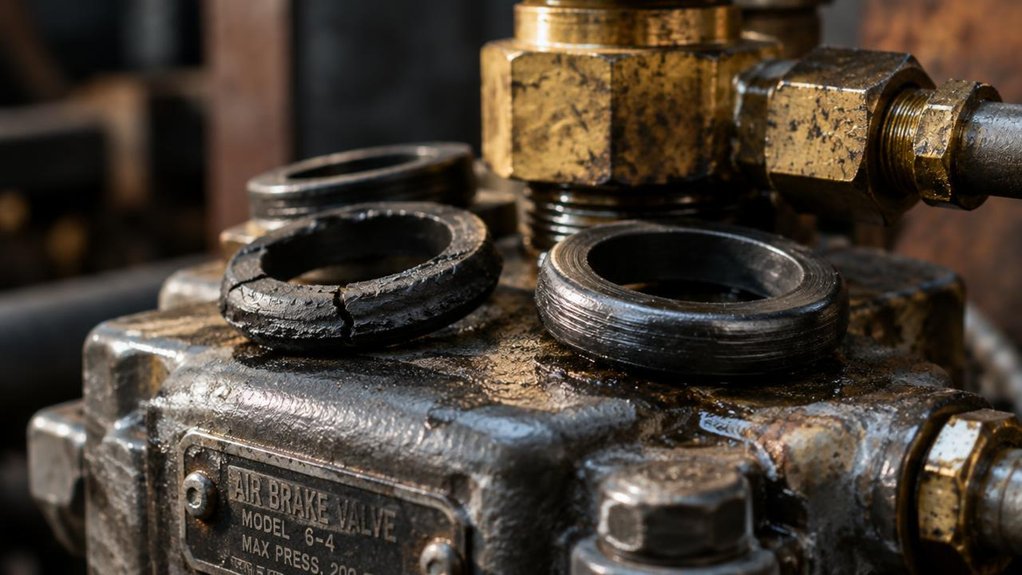
Replace gaskets showing flattening, cracking, extrusion, or hardening. Replace any joint that leaks above specification during soap testing.

Inspection and Replacement Steps

  1. Confirm the valve model from the nameplate.
  2. Order the matching gasket kit from the locomotive parts catalog.
  3. Remove the cover and intermediate plate carefully.
  4. Clean all gasket seating surfaces thoroughly.
  5. Inspect each gasket for flattening, cracks, extrusion, and hardening.
  6. Install new gaskets from the matched kit at every opened joint.
  7. Tighten fasteners evenly in the specified sequence.
  8. Soap test each joint and recheck any leaks.

Mikura International supplies genuine locomotive parts from ALCO, EMD, GE, and WABCO. Visit https://mikurainternational.com to find the correct gasket kit for your locomotive.

Key Takeaways

  • Gaskets at every body and cover joint, plus any intermediate plate, on Wabco locomotive brake valves need replacement.
  • Confirm the model stamped on the valve nameplate and match the part number to the locomotive parts catalog.
  • Replace the full gasket kit for every joint, since gasket count and size vary by valve family.
  • Replace any gasket that is flattened, cracked, torn, extruded, hardened, or oil-saturated, even if it looks serviceable.
  • Never reuse a gasket once its seal has been broken, because compression set and tooling damage prevent resealing.

Which WABCO Brake Valves Use Gaskets?

Which WABCO Brake Valves Use Gaskets?

Most Wabco locomotive brake valves with separable housings use gaskets at their body and cover joints. You’ll find these seals between the valve body, the cover, and any intermediate plate. They keep compressed air inside the passages.

Identify each gasket before you disassemble anything. Valve families differ in joint count and gasket size.

Start by checking the model stamping on the valve nameplate. Compare the part number against your locomotive parts catalog. Confirm the gasket kit matches every joint on the unit.

Do not reuse a gasket that is flattened, cracked, or torn. Replace it even if it looks serviceable.

Gasket failure often shows first as a slow pressure bleed. Perform an air leak diagnosis with a soap solution at each joint while the system is charged. Mark any bubbling location for repair.

Complete a brake pipe hose inspection before condemning the valve. Cracked or swollen hoses can mimic a failed gasket.

How Can You Tell a WABCO Brake Gasket Has Failed?

A failed Wabco gasket on a locomotive usually reveals itself as a slow pressure bleed at a valve joint. You cannot trace the leak to a fitting or pipe.

A failed Wabco gasket on a locomotive usually shows up as a slow pressure bleed at a valve joint, not at a fitting or pipe.

You may notice the gauge needle drifting during a brake pipe leakage test. The main reservoir compressor may also cycle more often than it should.

Apply these visual inspection tips to the locomotive brake valve. Check the gasket for extrusion, flattening, cracking, and hardening. Oil saturation around the flange signals a seal past its service life.

Wipe the joint dry. Then watch for fresh seepage after a full main reservoir charge.

Check for these common leakage symptoms:

  1. You hear hissing at the valve body during brake release.
  2. Brake cylinder pressure falls after you set the application.
  3. Soap solution bubbles along the gasket seam.
  4. You find black residue or gasket fragments on the mounting surface.

Isolate the suspect valve and retest before replacing anything. Misdiagnosis wastes valuable time and costly replacement parts.

WABCO Gasket Parts to Inspect First

WABCO Gasket Parts to Inspect First

Start with the gasket and its seating surfaces before removing any valve components from the locomotive brake assembly. Remove the cover and examine the gasket’s full circumference for cracks, hardening, flattening, or nicks.

A gasket that looks intact can still fail once compressed. Check its thickness and resilience against the Wabco specification. Note any extrusion into the passages, since it signals excessive pressure or improper seating.

Next, inspect the mating surfaces on the valve body and cover. Look for scoring, pitting, warping, and residue that could prevent a tight seal. Run a straightedge across the sealing face and wipe it clean with a lint-free cloth. Any groove deeper than the gasket can accommodate means the housing needs machining or replacement.

Finally, inspect the fasteners and bolt holes. Uneven clamping often causes air leaks, so verify bolt torque before reassembly. Also, while inspecting brake shoe and wheel tread wear patterns on the locomotive, note the gasket condition.

How Often Should Wabco Brake Gaskets Be Replaced?

Never reuse a Wabco gasket once you have broken its seal. Compression set and tooling damage reduce its ability to reseal.

Replacement timing is not fixed. You must base it on several maintenance interval factors rather than a single calendar date.

Replacement timing depends on several maintenance interval factors, not a single calendar date. Inspect each locomotive’s gaskets based on actual operating conditions and test results.

Review these maintenance interval factors at every scheduled brake valve service on your locomotives:

  1. Operating environment: Dust, humidity, and extreme heat shorten expected service life. Inspect those gaskets sooner.
  2. Duty cycle: Heavy grades and frequent emergency brake applications fatigue the seal faster. Track cumulative brake cycles for each locomotive.
  3. Air quality: Moisture and oil contamination swell elastomers. Verify air dryer and lubricator performance first.
  4. Leakage results: Any leak exceeding specification during testing requires immediate gasket replacement, regardless of age.

Set your replacement schedule from actual inspection data, not the calendar alone. This data-driven approach helps you avoid costly, unplanned brake failures. Mikura International supports your locomotive brake maintenance program. Keep your entire locomotive fleet running safely and reliably.

WABCO Gasket Part Numbers by Locomotive Model

WABCO Gasket Part Numbers by Locomotive Model

Once you’ve set the replacement interval, confirm the correct part number before you order. Wabco gasket part numbers vary by locomotive model, engine series, and brake system configuration. Don’t rely on memory or a previous order. Start by identifying your locomotive’s model designation and build year from the data plate. Then open the current Wabco model lookup charts. Cross-reference the model against the brake valve and gasket kit listed for it.

Some models share kits, while others require distinct part numbers. Next, run brake gasket compatibility checks. Compare the listed part number against the existing valve housing markings and the original gasket dimensions. If the numbers don’t match, stop and verify with the manufacturer directly. Our team at Mikura International can help you confirm the right part for your locomotive. Record the exact confirmed part number, the locomotive road number, and the lookup date in your maintenance log. Doing so helps you avoid costly returns, delays, and unplanned locomotive downtime.

Frequently Asked Questions

Do Aftermarket Brake Gaskets Meet the Same Standards as Genuine WABCO Parts?

Not automatically. Never assume aftermarket locomotive brake gaskets are equivalent to genuine Wabco parts.

Verification is essential before any gasket enters a locomotive air brake system.

Start by requesting documentation confirming material compliance with the original Wabco specification.

Ask for compatibility test results covering both pressure cycling and temperature cycling.

Verify fitment against the OEM part number before installation.

Measure groove dimensions and sealing surfaces carefully.

Compare every measurement against the Wabco drawing for that specific component.

Check warranty terms closely, because many suppliers exclude damage linked to non-OEM parts.

Demand certifications rather than relying on price or marketing claims.

Can a WABCO Brake Gasket Be Reused After It Has Been Removed?

No, you should never reuse a locomotive brake gasket once it has been removed. The gasket that keeps your air brake system airtight rarely survives removal intact. Before reinstalling, inspect it carefully for cracks, flattening, tears, and hardening. Confirm that your cleaning solvent is compatible with the elastomer. Aggressive solvents can swell or degrade the material. Clean the mating surfaces with an approved solvent and remove all old residue. Torque the fasteners to the manufacturer’s specification. Do not gamble on a used seal in a locomotive brake system. Install a new gasket every time you disturb the joint.

How Much Does a Typical Locomotive Brake Gasket Replacement Cost?

A typical WABCO brake gasket replacement runs $150 to $900 per locomotive. The final cost depends on gasket count and component access.

Gasket kits generally cost roughly $20 to $120. Labor typically adds two to six hours at shop rates.

Freight downtime often costs more than the parts and labor combined. A locomotive out of service can idle thousands of dollars in revenue each day.

Schedule repairs during planned maintenance windows to limit lost service time.

Verify torque specifications before final assembly. Always perform a leak test after reassembly.

Mikura International can help locomotive operators source the right gasket kits for their WABCO brake systems. Contact our team to confirm part numbers before scheduling the job.

What Sealant or Lubricant Is Safe to Use With Brake Gaskets?

Your locomotive brake gasket is a shield that must survive brutal heat and constant pressure. Choose a sealant with proven high temperature compatibility. Use a manufacturer-approved, non-hardening gasket sealer for the best results. Pair it with a silicone-based or PTFE-based lubricant that will not swell the elastomer. Avoid petroleum greases, because they degrade rubber seals over time. Before installation, clean all mating surfaces thoroughly. Remove old sealant, oil, and debris from flanges and grooves. Torque bolts in a star pattern to ensure even clamping force. Do not over-apply sealant, since excess material can squeeze into the brake passages.

Does the FRA Require Documentation When Brake Gaskets Are Replaced?

The FRA does not have a standalone rule requiring a separate record for every brake gasket replacement. Documentation is required when the work falls under required locomotive brake maintenance. Review the required records under 49 CFR 229.27 to confirm which entries you must keep. Record the part identification and the technician’s name for every gasket replacement. Complete post-work verification before returning the locomotive to service. Include a brake leakage test in that verification. Retain the record for the period the regulation requires. Mikura International recommends keeping gasket part numbers, batch details, and installation dates together in one maintenance file.

7 Tips for Railroad Engine Bearing Wear Measurement

7 Tips for Railroad Engine Bearing Wear Measurement

Locomotive maintenance teams often struggle to separate real bearing wear from measurement error.
Inaccurate readings lead to missed failures, unplanned downtime, and costly crankshaft damage.

Wrong clearance numbers also cause premature shell replacement.
Accurate, repeatable measurement prevents these problems before they reach the engine.

The tips below show how to measure consistently and reliably.

Common pain points:

  • Clearance readings change from one inspection to the next.
  • Heat from recent operation distorts measurements.
  • Dirty journals and anvils produce false wear readings.
  • Teams apply the wrong wear limit to a journal.
  • Crown and parting-line wear are often misread or ignored.
  • Inspection records are incomplete, so wear trends go unnoticed.
  • Shells are replaced too early or too late.
Inspection CheckpointWhat to VerifyWhy It Matters
Component temperatureCap, axle, and frame are at ambient temperatureHeat closes clearance and hides metal loss
Journal and anvil conditionSurfaces are clean and free of oil, carbon, and debrisContamination causes inaccurate gauge readings
Main bearing clearanceMeasured in place using the correct methodConfirms the actual running clearance
Crown wearUniform wear pattern across the shellIndicates load distribution or alignment issues
Parting-line wearEdge wear at the shell split linePoints to housing fit or installation problems
Model-specific limitMatched to the correct EMD published maximumPrevents using the wrong replacement criteria
Inspection recordReadings, dates, and tag numbers loggedEnables trend analysis and early warning

Tip 1: Let Components Cool to Ambient Temperature

Wait until the cap, axle, and frame reach ambient temperature.
Heat closes clearance.

Warm components hide real metal loss.
Measure only after everything has stabilized.

Tip 2: Clean Journals and Anvils Thoroughly

Wipe the journals and anvils clean before measuring.
Remove oil, carbon, and debris.

Contamination skews gauge readings.
Clean surfaces give repeatable results.

Tip 3: Gauge Main Clearance In Place

Measure main bearing clearance without removing the shell from the housing.
Use the approved method for the engine model.

Record readings at the specified positions each time.

Tip 4: Read Crown and Parting-Line Wear

Inspect the crown of the shell for uniform wear.
Check the parting line for edge wear.

Crown wear often signals load or alignment issues.
Parting-line wear often points to housing fit problems.

Tip 5: Match Each Journal to the Correct EMD Limit

Confirm the engine model, bearing size, and current service data before comparing readings.
Apply the published EMD maximum for that specific journal.

Do not rely on generic or outdated limits.

Tip 6: Log Every Inspection

Record every clearance reading, date, and tag number.
Include oil analysis results and housing observations.

Consistent logs reveal wear trends before failure occurs.

Tip 7: Replace the Shell at the Published Maximum

Replace the shell once clearance reaches the published maximum.
Inspect the housing for damage before reinstalling.

Stay consistent with inspections, so oil trends and housing checks remain reliable.

Mikura International supplies genuine locomotive engine parts, including EMD main bearing shells, for verified replacement needs.

Key Takeaways

  • Measure traction-motor and support bearings only after they cool fully to ambient temperature.
  • Wipe journals, cap faces, and gauge anvils clean before seating any measuring tool.
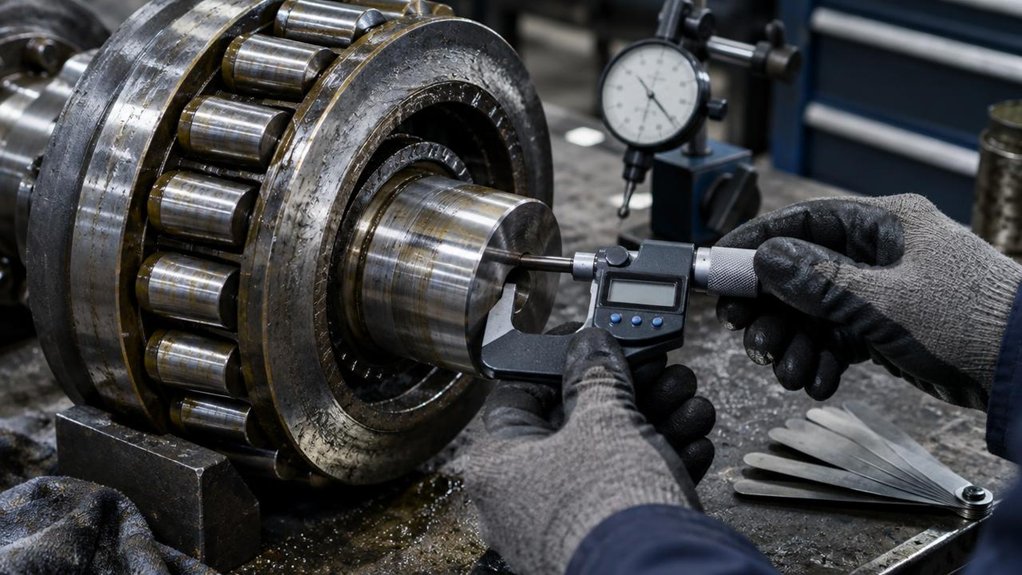
  • Gauge clearance in place using the builder’s Plastigage, lead-wire, or dial-indicator method.
  • Record crown wear and the thinner parting-line wall thickness; replace shells at the builder’s crown limit.
  • Compare each reading with the engine-specific EMD limit and confirm wear with oil-analysis trends.

Measure EMD Bearing Wear Only When Cold

Measure EMD Bearing Wear Only When Cold

Because EMD traction-motor and support bearings expand as they heat, measure wear only after the locomotive cools to ambient temperature. Do not gauge a hot journal and treat the reading as final. Thermal growth closes clearances and shifts the housing. A warm reading understates wear. It can hide a bearing that is already out of limit.

Set cold measurement timing by the shop thermometer, not by how long the unit has sat. Wait until the bearing cap, the axle, and the motor frame match ambient air. If one component stays warmer, wait longer. Record the air temperature beside each reading. This lets the next inspector confirm the same condition.

Prevent measurement bias by comparing each reading with the last cold record. Do not compare against a hot check taken during the run. Do not torque, pry, or correct for unmeasured heat. If the locomotive ran recently, leave gauges boxed.

Clean Bearing Surfaces Before You Gauge

Before you seat the gauge, wipe the journal, the cap face, and both anvils until clean metal shows. Oil film, carbon, and lint change contact and shift your reading. Use a clean, lint-free rag and a light solvent approved for the locomotive bearing. Don’t leave any residue behind.

After you wipe, inspect the lubricant condition on the rag and in the oil groove. Dark grit, metal flakes, or a burnt smell means you stop and report the finding before you continue. Then verify bearing alignment by eye and by feel. The cap must sit square on the journal without a cocked edge or a lifted corner. A cocked cap loads one anvil and gives a false wear number.

Reclean any spot the rag missed. Seat the anvils only on dry, bright metal. If you don’t, grit under the contact pads stacks into the measurement. You end up chasing a number that isn’t real.

Gauge Main Bearing Clearance in Place

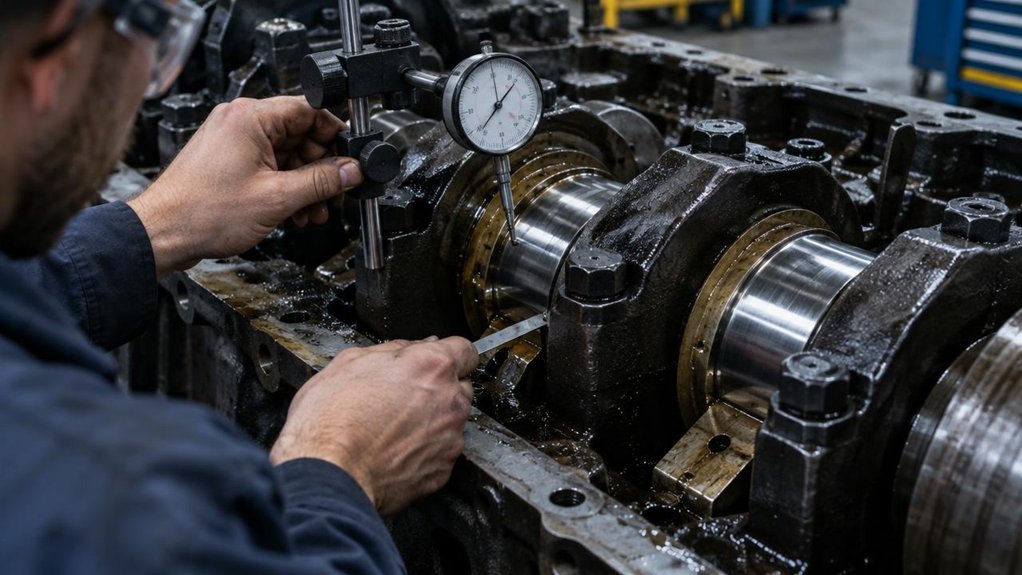
How do you gauge main bearing clearance in place on a locomotive engine? Start by confirming the locomotive builder’s inspection procedure. Avoid crankshaft removal unless the railroad’s maintenance procedure requires a full teardown. Select inspection tooling that matches the engine builder’s method. Choose Plastigage, calibrated lead wire, or a dial indicator on a rigid fixture. Clean the journal and bearing shell thoroughly before any measurement. Seat the gauge material or indicator tip only where the procedure allows.

Torque the main bearing cap to the specified sequence and value. Release the cap carefully, then read the crushed gauge width or indicator travel. Compare the reading against the specification chart for that bearing position. Match the comparison to the oil grade and temperature band listed in the procedure. Reject any reading outside the minimum or maximum clearance limits. Record the bearing position, tool ID, and torque value for each measurement. Consistent records allow the next inspection to repeat the same setup. Stop once installed clearance is confirmed, logged, and checked against the builder limit for that main bearing.

Mikura International offers locomotive engine bearing components and inspection tooling for railroad maintenance teams.

Read Bearing Wear at Crown and Parting Line

You read crown wear first because that point takes the highest load and shows the earliest loss of bearing material. Place the gauge at the crown, record the thickness, and compare it with the manufacturer’s limit before you accept the shell. Then check both parting lines for edge wear, fretting, and uneven crush so you don’t miss a shell that’s still thick at the crown but failing at the joints.

Crown Wear Reading

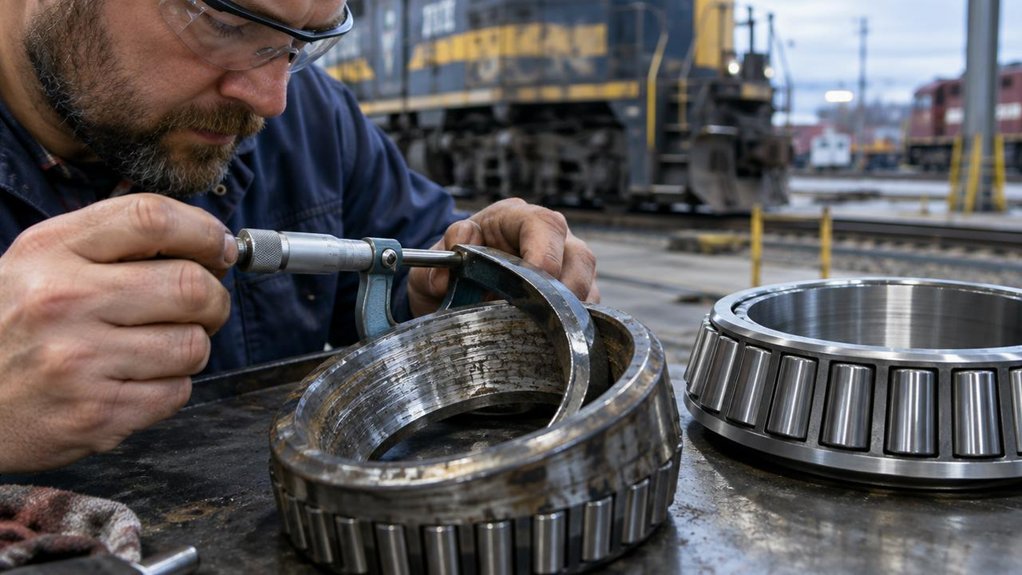
When you take a crown wear reading on a locomotive engine, measure the bearing shell at the crown and at the parting line. Compare the two thicknesses to quantify metal loss. Seat the shell on a flat reference plate first. Zero your digital dial gauge on an unworn area before you probe the crown. Hold the gauge perpendicular to the shell surface. Take three readings across the crown and record the lowest value. Subtract the crown thickness from the parting-line thickness to find wear. Do not average away a local thin spot. Log each result with engine hours so wear trends show whether loss is stable or accelerating. Replace the shell when crown wear reaches the locomotive builder’s limit. Recheck the readings if they disagree.

Parting Line Checks

Parting-line thickness sets the baseline for wear calculation. Check both locomotive bearing shell halves with the same gauge setup. Place each shell half on a certified flat plate. Measure wall thickness at both parting lines with one micrometer. Keep anvil force, temperature, and zero consistent for every point. Record the thinner parting-line value as the baseline. Subtract the lowest crown reading from that baseline to calculate wear. Do not average mismatched halves. When the two parting-line readings exceed the manufacturer’s spread, reject the shell. Order NDE inspection for the rejected shell. Open root cause analysis for crush loss, bore distortion, or embedded debris. Recheck the locomotive engine housing before reuse. This keeps your wear figure repeatable. Log the gauge serial number with every reading.

Compare Bearing Wear With EMD Limits

Compare Bearing Wear With EMD Limits

On locomotive engines, match each wear reading to the EMD limit for that position.

Use the bearing position, engine model, and service interval for every comparison.

Do not use one clearance for every journal.

Main, rod, and cam bearings follow separate charts.

A 645 limit does not apply to a 710 engine.

Select the table for the engine model and the service interval now in force.

Compare OEM and EMD tolerances before you scrap any shell.

OEM specifications often run tighter than EMD field limits.

A high OEM comparison can still pass the railroad limit.

Decide from the EMD figure.

Use the OEM gap only to judge how fast clearance is growing.

Interpret wear gauge trends on the same journal.

A sub-limit reading that climbs each time needs action sooner.

A steady reading near the cap can wait longer.

Replace any bearing that meets or exceeds the published EMD maximum.

Record Bearing Wear After Each Inspection

Log each bearing clearance right after you finish the inspection. Do not delay the entry until shift end. Delayed entries mix positions and reduce precision.

Record the clearance beside the bearing location, locomotive engine number, date, and your name. Use the same units every time. Consistent units keep comparisons valid.

Attach the reading to your visual inspection records before you leave the work area. Add brief notes on oil film, discoloration, and scoring. Keep these observations separate from the measured value.

You will rely on these figures for trend wear analysis after repeated inspections. Identify the gauge and its calibration date. Reviewers use this information to assess data quality.

If you repeat a questionable measurement, enter both results. Mark the accepted reading clearly. Retain measured precision without rounding.

Sign every line. Place the completed sheet where the next crew can retrieve it immediately. File the sheet before you leave today.

Schedule Replacement When Bearing Wear Exceeds Spec

Schedule Replacement When Bearing Wear Exceeds Spec

You’ve recorded each clearance with its location and date. Compare the accepted reading with the published wear limit before the locomotive returns to service.

If clearance exceeds the published specification, do not return the locomotive to service. Schedule replacement before the next assignment. Tag the axle so dispatch will not release it.

Complete a bearing housing inspection before you order parts. Check the bore for ovality, fretting, and heat tint. Confirm cap-bolt torque. Do not reuse a housing that fails those checks. Replace it with a qualified new spare from Mikura International.

Use oil analysis trending to confirm the reading. Rising iron or copper, with falling viscosity, shows the wear is not an isolated measurement error. When metals rise across two samples as clearance grows, move the replacement earlier.

Log the limit, the decision, and the shop that will fit the new bearing. This keeps the out-of-spec journal off the main line.

Frequently Asked Questions

What Tools Are Needed to Measure EMD Bearing Wear?

Line the gauge up with the scar so both readings coincide. Never trust a single number.

Measure EMD bearing wear with an outside micrometer, a dial bore gauge, and a feeler set.

Add ultrasonic testing when wall loss hides beneath the surface.

Run a boroscope inspection when you cannot pull the cap.

Record clearance, ovality, and heat tint before you release the locomotive engine.

How Often Should Railroad Engine Bearings Be Inspected?

Railroad engine bearings require inspection on a schedule set by the engine builder. Your railroad’s preventive maintenance program also defines these intervals. Actual operating conditions determine how often you should check them. Typical intervals range from daily visual checks of oil, temperature, and vibration. Scheduled teardowns occur at defined mileage or hour limits. Do not wait for failure to act. Tighten inspection intervals when you see rising heat, metal in the oil, or abnormal noise. Document every check result so that trends become visible over time. Mikura International supports locomotive maintenance teams with quality bearing components and technical guidance.

What Symptoms Indicate Excessive Railroad Engine Bearing Wear?

The writing is on the wall when excessive bearing wear appears in a locomotive engine. Early detection protects the engine, the train, and the crew.

Watch for common failure indicators and unusual vibration symptoms right away. Small changes often signal larger problems ahead.

Heat rise is one of the first warning signs. A bearing running hotter than normal points to lubrication loss or excessive friction.

Metallic noise deserves immediate attention. Grinding, whining, or knocking sounds often indicate that bearing surfaces are breaking down.

Discolored oil is another key indicator. Dark, milky, or glittery oil may carry metal particles from worn bearing surfaces.

Excess end play also signals trouble. Measure the axial movement of the crankshaft and compare it against manufacturer limits.

Do not ignore rumble, knock, or a harsher running feel. These symptoms often appear before bearing failure becomes visible.

Maintenance teams should measure clearances and log trends over time. Trend data reveals gradual wear that a single inspection might miss.

Remove the engine from service if measured clearances exceed approved limits. Continued operation can damage the crankshaft and surrounding components.

Shut the engine down before the journal seizes. A seized journal or failed axle under load can cause derailment and serious injury.

Mikura International recommends regular inspection schedules for locomotive engines. Consistent monitoring helps operators avoid costly unplanned failures.

Who Is Qualified to Measure EMD Engine Bearing Wear?

You rely on qualified personnel to measure EMD locomotive engine bearing wear. Qualified personnel include EMD-trained diesel technicians, certified railroad machinists, and OEM-authorized inspectors. These professionals know the engine model and the correct gauging method. General laborers should not handle this work. A documentation review must come first before anyone sets a micrometer. The review covers the maintenance manual, wear-limit tables, calibration records, and the work order. This step matches the procedure to the bearing. It also ensures every result is traceable.

Can Hot Bearings Be Measured After Cooling Completely?

A hot locomotive bearing gives a valid wear reading only after it cools completely. Testing confirms this principle holds, but only within clear limits. Technicians measure the axle journal only when it reaches ambient temperature. Time alone is not a reliable indicator of readiness. Cooling intervals are enforced so contraction finishes evenly across the journal.

Before logging any diameter, technicians verify caliper accuracy against a certified standard. The measured figures are then compared with the bearing’s baseline record. Any reading affected by residual heat is rejected and never logged. Mikura International recommends following this sequence on every locomotive bearing inspection. Disciplined measurement protects bearing life and supports dependable locomotive operation.

Why Choose Specialized Camshaft Bearing Press Tools for Locomotives?

Why Choose Specialized Camshaft Bearing Press Tools for Locomotives?

The Most Common Pain Point: Bearing Damage During Installation

Pressing a camshaft bearing into an EMD engine block leaves little room for error. A misaligned press can scratch the bore, block oil galleries, and force costly block repairs.

Generic fixtures rarely match the exact bore diameter, shoulder height, and oil-gallery geometry of EMD blocks. Mikura International supplies genuine EMD locomotive engine parts to help operators avoid these failures.

Common problems that cost locomotive operators time and money:

  • Bore scoring caused by off-axis pressing
  • Bearing walking or rotating inside the bore
  • Oil gallery blockage from misaligned seating
  • Pilot diameter mismatch with the bearing
  • Damaged shoulder or locating face
  • Overdriving the bearing past the specified seating load
  • Poor concentricity that leads to early camshaft wear
  • Repeated press attempts that weaken the bore
Pain PointRoot CauseCorrective Action
Bore scoringOff-axis pressing with a generic fixtureUse guided pilots matched to EMD bore specifications
Bearing walkingUnverified locating facesCheck locating faces against OEM drawings
Oil gallery blockageBearing seated out of alignmentConfirm gallery alignment before pressing
Pilot mismatchIncorrect pilot diameterMeasure pilot diameter against specification
Concentricity errorNo indicator checkConfirm concentricity with a dial indicator
Bearing distortionOverdriving the pressStop at the specified seating load

Why Specialized Tools Prevent These Failures

You choose specialized camshaft bearing press tools to match your EMD block’s exact bore diameter, shoulder, and oil-gallery geometry. Generic fixtures miss those dimensions.

They can push the bearing off axis, and that action scores the steel. You avoid this by verifying pilot diameter and locating faces against specification.

Guided pilots keep the bearing square during pressing. A dial indicator confirms concentricity before the job is final.

Do not overdrive the bearing past the specified seating load.

Selection Checklist

  • Confirm the tool matches the EMD block’s bore diameter
  • Verify the shoulder and locating face dimensions
  • Check that the oil-gallery geometry is supported
  • Require guided pilots that keep the bearing square
  • Confirm the seating load limit against the engine specification

Key Takeaways

  • Specialized tools match EMD block bore diameter, depth, and oil-gallery locations, preventing off-axis pressing.
  • Rated tools with verified tolerance ranges protect the bore from scoring and permanent steel damage.
  • Guided pilots and stepped shoulders keep bearings square throughout the press stroke.
  • Calibrated torque and load limits stop installation at the correct seating load, avoiding bore distortion.
  • Proper tooling supports controlled heating and lubrication, ensuring reliable bearing seating and locomotive uptime.

Why Generic Press Tools Fail on EMD Camshaft Bearings?

Why Generic Press Tools Fail on EMD Camshaft Bearings?

Generic press tools fail on EMD locomotive camshaft bearings because they ignore the block’s bore geometry. Standard fixtures rarely match the bore’s diameter, depth, or oil-gallery locations. Without that match, they push bearings off axis. That misalignment damages the bore and can permanently score the block’s steel.

Generic press tools miss the bore’s diameter, depth, and oil-gallery locations, pushing bearings off axis and scoring the block’s steel.

Start by verifying tooling compatibility before you touch the bearing. Confirm the pilot diameter, stepped shoulder, and locating faces match your locomotive engine’s specification. Do not improvise adapters. They introduce play you cannot measure.

Next, prioritize misalignment prevention. Use a guided pilot that holds the bearing square throughout the stroke. Apply torque control with a calibrated driver. Stop at the specified seating load rather than forcing the bearing home. Overdriving distorts the bore and compromises seating.

Finally, verify load distribution. Check that the bearing sits flush and rotates freely. Confirm that the lubrication holes align with the block’s oil passages. Bore protection matters on every locomotive overhaul.

What Makes a Camshaft Bearing Press Tool Effective?

A press tool is only as effective as its control over alignment, load, and fit. It acts directly on the camshaft bore in a locomotive engine.

You’ll get the best results when you verify the setup before pressing. Start with precision alignment checks. Confirm that the bearing, the bore, and the press ram sit square. Recheck after every adjustment. Do not rely on visual judgment alone. Use dial indicators or laser gauges to confirm concentricity.

Next, you’ll need consistent force control throughout the stroke. Set your hydraulic pressure limits before the job begins. Watch the load curve for sudden spikes. A spike usually signals a misaligned bearing or a burr in the bore. Stop immediately when a spike appears. You’ll protect both the bearing and the camshaft housing by pressing slowly and steadily.

Log each press. Record force readings and alignment values so you can trace any future failure. Keep hands clear of the ram at all times.

Which Press Tool Fits Your EMD Block Specs?

Which Press Tool Fits Your EMD Block Specs?

Once you have confirmed alignment, load limits, and fit, match the press tool to the locomotive engine’s block specifications. Start by pulling the EMD block’s bore dimensions from the service manual. Then select a tool rated for that camshaft bearing diameter.

Confirm alignment, load limits, and fit first, then match the press tool to the EMD block’s bore dimensions from the service manual and select one rated for that camshaft bearing diameter.

Compare bore tolerances against the tool’s stated range. Reject any tool that falls outside those limits. Verify the press tool’s rating label before each use. Check clearance before every pull to avoid galling and misseating.

Don’t skip the final check. Mount the tool on the block, then verify press alignment with a dial indicator before applying force. If the ram drifts, stop immediately and recheck your setup.

Wear eye protection, keep hands clear of the pinch zone, and never exceed the rated hydraulic pressure. You are responsible for a clean, square installation that protects both the crew and the engine. Log all measured values in the maintenance record.

How Do You Press Bearings Without Bore Damage?

Press bearings slowly, square, and lubricated, and you’ll keep the bore intact. Rushing the stroke or letting the press ram at an angle scores the bore wall and spins the bearing. Start every press with a clean, deburred housing and a verified tool fit. Check the bore diameter and surface finish before you begin.

Use controlled heating when the interference fit is tight. Warm the marine engine housing evenly to the temperature specified for your engine model. Never use an open flame. Keep the temperature below the limit that alters the bore’s metallurgy. Don’t skip heat-resistant gloves and eye protection.

Position the bearing square to the bore before applying force. Avoid misalignment by seating the pilot first and confirming the bearing enters without binding. If resistance spikes, stop, back out, and recheck alignment rather than forcing it. Verify the press force against the tool’s rated limit before you finish seating.

Do Locomotive-Grade Press Tools Pay Off for EMD Engines?

Do Locomotive-Grade Press Tools Pay Off for EMD Engines?

Locomotive-grade press tools usually pay for themselves on EMD engines. They prevent bore rework and reduce downtime. If you’re pressing camshaft bearings in an EMD block, precision matters. Low-quality tooling rarely holds alignment across repeated installs. A single out-of-square bearing can cost you an entire block. Long-life tooling with hardened guide surfaces and precision-machined pilots keeps bores true for years. Mikura International supplies tooling built for these demands.

Consider the math. A bore repair or block replacement can cost far more than the tool itself. A stranded locomotive also burns crew hours and disrupts schedules. Trackside reliability depends on getting the job right the first time. That means choosing tooling rated for the loads these engines demand.

Safety matters on every job. Inspect the press frame, threads, and load-rated components before each use. Keep hands clear of the pressure path at all times. Never exceed the rated tonnage. Verify the bearing is seated square before releasing any pressure. Stop immediately if the bearing binds.

Frequently Asked Questions

What Warranty Coverage Do Specialized Camshaft Bearing Press Tools Typically Include?

Warranty Coverage for Locomotive Camshaft Bearing Press Tools

Most specialized camshaft bearing press tools for locomotive engines carry a twelve-month warranty. The warranty typically covers material and workmanship defects, hydraulic component failures, and frame integrity.

Before operating the press, confirm that torque certification accompanies the unit. Valid calibration records protect your claim if a dispute arises. Keep documentation current throughout the press’s service life. Log maintenance, operator training, and load testing. Misuse, unauthorized modifications, and worn parts typically void coverage.

Can These Press Tools Be Used on Non-EMD Locomotive Engines?

Not automatically. Do not assume compatibility before completing the required checks.

You can use these press tools on non-EMD locomotive engines only after verifying compatibility. Start by comparing the tool against your engine’s bore dimensions and bearing specifications.

Confirm that engine-specific fixtures seat correctly. Check that the press operates within its hydraulic limits. Verify that the tool carries model certification covering your exact locomotive engine model.

Skipping any step can cause bearing misalignment, housing damage, or personal injury. Always consult the equipment documentation first.

How Often Should Press Tools Be Calibrated and Inspected for Accuracy?

Press Tool Calibration and Inspection for Locomotive Maintenance

Follow strict calibration intervals for locomotive press tools. Recalibrate every six months or after 500 press cycles, whichever comes first. Verify accuracy before every shift using certified gauges. Confirm that load readings stay within tolerance. Increase inspection frequency when press tools operate under heavy use. Schedule an annual performance audit for every press tool. Inspect hydraulic seals, alignment fixtures, and guide surfaces after any overload event. Always lock out the locomotive and press equipment before inspection. Document every calibration and inspection result. Accurate records support smooth audits and help maintenance teams track tool performance over time.

What Training Do Technicians Need Before Operating Hydraulic Bearing Press Equipment?

You need documented operator certification before operating any hydraulic bearing press in a locomotive workshop. Your training should cover press controls, pressure limits, and emergency shutdown procedures. Before every job, you will perform a risk assessment. Identify pinch points where hands or fingers can become trapped. Check for hose failure hazards before pressurizing the system. Verify load alignment on axle and wheelset bearings to prevent sudden shifts. You must demonstrate competence under supervision before working independently. Retrain whenever the equipment, pressure settings, or procedures change. Do not skip lockout/tagout training. Stored hydraulic energy can cause serious injury even after power is removed.

Which Safety Standards Govern Press Tool Use in Railroad Maintenance Facilities?

Safety Standards for Press Tool Use in Railroad Maintenance Facilities

Railroad maintenance facilities must satisfy OSHA requirements before operating any press tool on locomotive components. Start with 29 CFR 1910.147 lockout/tagout procedures. Isolate hydraulic power and bleed all residual pressure before servicing the press. Apply 29 CFR 1910.212 machine guarding requirements at every press station. Wear the personal protective equipment specified under 1910.132. Your facility’s railroad safety program should follow FRA oversight. Follow the manufacturer’s load ratings for every fixture and die. Inspect hoses, gauges, and fixtures before every shift. Never exceed rated capacity, even momentarily, during any pressing operation. Mikura International recommends documenting every inspection and training record to stay audit-ready.

How to Maintain Locomotive Engine Bearing Lubrication Systems

How to Maintain Locomotive Engine Bearing Lubrication Systems

Locomotive bearing lubrication problems can cause overheating, accelerated wear, and unplanned downtime.

Finding the cause early helps protect engine components and supports reliable operation.

Follow the locomotive’s model-specific EMD service manual and current maintenance guidance.

Use only approved procedures and parts suited to the engine and operating conditions.

CheckWhat to look forAction
Oil supplyLow level or interrupted flowVerify the supply using the approved procedure
Oil pressureReadings outside specified limitsStop and investigate before operation
Oil conditionContamination or unexpected changesDo not operate until the cause is identified
FiltersDamage, blockage, or incorrect installationInspect and replace as specified
BearingsAbnormal heat, noise, or visible damageKeep the locomotive out of service pending assessment
LeaksOil around lines, fittings, or bearing areasLocate and correct the source before restarting

Key maintenance precautions:

  • Select oil approved for the engine, climate, and operating conditions.
  • Do not choose oil by viscosity grade alone.
  • Do not mix oil brands unless compatibility is confirmed.
  • Secure the locomotive before inspection or cleaning.
  • Apply lockout/tagout and allow components to cool.
  • Check oil flow, pressure, filters, bearings, and leaks as directed.
  • Do not start the engine if damage or contamination is found.
  • Use genuine locomotive engine parts supplied by Mikura International when replacements are required.

Key Takeaways

  • Select oil approved for the locomotive’s EMD model and operating conditions; verify viscosity, formulation, and additive compatibility in current guidance.
  • Secure the locomotive and follow lockout/tagout procedures before inspecting accessible bearings, caps, fasteners, and oil passages.
  • Measure bearing oil flow and pressure at designated test points with calibrated gauges; check filters and leaks without bypassing alarms.
  • Clean bearings only at the specified maintenance interval, using approved methods and materials while preventing contamination of oil passages.
  • Inspect for wear, damage, leaks, and contaminated oil; report out-of-limit findings and do not start the engine if damage is found.

Choose Oil to Match EMD Specifications

Choose Oil to Match EMD Specifications

Select engine oil that meets EMD specifications for your locomotive model and operating conditions. Do not rely on viscosity grade alone. Check the engine manual and current EMD service guidance before ordering or filling. The approved formulation helps meet lubrication requirements and protect bearings under your locomotive’s temperatures, loads, and duty cycles.

Check that the oil’s viscosity falls within the approved range for your climate and operating profile. Do not use a heavier or lighter oil without written manufacturer approval. Viscosity affects oil flow during startup and film strength at operating temperature. Also verify additive compatibility when changing brands or topping up. Do not mix oils unless EMD guidance confirms they are compatible.

Keep product labels and delivery records available. Inspect containers for contamination, damage, or incorrect identification. Use clean, dedicated transfer equipment and follow site handling procedures. Before adding oil to the locomotive’s lubrication system, confirm that it meets the required specification.

Check EMD Camshaft Bearings Before Startup

After confirming the oil meets EMD specifications, inspect the locomotive’s camshaft bearings before startup. Secure the locomotive against movement, apply lockout/tagout procedures, and follow the engine service manual. Do not open bearing housings or remove components unless authorized by the procedure.

Inspect accessible bearing surfaces, caps, fasteners, and oil passages for scoring, cracks, looseness, sludge, or metal debris. Check for overheating discoloration and unusual wear. If you find damage or contamination, do not start the engine. Report the condition and arrange qualified repairs.

Review maintenance records and oil-analysis results for trends in wear metals or contaminants. Confirm the specified lubricant is present, and verify bearing lubrication using the approved pre-start procedure. Record observations, corrective actions, and unresolved concerns. Obtain required authorization before releasing the locomotive for startup, and keep personnel clear of moving parts.

Inspect Bearing Oil Flow, Pressure, and Filters

Inspect Bearing Oil Flow, Pressure, and Filters

Before startup, check locomotive bearing oil flow and pressure using the approved procedure and specified limits. Secure the locomotive against movement, wear required protective equipment, and use calibrated gauges at designated test points. Isolate the system before connecting instruments. Never loosen pressurized fittings.

CheckAction
Flow and pressureCompare readings with specified limits. Investigate abnormal values.
FiltersCheck indicators and inspect housings for leaks or damage.

During operation, monitor readings as directed. Respond promptly to sudden pressure drops, restricted flow, or rising bearing temperatures. Follow the maintenance procedure, including shutdown requirements.

Inspect filter housings, lines, and connections for seepage, looseness, or contamination. Replace filters only as specified. Confirm correct installation and sealing. Take oil samples using approved methods at designated ports. Label samples and send them for analysis.

Record readings, filter condition, and sample details. Report out-of-range results to qualified maintenance personnel before returning the locomotive to service. Never bypass a filter or defeat an alarm to keep the locomotive running.

Follow the EMD Bearing Cleaning Schedule

Follow the EMD maintenance manual’s bearing-cleaning schedule for the specific locomotive model and operating conditions. Use the specified interval, cleaning method, and approved materials. Do not substitute solvents or extend intervals without authorization.

Before servicing, secure the locomotive against movement and isolate the relevant equipment. Follow site lockout procedures, allow components to cool, and wear the required protective equipment.

Keep dirt, lint, and cleaning fluid out of oil passages and the lubrication system. Use clean, lint-free materials and dedicated tools. Collect waste fluid for proper disposal. Do not direct compressed air into bearing openings, as it can push contaminants deeper or create hazards.

Protect exposed surfaces during cleaning. Restore covers and connections according to the manual. Inspect filters at the specified service point, following the approved procedure and using replacement parts that meet the manual’s requirements.

Record the service date, operating hours, materials used, and any deviations in the maintenance log. If instructions conflict or conditions exceed manual limits, stop work and consult qualified maintenance personnel before returning the locomotive to service.

Check for Bearing Wear, Dirty Oil, and Leaks

Check for Bearing Wear, Dirty Oil, and Leaks

After cleaning, inspect accessible locomotive bearing surfaces and lubrication components for abnormal wear, discoloration, scoring, or oil leaks. Follow isolation and lockout procedures before opening guards or touching components. Hot oil and rotating machinery can cause serious injury.

Check bearing surfaces for pitting, cracks, uneven contact, and metal particles. Compare findings with maintenance limits. Do not return damaged bearings to service if they exceed those limits.

Inspect seals for hardening, cuts, looseness, or seepage. Check joints, hoses, fittings, and drain points for fresh oil. Trace leaks to their source instead of tightening connections blindly.

Collect an oil sample using the approved method. Check for water, sludge, fuel dilution, and metallic debris. Compare results with baseline readings and specified limits. Replace or filter oil only as directed by maintenance procedures.

Document bearing wear, sample results, and leaks. Report out-of-limit conditions promptly. Keep the area clean, contain spills, and verify repairs before restarting the locomotive.

Frequently Asked Questions

How Often Should Locomotive Engine Bearing Lubrication Systems Undergo a Complete Overhaul?

Overhaul a locomotive engine bearing lubrication system according to the manufacturer’s recommendations and the fleet maintenance program. There is no universal overhaul interval. Schedule inspections based on operating hours, condition-monitoring results, and service history. Arrange an earlier overhaul if you find contamination, pressure loss, abnormal bearing wear, or recurring faults. Record all inspections, repairs, and overhauls in the locomotive’s maintenance records.

What Safety Precautions Should Technicians Follow When Servicing a Lubrication System?

Before servicing a locomotive lubrication system, shut down the locomotive and isolate all energy sources using approved lockout procedures. Verify zero energy with suitable instruments. Allow hot components to cool, wear appropriate protective equipment, and keep clear of moving parts. Relieve system pressure according to the manufacturer’s instructions, then confirm gauges read zero before opening lines or filters. Use compatible tools, contain oil spills, and dispose of used oil properly. Before restarting, reinstall all guards and check for leaks.

Which Tools Are Needed to Diagnose Lubrication System Faults?

To diagnose lubrication faults in a locomotive, use calibrated pressure gauges, temperature probes, flow meters, and oil sampling kits. A multimeter can check electrical instrumentation, while a diagnostic scanner helps interpret fault codes. Keep suitable fittings, clean sample containers, and locomotive service data nearby. Verify instrument calibration, isolate equipment as required, and follow site lockout procedures before testing.

How Can Operators Monitor Bearing Lubrication Remotely?

Operators can monitor locomotive bearing lubrication remotely by tracking oil pressure, temperature, flow, and vibration with installed sensors. Transmit readings to a secure dashboard for continuous review. Compare live data with operating limits and historical trends. Set alerts to notify operators and maintenance staff when readings become abnormal. Regularly verify sensor calibration, communication links, and alert delivery. Treat remote readings as diagnostic aids, and follow approved procedures before inspecting equipment or changing operating conditions.

What Should Be Done if a Lubrication System Alarm Activates While the Locomotive Is Running?

If a lubrication system alarm activates while a locomotive is running, follow the applicable emergency and alarm procedures immediately. Notify the engineer, reduce the load, and stop at a safe location as procedures require. Record the alarm indication before resetting it. Inspect for oil leaks, low pressure, abnormal temperatures, or unusual noise. Use approved fault-isolation procedures to identify the cause. Do not resume operation until qualified personnel confirm the lubrication system is safe and authorize movement.

Why Replace Connecting Rod Bearings in Locomotives Regularly?

Why Replace Connecting Rod Bearings in Locomotives Regularly?

Regular bearing replacement protects engine health and uptime, supporting predictable maintenance windows in Australia.

Connecting rod bearings wear from heat, pressure, and friction. Wear changes clearance, impacting oil flow and lubrication efficiency, which can lead to knocking, reduced power, and unexpected outages.

In EMD locomotives, bearing wear is common due to heavy duty cycles. Proactive replacement minimizes unplanned downtime and costly repairs by preserving bearing geometry and oil film integrity.

Regular replacement also maintains fuel efficiency. Worn bearings elevate friction and parasitic losses, lowering locomotive performance during long hauls and steep climbs.

With Mikura International you gain access to genuine EMD Locomotive Connecting Rod Bearing parts and reliable on‑time delivery to support tight maintenance windows in Australia.

Key benefits of regular replacement:

  • Consistent engine clearance and oil film integrity.
  • Reduced risk of bearing seizure or main journal damage.
  • Lower maintenance cost over life cycle.
  • Improved reliability for critical running days and shunting tasks.

Below are practical steps to plan bearing replacement effectively.

  1. Inspect bearings at planned overhauls. Look for scoring, pitting, or excessive play.
  2. Check oil quality and filtration. Contaminants accelerate bearing wear.
  3. Confirm correct bearing type and fitment from Mikura International. Use torque specs from OEM manuals.
  4. Verify crankcase clearance and oil clearance targets after installation.
  5. Schedule downtime to align with maintenance windows in your Australian operations.
  6. Document part numbers and batch data for traceability and future sourcing.
  7. Validate engine performance after fitment with test run data and monitoring.

We at Mikura International provide technical support, genuine EMD Locomotive Connecting Rod Bearing options, and guaranteed on-time delivery for Australia customers.

Overview of locomotive engine reliability and maintenance

Locomotive reliability hinges on disciplined maintenance and timely component exchanges. Mikura International emphasizes predictable service windows, steady performance, and clear maintenance planning. Regular checks support durable operations and reduce surprise outages.

Role of connecting rod bearings in engine performance

Connecting rod bearings govern crankshaft motion and oil-film integrity. Worn bearings enlarge clearances, raise friction, and can elevate vibration and transient power loss. Timely bearing replacement helps preserve compression stability and engine smoothness.

Mikura International and commitment to dependable components

At Mikura International, we deliver reliable locomotive components with precision and speed. Our ISO-aligned standards and global sourcing network support on-time delivery for ALCO, EMD, GE, and WABCO engines. We back our EMD Locomotive Connecting Rod Bearing offerings with proven performance.

Expert Insight

“Locomotive reliability hinges on proactive maintenance and timely part replacements; for connecting rod bearings, maintaining tight clearances and stable oil pressure through timely replacements preserves compression, reduces vibration, and minimizes downtime.” , Industry Analyst

1. Preventing Bearing Wear Through Scheduled Replacement

Understanding wear mechanisms in EMD Locomotive Connecting Rod Bearings

Wear in EMD Locomotive Connecting Rod Bearings progresses with load cycles and oil film degradation. Surface fatigue reduces shell and journal integrity, widening clearances. Contaminants accelerate abrasive wear and scuffing, diminishing oil retention.

Thermal cycling and seating deficiencies create hot spots. Hot spots elevate friction and hasten wear. Differential cooling stresses can spall bearing material and cause misalignment.

Preventing Bearing Wear Through Scheduled Replacement

Recommended replacement intervals for heavy-duty diesel engines

  • Follow manufacturer-backed inspection intervals based on service hours or miles.
  • Use defined hour thresholds with margins for severe duty as per OEM guidance.
  • Maintain detailed maintenance records for accurate scheduling and traceability.

Table: comparative interval guidance by operating regime

Operating regimeSuggested interval (hours)Notes
Balanced duty cycle2,000-3,000Regular service, stable loads
Heavy haul/peak loads1,000-2,000Increased wear potential
Idle/low cycles3,000-4,000Less dynamic stress but oil degradation risk

2. Reducing Risk of Catastrophic Engine Damage

Consequences of Failed Bearings on Locomotive Operation

Failed bearings disrupt crankshaft motion and oil clearance. This can cause sudden power loss and unplanned downtimes. Loss of lubrication accelerates wear on journals and rods. Severe damage may trigger engine seizure or misalignment.

  • Unscheduled maintenance interrupts rail services
  • Higher risk of secondary failures in pistons and rods
  • Increased repair costs and longer rebuild times

How Early Replacement Mitigates Crankshaft and Piston Damage

Replacing bearing pairs before excessive wear preserves shaft alignment and oil film stability. Early changes reduce friction hotspots and thermal stress. Consistent bearing condition supports predictable engine performance under variable loads.

  • Maintains compression integrity across cylinders
  • Minimizes crankpin and piston ring wear
  • Lower probability of catastrophic crankshaft fracture
AspectImpact of Delaying ReplacementImpact of Timely Replacement
Oil film integrityDegrades, increasing metal-to-metal contactPreserved, reducing wear channels
Crankshaft alignmentDrifts under loadMaintained, stabilizing RPM and torque
Piston dynamicsHigher stress on rings and landsLower stress, smoother combustion

3. Enhancing Fuel Efficiency and Emissions Compliance

Impact of bearing condition on engine efficiency

Properly conditioned EMD Locomotive Connecting Rod Bearings minimize parasitic losses, reducing friction during high load cycles. This yields steadier torque delivery and helps maintain a consistent oil film that supports efficient cylinder charging.

  • Reduced mechanical resistance enhances thermal efficiency.
  • Stable clearances promote uniform combustion and power output.
  • Lower friction helps keep the engine cooler under heavy loads.

Maintenance and emissions compliance

Regular bearing replacement supports predictable combustion timing and emission control. Maintaining tolerances prevents irregular fuel burn that can raise NOx and particulates. Timely maintenance aligns with OEM guidance and Australian standards for locomotives.

  • Consistent lubrication aids stable exhaust gas temperatures.
  • Controlled combustion minimizes anomalies that trigger recalls or non-compliance alerts.
  • Documented bearing service history assists audits and reporting.
ParameterPoor bearing conditionOptimal bearing condition
Frictional lossElevatedMinimized
Fuel efficiencyDeclines under loadMaintains high efficiency
Emissions consistencyInconsistentStable across cycles

4. Cost Management and Total Cost of Ownership

Short-term vs long-term costs of regular bearing replacement

Regular bearing replacement incurs upfront costs for parts and skilled labor. Plan for periodic stocking and dedicated maintenance windows to minimize disruption. Over the life cycle, scheduled replacements reduce the risk of large, unplanned expenditures.

Cost Management and Total Cost of Ownership
  • Initial procurement costs for high quality EMD Locomotive Connecting Rod Bearing
  • Labor hours for inspection and installation
  • Scheduled downtime to align with maintenance plans

Downtime impact and part reliability considerations

Downtime affects fleet productivity and service level agreements. Reliable parts and standardized procedures reduce rework and spare parts pressure. Durable bearings enable longer maintenance intervals and more predictable planning.

  • Downtime duration directly influences operational costs
  • High reliability components reduce rework and returns
  • Inventory redundancy supports rapid turnaround needs
AspectShort-term costLong-term cost
Parts and materialsModerate, recurringLow to moderate, predictable
Labor and downtimeScheduled window costsMinimized due to fewer failures
Risk of unscheduled repairLow with regular replacementSignificantly reduced over time

5. Selection of High-Quality Replacement Bearings

Criteria for choosing Mikura International components

Choose Mikura International for proven reliability and regional support. Prioritize bearings that meet OEM tolerances and material standards. Ensure traceable lot labeling and documented quality checks.

Selection of High-Quality Replacement Bearings
  • OEM-grade material composition
  • Certified manufacturing processes
  • Comprehensive inspection records
  • Availability of regional technical support in Australia

Compatibility and performance benchmarks for ALCO, EMD, GE, WABCO engines

Compatibility covers crankpin sizing, bearing bore, and clearance tolerances. Performance benchmarks include surface finish, load capacity, and oil film retention under high heat.

  • ALCO and EMD blocks: matched clearance and stud thickness
  • GE and WABCO variants: verified cross-compatibility and retention features
  • Consistent radius profile to prevent oil starvation zones
  • Long-term lubricity and reduced micro-pitting under cyclic loads
Engine FamilyKey Compatibility NotesPerformance Benchmark
ALCOCrankpin diameter and bearing bore alignmentStable clearance under full-load cycles
EMDOil film retention and surface finishLow wear rate over service interval
GERetainer and fitment compatibilityConsistent torque delivery
WABCOCross-compatibility with shared housingsPredictable lubrication performance

6. Installation best practices and inspection protocols

Pre-installation checks and tolerances

Prepare a clean work area with proper tooling and a controlled environment. Verify the EMD Locomotive Connecting Rod Bearing part numbers align with the specification. Confirm crankshaft journals and connecting rod housings are within OEM tolerances before fitting.

  • Inspect lubrication passages for obstructions
  • Verify journal surface finish meets minimum roughness requirements
  • Check bearing tangs, chamfers, and oil holes for correct orientation

Post-installation testing and routine inspections

After installation, run functional checks to confirm seating and oil film formation. Execute a controlled engine cycle and monitor clearance indicators and oil pressure trends.

  • Record initial oil pressures at idle and rated RPM
  • Use a bore scope to inspect bearing seats for micro-movement
  • Schedule routine inspections at defined service intervals to detect wear progression
ActivityKey checkAcceptable condition
Pre-installationJournal condition, bearing fitWithin OEM tolerances, clean seating
Post-installationOil film and clearanceStable film, no abnormal play

7. Predictive Maintenance Tools and Data

Using vibration, oil analysis, and thermal data to time replacements

Collect baseline vibration spectra for each EMD locomotive family and monitor for shifts that indicate bearing wear or looseness.

Predictive Maintenance Tools and Data

Analyze oil samples for metal content and particle size distribution to map wear progression and adjust replacement timing accordingly.

Track bearing temperature rise during operation to identify friction hotspots and schedule inspections before failures occur.

  • Establish baseline vibration spectra for each EMD locomotive family.
  • Track trends in metal content and particle size in oil samples.
  • Set warning thresholds for oil temperature and outlet oil pressure.

Leveraging service data from Mikura International and OEM records

Access Mikura International technical service data to align replacement timing with validated wear curves and regional operating profiles.

Cross reference OEM maintenance intervals and bearing life estimates for accuracy and consistency across fleets.

Use field reports to refine regional maintenance calendars in Australia and improve forecast confidence.

  • Compare actual wear indicators against OEM reference profiles.
  • Incorporate regional operating profiles to adjust intervals.
  • Log all sensor readings for continuous improvement.

FAQ

What is the purpose of replacing the EMD Locomotive Connecting Rod Bearing regularly?

  • Prevent wear progression that can lead to crankshaft misalignment and reduced efficiency.
  • Preserve the integrity of the oil film and minimize friction under high load cycles.

How do I determine replacement timing?

  • Follow OEM-backed service intervals based on engine family, load profile, and operating hours.
  • Correlate observed wear indicators with vibration and oil analysis data to refine timing.

What are signs of bearing wear to watch for?

  • Unusual engine noise or mild misfire during heavy operation.
  • Rising oil consumption and shifts in oil pressure trends.

Which Mikura International bearings are recommended?

  • Bearings certified for cross compatibility with EMD locomotives and related engines.
  • Components designed to retain oil film under high temperatures and loads.

What is the impact on downtime and maintenance costs?

  • Regular replacements reduce unscheduled outages and extend engine life.
  • Plan downtime windows to minimize disruption and align with scheduled maintenance.

Expert Insight

“Regular bearing replacement, guided by engine family, load profile and service hours, protects crankshaft efficiency by preserving oil film and reducing wear during high-load cycles.” , Industry Analyst

Conclusion

Concluding the guide, Mikura International emphasizes dependable replacement bearings as a maintenance discipline that supports sustained locomotive availability in Australia. The focus remains on aligning part selection and service timing with OEM guidance and regional operating patterns.

Key takeaways:

  • Scheduled replacements mitigate unexpected outages and help protect crankshaft and bearing assemblies under heavy duty cycles.
  • High quality Mikura components sustain oil film integrity and reduce parasitic losses during extended load profiles.
  • Evidence-based maintenance planning, supported by vibration and oil analysis, informs precise timing and reduces downtime.

Our team continues to provide precise part matching, regional logistics support, and technical guidance to keep locomotives in productive service, with a clear focus on reliability and traceability.

Why Replace Diodes in EMD Locomotive Voltage Regulators?

Why Replace Diodes in EMD Locomotive Voltage Regulators?

You rely on EMD locomotives to stay on schedule. Diode health in the voltage regulator is critical for reliability. Replacing worn diodes prevents voltage spikes and regulator failure.

Key benefits include better regulation, reduced heat, and fewer unplanned outages. This saves maintenance time and keeps trains moving on time.

Our approach focuses on the specific needs of EMD locomotive systems. We select high quality diodes that meet the exact ratings for your regulator. This ensures compatibility and long service life.

Common issues indicate when replacement is needed. Look for excessive regulator heat, irregular voltage output, or repeated fuse blows. These signs point to diode degradation.

Concrete scenarios and actionable steps

Scenario: An EMD hauled train experiences intermittent voltage dips during peak load, causing lighting flicker in passenger cars.
Action: Schedule a diode health check during the next major maintenance window and measure regulator output under load with a calibrated multimeter. If the diode forward drop increases or leakage rises, replace the pair rather than a single diode to restore symmetry.

Scenario: A yard switcher repeatedly blows a fuse after a short idle period.
Action: Inspect the regulator bridge for diode cracking or solder joint fatigue. Replace with OEM-grade diodes rated for the regulator current, and reflow joints to prevent micro-cracks that mimic failure later.

Scenario: High regulator heat persists after a clean fan and vent path check.
Action: Conduct a thermography scan on the regulator module to locate hotspots. If hotspots align with diode clusters, proceed with replacement and verify heat sinking in the housing to avoid new hot spots.

Practical steps for maintenance teams

  1. Use OEM-grade or higher reliability diodes designed for locomotive regulators.
  2. Verify voltage and current ratings match your regulator spec sheet.
  3. Inspect related components during replacement to prevent cascading failures.
  4. Document part numbers and batch codes for traceability.
  5. Test the regulator under load after replacement and record performance data for the maintenance log.

For sourcing managers, timing matters. Plan replacements during planned maintenance windows to minimize disruption. Mikura International offers ready-to-ship diode sets tailored to EMD regulator models, with batch documentation and a compatibility guarantee.

Expert Insight

“Use OEM-grade or higher reliability diodes designed for locomotive regulators, ensure voltage and current ratings match your regulator spec sheet, and document part numbers for traceability to prevent cascading failures during planned maintenance windows.” , Industry Analyst

Diodes in EMD locomotive voltage regulators handle high currents and fast switching. Faulty diodes cause regulator instability, voltage dips, and unexpected shutdowns. In harsh rail environments, failures raise maintenance costs and downtime. Regular diode checks protect power quality, shield surrounding components, and extend regulator life. Mikura International provides reliable replacement components that restore performance quickly and safely.

Why Mikura International focuses on reliable replacement components.

You gain quick access to proven, ISO-certified diode replacements for EMD regulators. Our team sources parts that meet strict electrical and environmental standards. This ensures compatibility, reliability, and long service life. We minimize supply gaps with on-time delivery and integrity in every transaction. Our priority is to support spare parts sourcing managers in Australia with accurate, fast, ethical service.

  • Ethical sourcing: components from approved suppliers with traceability.
  • Technical assurance: parts tested for reverse recovery and surge handling.
  • Delivery reliability: guaranteed on-time shipment to keep maintenance windows intact.

In practical terms, implement a diode health plan within your maintenance cycle. 1. Inspect diodes during routine regulator checks using a handheld multimeter to verify forward voltage drop remains within specification. 2. Schedule a full diode bench test every 12 to 18 months, including reverse recovery time and peak current capability. 3. Maintain an inventory buffer for critical diodes to prevent downtime when a part is flagged or out of stock. 4. Document results in a maintenance log and correlate with regulator uptime data to identify recurring failure patterns.

Focus AreaMikura International Approach
Part QualityISO-certified, audited suppliers
DeliveryOn-time to reduce downtime
SupportTechnical guidance for replacement

Expert Insight

“Reliable, ISO-certified replacements enable rapid, safe restoration of performance with traceable sourcing, on-time delivery, and technical guidance that minimizes downtime for spare parts managers.” , Industry Analyst

1. Understanding EMD Voltage Regulators and Diodes

Role of diodes in regulator circuits

Diodes act as fast switching elements in EMD voltage regulators. They steer currents, clamp voltages, and protect switching transistors during throttle transitions. Selecting the right diodes prevents regulator oscillations and helps maintain stable output.

  • Rectification paths control current flow during charging and discharging cycles.
  • Fast recovery diodes minimize reverse recovery losses at high switching frequencies.
  • Forward voltage characteristics influence overall regulator efficiency and thermal behavior.

How diodes affect performance and reliability in locomotives

Diodes shape reliability and uptime by controlling heat and electrical stress. A degraded diode elevates hotspot formation and increases the risk of regulator failure in harsh rail environments. High quality diodes extend service intervals and reduce maintenance windows.

  • Thermal behavior from diode operation governs cooling requirements.
  • Electrical stress from transients tests diode endurance and longevity.
  • Consistency of reverse recovery affects surge protection for the regulator network.
AspectImpact on the Regulator
EfficiencyLow forward drop preserves power loss margins and improves thermal margins.
Thermal LoadHigher quality diodes reduce hotspot formation in modules.
ProtectionFast recovery limits voltage overshoots during switching events.

For sourcing managers, align diodes with regulator design, switching speed, and environmental ratings. This alignment minimizes early failures and extends regulator life in Australian operations. In practice, specify diodes with a low total ionizing dose tolerance for onboard electronics and verify vendor data sheets include a minimum 50 kA surge rating for wind gust events typical in coastal rail corridors. Mikura International recommends validating diode performance under simulated throttle ramps and ambient temperatures from -40°C to 85°C before final sign-off.

2. Common Diode Failures in Harsh Locomotive Environments

Thermal stress

Elevated ambient temperatures accelerate diode aging. Repeated thermal cycling causes junction fatigue and die attach cracking. This raises forward voltage drift and leakage current. Proper derating minimizes these effects.

  • Hot spots in power modules accelerate failure.
  • Inadequate cooling compounds thermal stress on diodes.
  • Delayed heat dissipation reduces regulator efficiency.

Vibration

Locomotives expose components to continuous vibration. Mechanical stress loosens interconnections and damages bond wires. Vibration can misalign heatsinks, worsening thermal conditions. Over time, contact resistance rises and failures propagate.

  • Loose solder joints increase intermittent faults.
  • Bond wire fatigue may lead to open circuits.
  • Module seating integrity affects thermal paths.

Electrical transients

Transients from regenerative braking, switching events, and load changes stress diodes beyond steady state. Recovered energy can trigger overshoots and reverse recovery spikes. Proper transient handling reduces ripple and protects adjacent devices.

  • Surge events amplify reverse recovery losses.
  • Inadequate snubbing raises voltage overshoot risks.
  • Insufficient protection elevates risk of secondary failures.

Symptoms indicating diode degradation

Early signs help prevent unexpected outages. Look for abnormal heating near diode clusters, rising junction temperatures, and unusual regulator noises. Increased leakage current often signals aging diodes.

SymptomLikely Cause
Excessive heat in diode areaThermal degradation or poor cooling
Intermittent regulator faultsLoose connections or bond-wire fatigue
Voltage overshoot during switchingInadequate transient protection

Documented symptoms guide timely diode replacement. This reduces downtime and stabilizes regulator performance in Australian operations.

3. Benefits of Replacing Diodes with High-Quality Parts

Improved reliability and reduced downtime

High-quality diodes stabilize regulator output during load steps, preventing voltage dips that can trigger equipment faults. In Australian operations, this translates to fewer unexpected outages during peak afternoon loads when solar generation fluctuates.

Reliable parts withstand harsh ambient conditions with minimal drift, ensuring consistent performance across coastal and desert sites alike.

  • Lower failure rates prevent unplanned maintenance windows by reducing the need for on-site diagnostics.
  • Consistent switching reduces nuisance trips in distributed energy setups, such as remote substations.
  • Extended service intervals boost fleet availability by aligning part replacements with calendar planning rather than reactive calls.

Enhanced electrical protection and longevity

Robust diodes offer stronger reverse recovery resilience, which protects switch-mode power supplies and nearby sensors from transient surges during load transients or switching events.

Superior derating preserves performance through heat cycles, maintaining regulator accuracy in high-temperature environments typical of inland Australian sites.

  • Better surge handling guards the regulator network against temporary overvoltages from lightning or grid disturbances.
  • Stable leakage characteristics reduce parasitic heating, extending component life in sealed enclosures.
  • Longer mean time between failures supports uptime goals by decreasing the frequency of on-site maintenance checks.
BenefitImpact
Regulator stabilityMore consistent output under varying loads, even during rapid load steps or intermittent generation.
DowntimeFewer repair events and quicker return to service after disturbances.
Maintenance planningPredictable replacement intervals simplify scheduling and inventory management.

4. Selection Criteria for Replacement Diodes

Choose diodes that fit the EMD regulator design and Australian operating conditions. Ensure compatibility with the module topology and heat management practices. This section outlines the essentials to guide sourcing decisions.

Voltage, current ratings, and reverse recovery characteristics

Match the diode voltage rating to the regulator’s maximum bus voltage. Pick current ratings that exceed peak load needs. Review reverse recovery time to cut switching losses and spike risks.

  • Voltage rating: at least 20 percent above the maximum system voltage.
  • Current rating: continuous and surge specs above regulator demand.
  • Reverse recovery: fast recovery suits high frequency operations.

Environmental ratings and certification standards

Diodes must endure locomotive vibration and ambient temperatures. Check thermal derating guidance and encapsulation quality. Verify compliance with rail industry standards.

  • Temperature range suitable for engine room and cab environments.
  • Vibration and shock tolerance aligned with Australian rail norms.
  • Certifications: ensure alignment with rail-specific quality frameworks and supplier QA processes.
CriterionWhat to verify
Voltage ratingBuffer above maximum bus voltage by at least 20%
Current ratingExceeds peak load and includes surge margin
Reverse recoveryLow recovery time to reduce switching losses
Environmental ratingThermal derating, vibration, and moisture tolerance
CertificationsRail-specific quality and safety standards

5. Replacement Process and Best Practices

Step-by-step replacement workflow

Prepare the work area and confirm part numbers before starting. 1. Power down the regulator module and remove access panels. 2. Discharge any stored energy safely per standard procedure. 3. Document existing diode layout and take high-resolution photos for reference. 4. Desolder or unsolder old diodes with proper heat management. 5. Inspect adjacent components for heat damage or mounting fatigue. 6. Install replacement diodes with correct orientation and secure solder joints. 7. Reassemble the module and verify connector integrity. 8. Reconnect power and perform a controlled test run at low load. 9. Gradually increase load to normal operating conditions while monitoring signals. 10. Record test results and update maintenance logs for traceability.

  • Follow the regulator manufacturer guidelines for torque on mounting hardware.
  • Use anti-static practices to protect sensitive devices during replacement.
  • Maintain clean soldering and avoid cold joints that cause intermittent faults.

Quality control and testing post-installation

Execute functional tests to confirm proper diode operation. 1. Check forward voltage and reverse leakage at ambient conditions. 2. Validate switching behavior under stepped load profiles. 3. Monitor regulator output stability for several cycles.

  • Perform thermal imaging to verify even heat distribution around new diodes.
  • Run a vibration test to ensure components stay seated under typical rail conditions.
  • Compare post-installation data against baseline measurements stored in the maintenance system.
AspectBest Practice
DocumentationCapture part numbers, torque values, and test results in the maintenance log.
SafetyLockout tagout procedures and energy isolation must be documented.
TraceabilityKeep replacement diodes with batch codes for future audits.

6. Cost Considerations and Total Cost of Ownership

Cost decisions should balance initial outlay with long term reliability. The right diode choice lowers warranty and service costs over time.

Upfront vs. long term savings

  • Higher quality diodes may cost more initially but reduce failure rates in harsh environments such as coastal Australia where humidity accelerates corrosion.
  • Fewer field visits save travel and labor expenses for Australia operations by reducing truck rolls during remote outages.
  • Better protection lowers risk of collateral gear damage in regulators, preventing cascading downtime in critical mining or telecom sites.
  • Lower leakage and tighter tolerances yield steadier regulator performance, translating to fewer trim adjustments in low-temperature operations.
MetricImpact
Unit pricePremium diodes cost more upfront but extend service intervals
Downtime costLower with robust parts during peak seasons
Maintenance intervalExtended with durable components and better thermal design
Warranty coverageMore comprehensive with reputable brands and traceable QA

Impact on maintenance schedules and uptime

  • Preventive diode replacement aligns with planned outages, for example during scheduled network maintenance windows in regional hubs.
  • Predictable performance reduces unexpected regulator trips, which can trigger safety interlocks in industrial systems.
  • Documented parts provenance aids audits and spares planning, supporting ISO 9001 and supplier QA requirements.
  • Enhanced heat management protects nearby components and lowers cascade maintenance in densely packed enclosures.
ConsiderationEffect on TCO
Spare inventory ageStable stock reduces last minute orders and expedited freight
Repair cycle timingLonger cycles improve fleet availability and battery longevity
Regulator reliabilityFewer component related faults and recall risk

Expert notes stress evaluating supplier QA, batch traceability, and compatibility with EMD module topologies to lock in long term savings. Mikura International recommends validating a supplier’s corrective action reports and test data from representative production lots to ensure consistency across deployments.

FAQ

What qualifies as a high quality diode for EMD regulators?

  • Choose diodes with robust surge ratings and correct voltage and current specs, and verify they meet relevant railway or locomotive standards.
  • Look for proven reverse recovery performance under high di/dt conditions typical of regenerative braking events.
  • Verify environmental ratings match harsh locomotive conditions, including vibration, wide temperature ranges, and exposure to dust or fine particulates.

How often should diodes be inspected during maintenance?

  • Schedule visual checks every 6 to 12 months based on service intensity and operating hours captured by the onboard maintenance system.
  • Include thermal profiling to spot hotspots around diode packs and verify cooling airflow with a handheld anemometer.

What signals indicate diode degradation?

  • Unstable regulator output and increased ripple measured at the test point under load.
  • Frequent regulator trips or abnormal heating near the diode area, plus occasional open circuit or shorted diode readings during insulation resistance tests.

What is the typical replacement workflow?

  • Power down and isolate energy sources using lockout procedures, then confirm zero energy with a multimeter.
  • Remove the heat sink and desolder obsolete diodes with proper heat management, using preheating and no-clean flux compatible tools to minimize PCB stress.
  • Install replacements with correct polarity and verify solder integrity, including post-solder inspection and vacuum reflow if required.

How does diode choice affect total downtime?

  • Higher reliability parts reduce unplanned outages and field service calls, shortening repair windows by up to 40 percent in some fleets.
  • Durable diodes simplify maintenance scheduling and inventory planning, enabling predictive stocking based on MTBF data from manufacturers.
QuestionShort Answer
CompatibilityMust align with EMD regulator topology and part numbers, including board footprint and thermal pad layout.
WarrantyPrefer brands offering strong warranty coverage and batch traceability, with documented lot-level QA data.
TestingPost install tests should confirm forward voltage, leakage, switching stability, and thermal performance under rated load.

Key takeaways

Replacing diodes in EMD locomotive regulators is essential for reliability. High quality parts reduce regulator trips and shield surrounding components. A structured replacement process minimizes downtime and preserves fleet performance. For Australian operators, plan around regional heat and altitude variations to maintain performance margins. When done correctly, you gain longer regulator life and fewer field failures.

  • Prioritize diodes with robust surge ratings and proven reverse recovery.
  • Match environmental specifications to Australian locomotive conditions, including temperature and dust exposure.
  • Integrate replacement into planned maintenance to avoid unscheduled outages, scheduling swaps during overnight crews or depot downtime.
AspectImpact
ReliabilityDurable diodes reduce regulator failures and protect auxiliary circuits during peak loads.
DowntimeScheduled swaps minimize on-site disruptions and engine removal requirements.
Maintenance planningClear provenance simplifies spares strategy and vendor coordination for bulk orders.

How Mikura International supports locomotive reliability

We deliver certified, traceable diode replacements tailored to EMD regulator topologies and the common field configurations seen on Australian fleets. Our team provides rapid responses to inquiries and coordinates on-time shipments, even during peak maintenance windows. We align offerings with ISO standards and industry certifications to uphold integrity in every part we supply, and we maintain a serial-based record for each batch to ease audits.

  • Ethical sourcing and batch traceability for every diode package, with documented lot codes.
  • Technical guidance on voltage and current compatibility with existing regulators, including derating in high ambient conditions.
  • Quality control and post-install testing to confirm proper functionality, featuring bench and engine-side checks before return to service.
Translate »