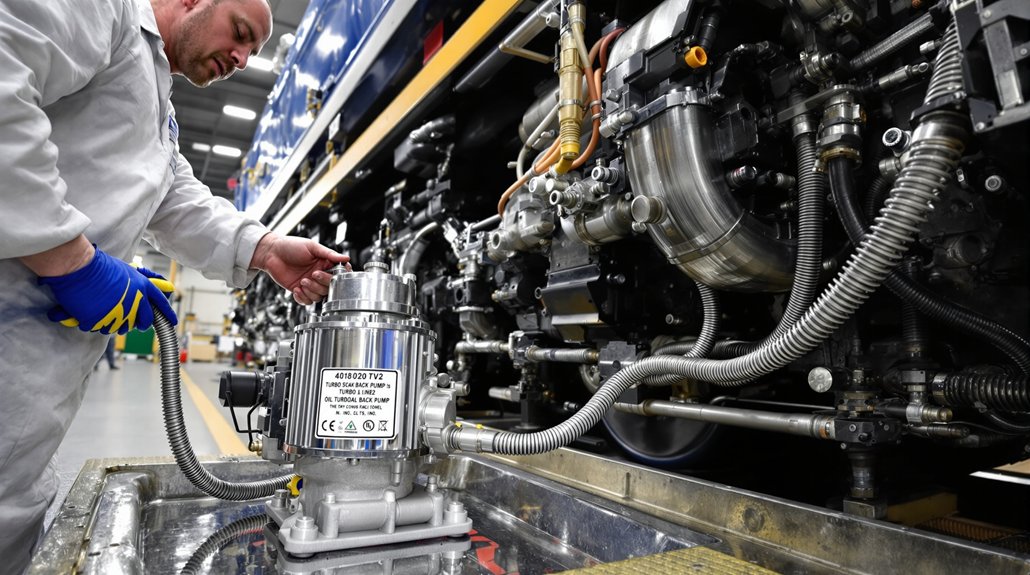
Soak Back Pumps: The Key to Locomotive Turbocharger Longevity

Soak Back Pumps: The Key to Locomotive Turbocharger Longevity

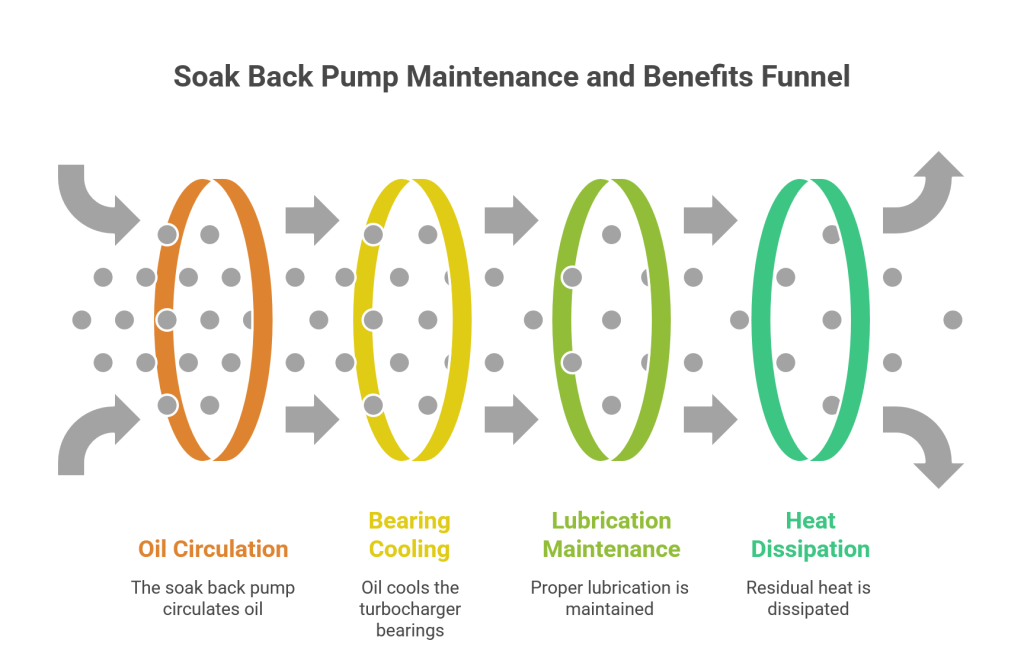
The soak back pump is critical for locomotive turbocharger longevity by preventing oil coking, which causes over 90% of turbocharger failures. It works by circulating oil for up to 35 minutes after engine shutdown to cool bearings, maintaining proper lubrication and dissipating residual heat. Key maintenance includes monthly oil flow checks, filter replacement every 30,000-60,000 miles, and regular oil analysis. Performance benefits include extended turbocharger life by 50-100%, significant maintenance cost savings, and reduced downtime.

1. The Critical Role of Soak Back Pumps in Turbocharger Longevity
The Critical Role of Soak Back Pumps in Turbocharger Longevity

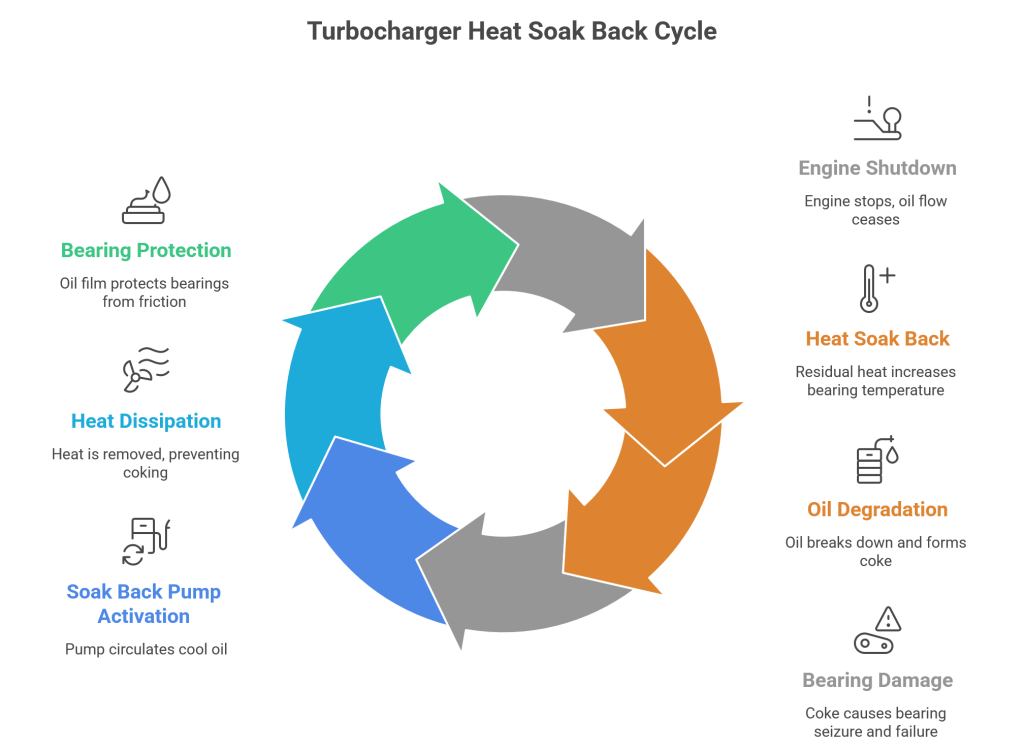
Locomotive turbocharger failures represent one of the most significant maintenance challenges in heavy-duty diesel operations. A significant proportion of these failures are directly linked to lubrication oil problems, including contamination, starvation, and thermal breakdown. These issues lead to costly repairs, operational downtime, and reduced engine reliability. The primary technical challenge addressed by the soak back pump is the phenomenon of heat soak back-the rapid temperature increase in turbocharger bearings immediately after engine shutdown, which can cause residual oil to coke and solidify, leading to bearing seizure and shaft failure.

1.1 The Oil Coking Crisis: Temperature Thresholds and Bearing Damage

Oil coking is a critical failure mode where lubricating oil, exposed to intense residual heat, thermally degrades and forms solid carbon deposits on bearing surfaces and oil passages. This process compromises lubrication and can cause catastrophic failure. Experimental data reveals specific temperature thresholds that define this risk.

  • Onset of Coking: In used engine oil, the formation of coke deposits can begin at temperatures as low as 150°C.
  • Post-Shutdown Temperature Rise: When an engine is switched off after running under load, the temperature of the turbocharger bearing housing can climb 25°C higher than its temperature at the moment of shutdown.
  • Peak Temperatures: Under high-load conditions without active cooling, bearing housing temperatures can reach 175°C, far exceeding the coking threshold for many oils.

This thermal dynamic creates a vicious cycle: as oil cokes, it restricts oil flow and increases friction, which generates more heat and accelerates further coking.

1.2 The Dominance of Oil-Related Failures

Industry analysis consistently identifies issues with the lubricating oil system as the leading cause of turbocharger malfunctions. Problems range from the oil’s physical and chemical properties to delivery system failures. Common failure pathways include:

  • Oil Starvation: Caused by blocked feed lines, pump failures, or insufficient oil pressure, leading to immediate bearing wear and seizure.
  • Oil Contamination: The presence of dirt, carbon particles, or degraded oil additives accelerates wear and can clog critical oil passages.
  • Oil Breakdown and Coking: As detailed above, this is a direct consequence of inadequate post-shutdown cooling and is a primary target of soak back pump operation.

These failure modes underscore that turbocharger longevity is less about the turbocharger itself and more about the integrity and management of its lubrication system.

1.3 The Heat Soak Back Phenomenon: A Technical Breakdown

Heat soak back is the process where residual thermal energy from the hot turbine housing and wheel conducts radially inward through the central bearing housing after oil flow from the main engine pump ceases. This energy has no effective heat sink without continued oil circulation, causing bearing temperatures to spike. The consequences are severe:

  1. The thin oil film on precision bearings evaporates or chemically breaks down.
  2. Metallic contact increases, causing friction, micro-welding, and accelerated wear.
  3. Oil trapped in the hot housing begins to cook, forming hard carbon deposits that abrade surfaces and eventually block oil passages entirely.

This process is not gradual; it occurs within the first few critical minutes after shutdown, making immediate intervention essential.

1.4 The Soak Back Pump as an Engineering Solution

The soak back pump is engineered specifically to interrupt this failure sequence. It is an electrically driven auxiliary oil pump that activates automatically upon engine shutdown. Its core function is to continue circulating cool, fresh oil through the turbocharger bearings for a controlled period, typically up to 35 minutes as managed by the Locomotive Control Computer (LCC). This active cooling serves two vital purposes:

  1. Heat Removal: It carries away residual heat, preventing the bearing temperature from reaching the critical coking threshold.
  2. Bearing Protection: It maintains a protective oil film on the bearings during the turbocharger’s rotational coast-down, preventing dry friction.

Modern soak back pumps, such as those designed for Automatic Engine Start-Stop (AESS) systems, incorporate advanced features for reliability in demanding cycling applications. These include brushless induction motors to eliminate brush maintenance, liquid-cooled electronics to prevent heat-related failures, and hardened pump components for extended service life, with some designs touting maintenance-free operation for up to 10 years.

1.5 Implications for Maintenance Strategy

For experts managing locomotive and marine engine fleets, the soak back pump transforms the maintenance paradigm from reactive repair to proactive preservation. Its proper function is not optional but foundational to achieving advertised turbocharger service life. Key maintenance practices directly informed by this understanding include:

  • Verifying Pump Operation: Standard procedures dictate checking oil flow through the gear train with the engine shut down and the soak back pump motor running.
  • Adhering to Filter Service Intervals: The soak back filter protects the pump and turbocharger. Its replacement interval (often aligned with the turbocharger filter at 30,000-60,000 miles) is influenced by load, oil type, and operating conditions, and should not be excessively extended.
  • Integrating Oil Analysis: A rigorous lube oil analysis program is strongly recommended to monitor oil condition and wear metals, providing early warning of system issues that could affect the soak back system’s effectiveness.

In conclusion, the soak back pump plays a non-negotiable role in safeguarding turbocharger investment. By directly mitigating the primary cause of oil-related failures-post-shutdown heat soak back-it is a critical component for ensuring longevity, reliability, and cost-effective operation in heavy-duty diesel applications.

2. Technical Architecture: How Soak Back Pumps Work
Technical Architecture: How Soak Back Pumps Work | Operational Process

The soak back pump is a critical auxiliary lubrication system engineered to solve the thermal management challenges of turbocharged locomotive diesel engines. It operates independently from the main engine oil circuit to provide targeted cooling and lubrication to the turbocharger during two critical periods: immediately after engine shutdown and before engine startup.

2.1 System Components and Operational Architecture

The system consists of several integrated components:

  • Pump and Motor Assembly: The core is an electrically driven pump. Standard locomotive units use a DC motor, typically rated at 3/4 HP and operating at 74 VDC input with a speed of 1200 RPM. The pump is a gear-driven design for consistent delivery. Configurations include traditional horizontal mounts (e.g., Part Number 4947308R for EMD 645 engines) and modern vertical designs with integrated AC motors and inverters.
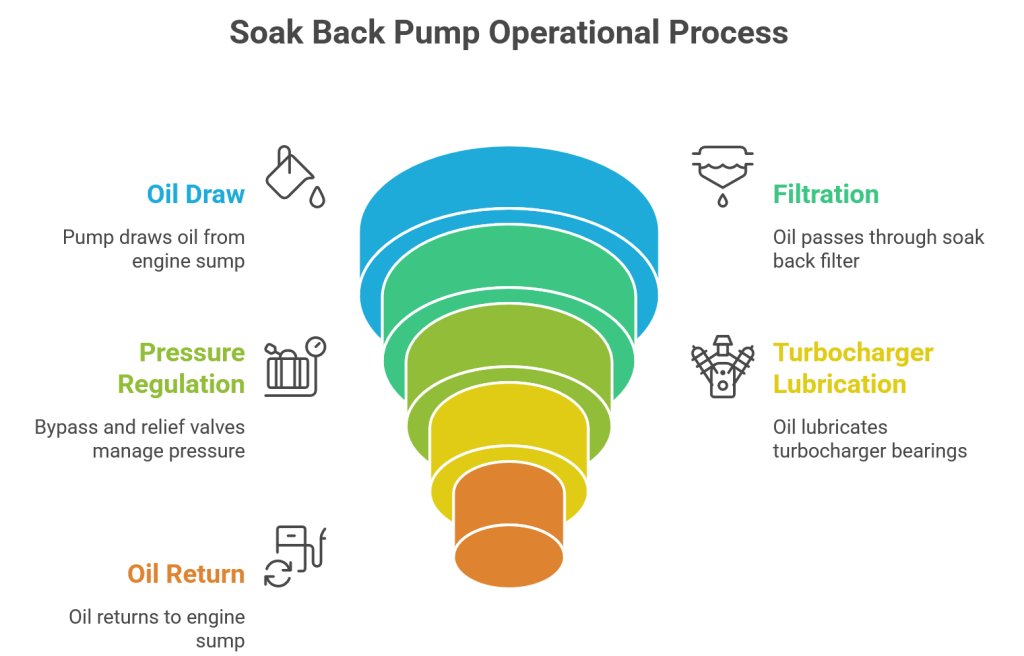
  • Filtration and Pressure Regulation: Oil passes through a dedicated soak back filter. A bypass valve within the filter housing, typically set at 70 PSI, opens if the filter clogs, ensuring uninterrupted oil flow to the turbocharger. A separate relief valve in the filter head, often set at 32 PSI, returns oil to the engine sump if the turbocharger is already being lubricated by the main engine pump.
  • Control and Monitoring: Operation is governed by the Locomotive Control Computer (LCC). Advanced pump designs incorporate features like brushless induction motors to eliminate brush maintenance, and liquid-cooled electronics to prevent heat-related failures.

2.2 Operational Timing and Control Logic

The LCC automates the pump with precise timing to maximize protection while conserving battery power.

  • Activation Triggers: The pump runs during engine starting to pre-lubricate turbocharger bearings before cranking, and after engine shutdown to remove residual heat.
  • Maximum Runtime: The LCC controls the pump motor to run for a maximum of 35 minutes during these phases. This duration is engineered to provide sufficient cooling and lubrication without excessive battery drain.
  • Flow Path: When activated, the pump draws oil from the engine sump, pushes it through the soak back filter, and delivers it directly to the turbocharger before the oil returns to the sump via gravity.

2.3 Technical Specifications and Performance Parameters

Soak back pumps are built to deliver specific performance metrics crucial for protection. Common specifications derived from technical documents and procurement requirements include.

ParameterTypical SpecificationNotes
Flow Rate13 LPM (3.5 GPM)Other sizes (e.g., 3.0 GPM, 6 GPM) are available.
Differential Pressure2.8 bar (40 PSI)Standard working pressure.
Input Voltage74 VDCCommon locomotive DC bus voltage.
Motor Power3/4 HPAlso available in 1/4 HP configurations.
Bypass Valve Setting70 PSIProtects against filter blockage.
Relief Valve Setting32 PSIPrevents over-pressurization.

2.4 Model Variations and Engine Compatibility

Pump specifications vary to match different locomotive engine families and their operational needs.

  • EMD 645 Series: Traditionally use horizontal DC pump assemblies like Part Number 4947308R.
  • EMD 710 Series: Can utilize modern vertical AC pump designs, which are often compatible with both 645 and 710 V-16 engine series.
  • Design Evolution: The shift from horizontal DC to vertical AC designs offers advantages like a smaller footprint (approximately 30 lbs), brushless “maintenance-free” operation, and integrated inverters. Manufacturers design these systems for extended service life, with some rated for up to 10 years of maintenance-free operation in heavy-duty applications.

2.5 System Integration and Protective Function

The pump’s integration into the broader lubrication system provides distinct protective benefits:

  1. Post-Shutdown Cooling: Circulating oil after the engine stops actively removes residual heat from the turbocharger’s bearings and housing, preventing the oil from coking and carbonizing on hot surfaces.
  2. Pre-Start Lubrication: Providing oil pressure to the turbocharger bearings before engine cranking eliminates dry-start conditions, a major source of premature bearing wear.
  3. Operational Reliability: The system offers a layer of redundancy. It ensures continuous oil flow during the transitions when the main engine-driven oil pump is not providing sufficient pressure.
  4. Support for Modern Operations: With features like brushless motors and robust construction, these pumps are specifically designed to withstand the frequent start-stop cycles of locomotives equipped with Automatic Engine Start-Stop (AESS) systems.

In summary, the soak back pump is a precisely controlled, dedicated system that directly combats the primary failure mechanisms of turbochargers in cyclic locomotive operation. Its architecture-from LCC-controlled timing to pressure-regulated filtration-is tailored to extend turbocharger life by ensuring proper lubrication during the engine’s most vulnerable operational phases.

3. Maintenance Best Practices for Soak Back Pump Systems
Maintenance Schedule and Best Practices for Soak Back Pump Systems

A systematic and disciplined maintenance regimen is paramount for the reliability of soak back pump systems and, by extension, the longevity of the turbochargers they protect. Following manufacturer-recommended procedures prevents oil starvation and heat-induced bearing failures, which are leading causes of costly turbocharger replacements. This section outlines a comprehensive maintenance strategy derived from established EMD maintenance instructions and industry practices.

3.1 Scheduled Maintenance Intervals and Operational Integration

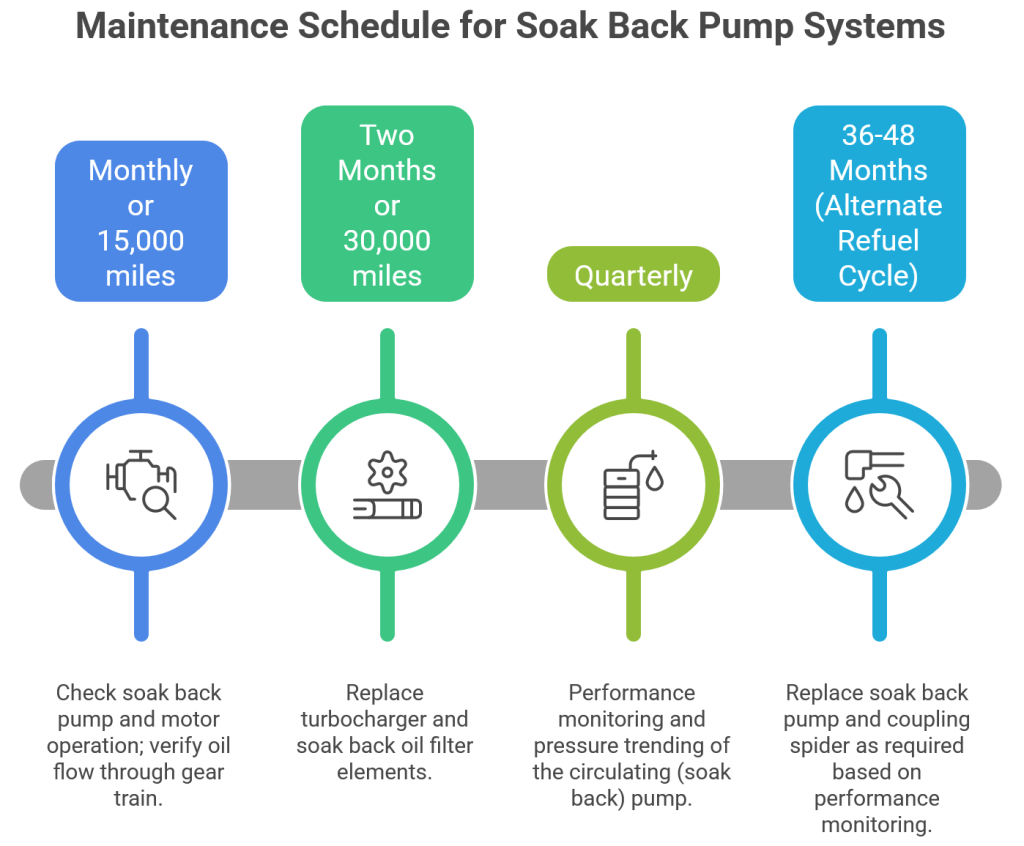
Maintenance of the soak back system is not isolated; it must be synchronized with the engine’s overall lubrication system schedule and the turbocharger’s service cycle. The EMD scheduled maintenance program provides clear, mileage-based intervals that serve as a foundational guide.

IntervalPrimary TasksKey Integration Points
Monthly or 15,000 milesCheck soak back pump and motor operation; verify oil flow through gear train.Acts as a frequent health check, preceding major inspections.
Two Months or 30,000 milesReplace turbocharger and soak back oil filter elements.Aligns with the typical lower bound of turbocharger inspection cycles (30,000-60,000 miles).
QuarterlyPerformance monitoring and pressure trending of the circulating (soak back) pump.Correlates with recommended lube oil analysis frequency.
36-48 Months (Alternate Refuel Cycle)Replace soak back pump and coupling spider as required based on performance monitoring.Integrated into major engine overhaul schedules.

These intervals are influenced by several operational factors that may necessitate more frequent attention: load factor, the type and quality of lubricating oil, operational conditions (e.g., start/stop frequency), climatic conditions, and the maintenance status of the main engine lube oil filters.

3.2 Detailed Maintenance Procedures and Verification

3.2.1 Oil Flow Verification and Operational Check

This is the most critical hands-on procedure to confirm the system is functioning as designed. As detailed in EMD Maintenance Instruction MI-1740, the correct sequence is:

  1. Ensure the engine is completely shut down and all safety protocols, including lockout/tagout, are followed.
  2. Start the soak back pump motor and confirm it is running.
  3. Remove the left rear handhole cover to access the gear train.
  4. Visually check for oil flow through the gear train. The flow should be consistent and steady.
  5. Critical Diagnostic Step: Observe the camshaft bearings. If lubricating oil flows from these bearings while the soak back pump is running and the engine is off, it indicates a potential malfunction. The next action is to inspect the turbocharger filter outlet check valve for proper operation.

3.2.2 Filter System and Protective Valve Maintenance

The soak back filter subsystem incorporates essential pressure-protective valves that require specific checks:

  • 70-PSI Bypass Valve: This valve is housed within the soak back filter assembly. Its purpose is to bypass the filter element entirely if it becomes clogged, ensuring uninterrupted oil flow to the turbocharger and preventing oil starvation. During filter changes, the housing should be inspected for proper valve seating and freedom of movement.
  • 32-PSI Relief Valve: Located in the filter head, this valve’s function is to protect the system from overpressure. If the turbocharger is already receiving oil from the main engine-driven lubrication pump (e.g., during startup before the soak back pump deactivates), this valve opens at 32 PSI to return the soak back pump’s delivered oil directly back to the engine sump.

3.2.3 Motor and Pump Performance Testing

Performance verification ensures the electromechanical heart of the system meets specification. Key parameters to check include:

  • Run-Time: The pump operation is typically controlled by the Locomotive Control Computer (LCC) and runs for a maximum of 35 minutes during engine starting and after shutdown.
  • Output Specifications: Verify the pump delivers its rated flow and pressure. Common specifications for modern pumps are 13 LPM (3.5 GPM) at a differential pressure of 2.8 bar (40 PSI).
  • Electrical & Mechanical: For traditional DC motors (e.g., 74 VDC, 3/4 HP, 1200 RPM), inspect brushes and commutators. For modern brushless induction motors, verify controller operation. In all cases, check for unusual noise, vibration, or signs of overheating.

3.3 Advanced Diagnostics and Proactive Monitoring

Moving beyond scheduled tasks, predictive maintenance techniques can identify degradation before failure.

  • Pressure Trending: Systematically recording the soak back pump’s discharge pressure over time can reveal trends. A gradual pressure drop may indicate pump wear or increasing filter restriction, while erratic pressure could signal valve issues.
  • Oil Analysis Integration: A rigorous lube oil analysis program is strongly recommended and forms the basis for justifying maintenance interval adjustments. Monthly or quarterly analysis of oil samples for wear metals, viscosity, and contamination provides direct insight into the health of the turbocharger bearings and the effectiveness of the filtration system, including the soak back filter.
  • Control System Diagnostics: Utilizing the Locomotive Control Computer (LCC) data logs to verify the soak back pump’s commanded versus actual run times can uncover control or sensor faults.

3.4 Maintenance Checklist for Field Technicians

A concise, actionable checklist ensures no critical step is missed during service:

Pre-Work & Safety

  •  Engine shut down, isolated, and locked out/tagged out.
  •  Turbocharger confirmed cool enough to touch.

Visual & Physical Inspection

  •  Inspect pump, motor, and lines for leaks, corrosion, or damage.
  •  Check electrical connections for security and integrity.
  •  Verify all mounting hardware is tight.

Operational Verification

  •  Start soak back pump motor; confirm smooth, quiet operation.
  •  Remove specified handhole cover; verify oil flow through gear train.
  •  Check for oil at camshaft bearings (diagnostic indicator).
  •  Record pump discharge pressure (if gauge is available).

Filter System Service (at scheduled interval)

  •  Replace soak back filter element with OEM-quality part.
  •  Clean filter housing; inspect for debris.
  •  Visually inspect bypass and relief valve components.

Documentation & Follow-Up

  •  Record all findings, measurements, and corrective actions.
  •  Update unit maintenance history.
  •  Determine next service date based on findings and interval guidelines.

3.5 Critical Failure Prevention Insights

Analysis of maintenance data highlights key intervention points:

  • Strict Filter Change Adherence: Adhering to the 2-3 month (30,000-mile) filter replacement interval is crucial. Extending beyond this risks filter structural integrity and increases the chance of the bypass valve activating due to clogging, which can allow unfiltered oil to reach the turbocharger.
  • Heeding Diagnostic Clues: The procedure noting oil flow from camshaft bearings during a soak back pump test is a specific diagnostic for a failed check valve. Promptly investigating this can prevent a situation where the soak back pump cannot build sufficient pressure to lubricate the turbocharger.
  • Understanding System Interaction: Recognizing that the 32-PSI relief valve is designed to work in concert with the main engine oil pressure prevents misdiagnosis of “low” soak back pressure during engine cranking, when both systems are active.

By implementing these detailed, fact-based maintenance practices, operators can transform the soak back pump from a simple auxiliary component into a cornerstone of a proactive reliability strategy, directly safeguarding turbocharger investment and operational availability.

4. Performance Benefits and Cost Savings Analysis
Performance Benefits and Cost Savings Analysis

The primary value proposition of a properly maintained soak back pump system is not merely theoretical-it translates directly into measurable, quantifiable benefits for fleet operators. By addressing the root causes of premature turbocharger failure, these systems deliver substantial improvements in component longevity, reductions in maintenance expenditure, and enhanced operational reliability.

4.1 Extending Turbocharger Service Life Through Improved Lubrication

The most direct benefit is the extension of turbocharger bearing life. The system’s core function-maintaining oil flow after the main engine-driven pump stops-directly combats oil coking and starvation during the critical post-shutdown heat soak phase. Research into specialized lubrication systems, such as those incorporating hydraulic accumulators, has demonstrated that maintaining stable oil supply can improve turbocharger rotor run-out time after shutdown by 30-40%. One study focusing on individual lubrication systems showed they could double the rotor inertia duration compared to a standard engine lubrication circuit, indicating a potential halving of bearing wear rates. This data underscores the principle that extended, controlled post-shutdown lubrication directly correlates with reduced mechanical wear on high-speed bearings.

Impact of Soak Back Operation on Lubrication Duration:

Engine ConditionStandard Lubrication SystemWith Functional Soak Back SystemApproximate Improvement
Post-ShutdownOil flow ceases immediatelyOil flow continues for up to 35 minutesPrevents dry spinning & coking
Pre-StartBearings are dry until engine oil pressure buildsBearings are pre-lubricated before crankingEliminates dry-start wear

4.2 Reducing Maintenance Costs and Downtime

The financial impact of avoiding turbocharger failures is significant. A single failure event necessitates not only the high cost of the turbocharger assembly itself but also associated labor, potential engine oil contamination, and, most critically, unscheduled locomotive downtime. Soak back pumps mitigate this risk proactively. Modern units are engineered for durability, with some designs boasting a maintenance-free service life of up to 10 years on heavy-duty equipment, eliminating the cost and downtime of regular brush replacements common in older DC motor designs.

Integrating soak back pump checks into the scheduled maintenance program is a low-effort, high-return activity. For instance, verifying operation by checking oil flow through the gear train with the engine off is a straightforward procedure that can prevent catastrophic failure. Furthermore, the system includes built-in protective features; a clogged soak back filter will bypass via a 70-PSI valve, and a 32-PSI relief valve prevents over-pressure, ensuring the turbocharger remains protected even during a filter maintenance lapse.

Comparative Maintenance Regimen:

TaskWithout Soak Back System FocusWith Soak Back System Focus
Turbocharger LongevityReliant on perfect main engine shutdown cooldown (often manual)Protected by automated post-lubrication and cooling
Bearing Failure RiskHigher risk of coking and starvation after shutdownSignificantly reduced risk due to controlled oil flow
System MaintenanceN/AQuarterly operational checks and filter changes at 30,000-60,000 mile intervals

4.3 Supporting Operational Efficiency and Modern Engine Cycles

Beyond failure prevention, soak back pumps enable more efficient locomotive operation, particularly in modern applications. They are specifically designed for compatibility with Automatic Engine Start-Stop (AESS) systems, which subject the turbocharger to frequent thermal cycles. In these demanding cycles, the soak back pump’s dual role is essential: it pre-lubricates bearings before a start and removes residual heat after a stop, making frequent start-stop operation viable without sacrificing turbocharger life.

The system’s automated operation, controlled by the Locomotive Control Computer (LCC) for a prescribed period (up to 35 minutes), also eliminates the need for manual engine idling to cool down the turbocharger, leading to direct fuel savings and reduced engine wear.

4.4 Return on Investment Considerations

The return on investment for ensuring a functional soak back pump system is compelling when viewed through the lens of total cost of ownership. The cost of a pump and its routine maintenance filters is minor compared to the expense of a turbocharger overhaul or replacement and the associated locomotive out-of-service time. The investment protects a critical, high-value component. Implementing a rigorous oil analysis program, as recommended by maintenance guides, further enhances this ROI by providing trend data on wear metals, allowing for predictive maintenance and justifying potential extensions of service intervals based on actual oil condition.

In summary, the soak back pump is a quintessential example of a modest, targeted engineering solution that delivers disproportionate economic benefits. By ensuring continuous lubrication during the turbocharger’s most vulnerable operational phases-immediately after shutdown and just before startup-it directly extends component life, reduces the frequency and severity of maintenance events, and supports the reliable, efficient operation demanded in modern locomotive service.

5. Advanced Monitoring and Diagnostic Integration
Advanced Monitoring and Diagnostic Integration

The evolution from reactive to predictive maintenance has made advanced monitoring and diagnostic integration a cornerstone of modern locomotive upkeep. For turbocharger longevity, integrating the soak back pump with sophisticated condition monitoring technologies transforms it from a simple protective device into an intelligent subsystem that provides actionable insights into bearing health and thermal management.

5.1 Integrated Control System Architecture

The foundation of this integration is the Locomotive Control Computer (LCC), which serves as the central nervous system for the soak back pump. Technical documentation confirms the LCC automatically controls the pump motor, running it for a maximum of 35 minutes during engine starting and after shutdown. This precise control is critical, as it ensures oil flow for residual heat removal during the most vulnerable post-shutdown period and provides pre-lubrication before cranking. The LCC’s integration enables the collection of operational data—such as pump activation status and run-time duration-which can be trended to detect deviations indicative of motor issues or control system faults.

5.2 Comprehensive Oil Analysis Programs

A disciplined oil analysis program is arguably the most critical predictive tool for the soak back and turbocharger lubrication circuit. The condition of the oil directly reflects the health of the components it lubricates. For these systems, a robust program should implement several key tests, drawing on established condition monitoring practices.

Essential Oil Analysis Tests:

  • Viscosity Monitoring: Tracks oil thickness. Significant deviation can signal degradation or contamination, affecting the pump’s ability to maintain proper flow and pressure.
  • Elemental Spectroscopy (ICP): Monitors wear metals like iron (bearings), copper (bushings), and aluminum (compressor wheel). Trending these elements helps identify abnormal wear patterns in the turbocharger long before failure.
  • Fourier-Transform Infrared (FTIR) Spectroscopy: Detects chemical changes such as oxidation (from high turbo temperatures), nitration, and additive depletion, which compromise the oil’s protective qualities.
  • Particle Counting: Measures contamination levels. High particulate counts can lead to premature clogging of the soak back filter, potentially activating its 70-PSI bypass valve and allowing unfiltered oil to reach the turbo bearings.

Industry guidance strongly recommends oil analysis as the basis for extending maintenance intervals, with a minimum of quarterly analysis and a preferred frequency of monthly or after every loaded engine run. Implementing such a program allows maintenance teams to spot early signs of wear and contamination, addressing issues proactively to prevent costly turbocharger failures.

5.3 Vibration Analysis and Infrared Thermography

Vibration analysis and infrared thermography provide complementary, non-invasive insights into the mechanical and thermal state of the soak back pump and turbocharger.

Vibration Analysis is particularly effective for detecting mechanical faults such as bearing defects, imbalance, or misalignment in rotating components. For the soak back pump motor and the turbocharger itself, establishing a baseline vibration signature and monitoring for changes can reveal developing issues. For instance, specific fault frequencies can indicate deteriorating pump motor bearings before they affect performance.

Infrared Thermography detects radiation energy and converts it to a temperature display, making it ideal for identifying thermal anomalies. Key applications for the soak back system include:

  • Verifying the turbocharger housing is cooling adequately during the pump’s post-shutdown cycle.
  • Detecting localized overheating on the soak back pump motor, which could indicate electrical problems or excessive mechanical friction.
  • Identifying hot spots or unusual temperature gradients in oil lines, which might suggest flow restrictions or blockages.

The correlation between these technologies is powerful. A bearing issue might show increased iron particles in the oil analysis, specific fault frequencies in the vibration spectrum, and an elevated temperature at the bearing housing in a thermographic survey. This multi-faceted view enables more accurate diagnosis and timely intervention.

5.4 Predictive Maintenance Integration

Modern predictive maintenance integrates data streams from the LCC, oil analysis, vibration sensors, and thermography into a cohesive monitoring platform. The goal is to shift from fixed-time maintenance to condition-based interventions.

Implementation Strategy:

  1. Data Collection: Utilize the LCC to log soak back pump run times and correlate them with engine shutdown events and turbo temperature sensor data.
  2. Trend Analysis: Systematically trend oil analysis results (wear metals, viscosity) and vibration data to establish normal baselines and identify drift.
  3. Threshold Alerts: Set automated alerts for key parameters, such as a rise in specific wear metals or a deviation in pump motor run-time.
  4. Proactive Scheduling: Use these insights to schedule filter changes (for the soak back and turbocharger oil filters) or pump inspections based on actual condition, potentially optimizing the typical 30,000–60,000-mile inspection window.

This integrated, data-driven approach transforms the soak back pump from a standalone component into a diagnostic node within a broader health monitoring network, directly contributing to extended turbocharger life and reduced unplanned downtime.

6. Future Developments and Optimization Strategies
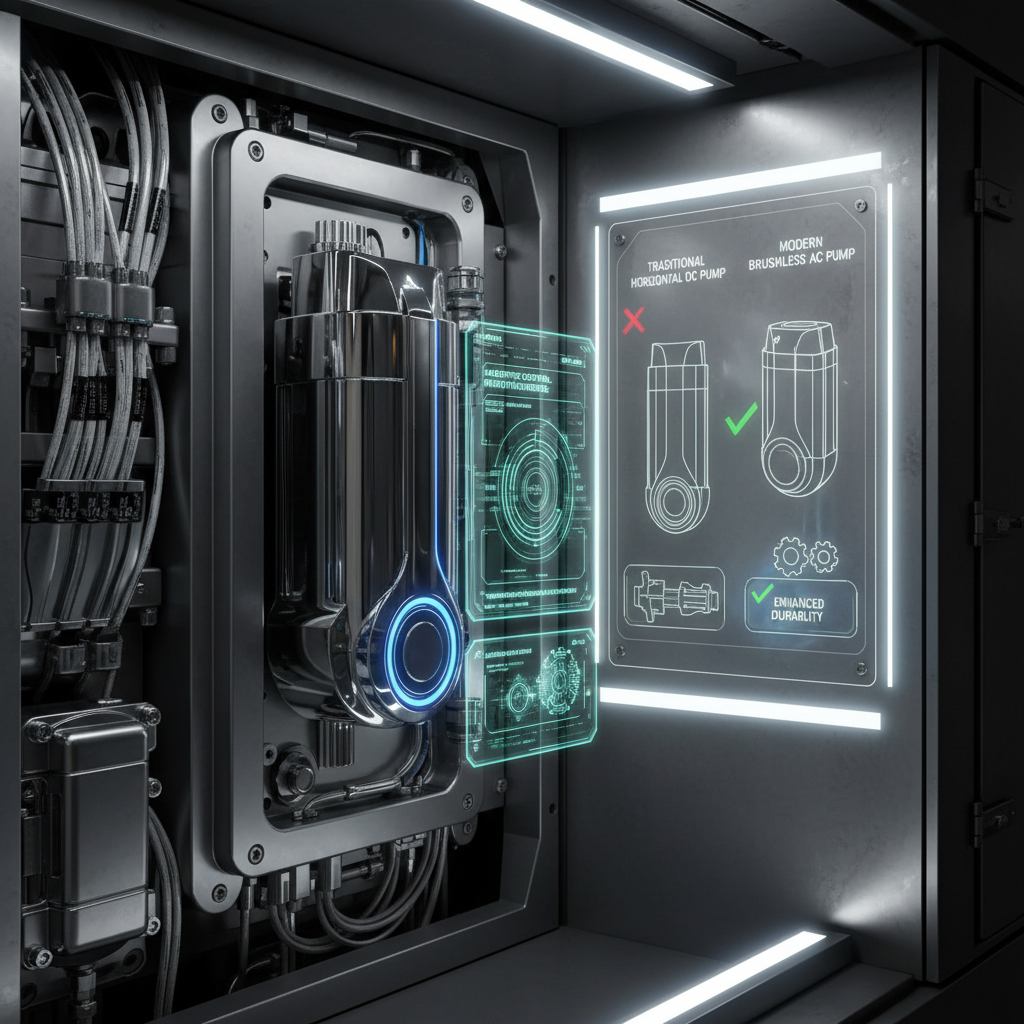
Future Developments and Optimization Strategies

The evolution of soak back pump technology is driven by demands for greater operational efficiency, extended component life, and seamless integration with modern locomotive control systems. Emerging designs and intelligent control strategies are reshaping how turbochargers are protected during critical post-shutdown and pre-start phases.

6.1 Advanced Pump Design Architectures

A significant trend is the shift from traditional horizontal DC motor configurations to advanced vertical AC models with integrated inverters. These newer designs offer marked improvements in reliability, maintenance requirements, and application flexibility.

Comparison of Traditional vs. Modern Soak Back Pump Designs:

FeatureTraditional DC Horizontal PumpModern AC Vertical Pump
Motor TypeDC motor (e.g., 74 VDC)Brushless AC motor with built-in inverter
Power & Speed3/4 HP at 1200 RPM3/4 HP at 1200 RPM
Flow Rate3-6 GPM3-7 GPM
Working Pressure40 PSI minimum40 PSI minimum
Mounting & WeightHorizontal, heavierVertical, ~30 lbs
Engine Compatibility645 Engine series645 and 710 Engine series (V-16)
Durability ClaimStandard intervalsEnhanced durability up to 6 years
Cooling MethodConventionalSelf-cooling using diesel as a medium

The advantages of the vertical AC design are substantial. Brushless induction motors eliminate the need for brush replacement, directly reducing maintenance costs and downtime. The integrated inverter and protective circuitry enhance reliability in environments prone to voltage fluctuations. Furthermore, the compact, vertical footprint simplifies installation in crowded engine rooms.

6.2 Integration with Automatic Engine Start/Stop (AESS) Systems

The proliferation of Automatic Engine Start/Stop systems, which shut down the main engine during prolonged idling to save fuel, creates a unique challenge. Soak back pumps must now be engineered for dramatically increased start/stop cycles without performance loss.

Key Design Features for AESS Compatibility:

  • Robust Cycling: Components must endure hundreds of additional annual cycles.
  • Intelligent Control: Seamless integration with the Locomotive Control Computer (LCC) is essential for coordinating pre-lubrication before an automatic restart.
  • Thermal Management: Liquid-cooled electronics are critical to prevent heat-related failures during potentially extended pump run times.
  • Longevity: Pumps are being designed for maintenance-free lives of up to 10 years in heavy-duty service to match extended maintenance intervals.

6.3 Optimization Through Adaptive Control and Monitoring

Future systems are moving beyond simple timers toward adaptive control based on real-time conditions. The standard 35-minute maximum runtime, as controlled by the LCC, may be optimized dynamically.

Potential Adaptive Control Strategies:

Control ParameterFixed ApproachAdaptive Optimization
Run TimeFixed duration (e.g., 35 min)Variable based on measured turbocharger temperature decay.
Activation TriggerEngine-off signalTemperature-based activation threshold.
System IntegrationStandalone operationCoordinated with engine cooling and lube oil systems.
Health MonitoringPeriodic manual checksContinuous pressure and vibration trending for predictive maintenance.

This shift enables condition-based maintenance. For instance, performance monitoring of pump pressures can indicate developing blockages in the turbocharger oil passages. Regular lube oil analysis, a cornerstone of comprehensive maintenance programs, provides essential data on wear metals and oil condition, informing decisions about pump and filter service.

6.4 Focus on Reliability and Service Life

The overarching goal of these developments is to create a “fit and forget” component with exceptional reliability. Key design features contributing to this goal include:

  • Hardened pump bodies and gears to maximize longevity under continuous or frequent cycling.
  • Continuously lubricated, self-cleaning bearings for consistent performance over the pump’s lifespan.
  • Standardized capacities and pressures (e.g., 13 LPM / 3.5 GPM at 40 PSI) that meet core protection requirements while allowing for customization in size and voltage as needed.

The trajectory of soak back pump development is clear: integration of more durable materials, intelligent and connected control systems, and designs tailored for the specific demands of modern, efficiency-focused locomotive operations. This evolution ensures that the soak back pump will continue to be a critical, yet increasingly reliable, guardian of turbocharger longevity.
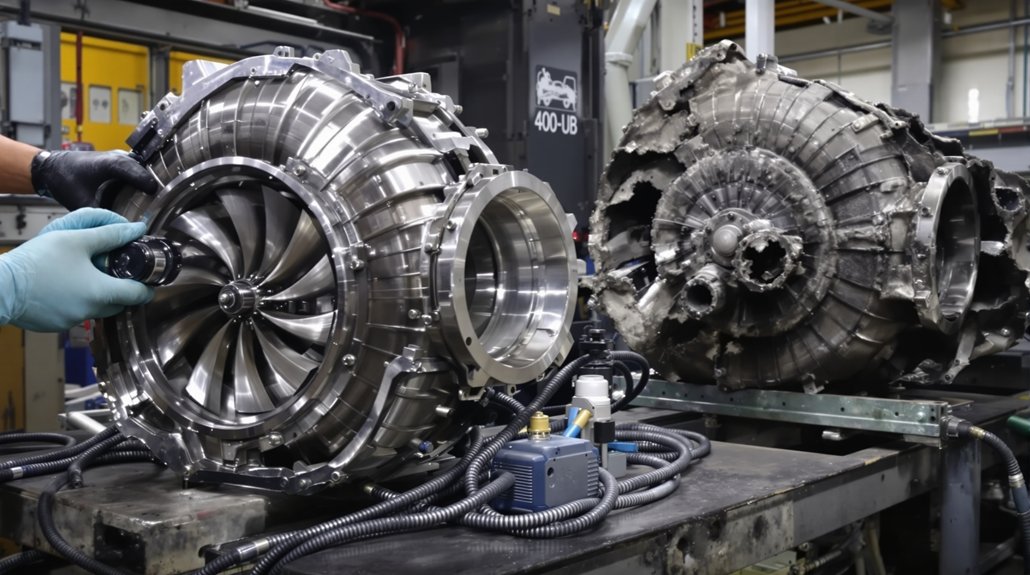
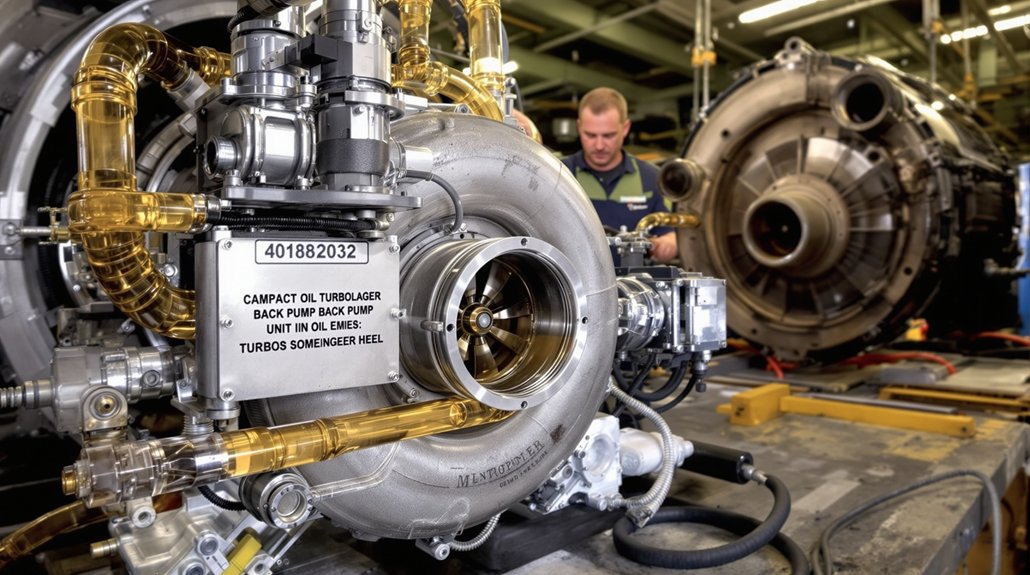
How Does Turbo Soak Back Pump 40182032 Prevent Oil Coking in Locomotive Turbochargers?

How Does Turbo Soak Back Pump 40182032 Prevent Oil Coking in Locomotive Turbochargers?

When a locomotive shuts down after a hard pull, the turbocharger is still extremely hot-but the oil flow that was keeping it cool stops almost instantly.

That’s when oil starts to overheat, oxidize, and coke on hot bearing and seal surfaces. Over time, this silent damage shortens turbo life, drives unplanned outages, and inflates overhaul costs.

Key pain points Turbo Soak Back Pump 40182032 is designed to address in locomotive turbochargers:

  • Oil coking in the turbo center housing during hot soak after shutdown
  • Varnish and hard carbon deposits on bearings and seal rings
  • Sticking or dragging bearings leading to slow spool-up and power loss
  • Increased turbo failures between scheduled overhauls
  • Higher lube oil contamination and filter loading from coke debris
  • Extended locomotive downtime due to turbo change-outs and inspections
  • Unpredictable performance on hot days or after heavy load cycles
  • Difficulty meeting OEM-recommended turbocharger life targets
  • Rising lifecycle cost per turbocharger over the locomotive’s service life

How Pump 40182032 Helps You Overcome These Issues

Problem / SymptomRoot Cause During Hot SoakWhat Pump 40182032 DoesOperational Benefit for the Locomotive
Bearing oil coking after shutdownStagnant oil exposed to residual turbo heatMaintains controlled oil circulation post-shutdownPrevents coke formation on bearing surfaces
Varnish and deposits in turbo coreLocalized overheating of trapped oilKeeps oil moving to remove heat from coreCleaner internals and smoother bearing operation
Frequent turbo overhauls or replacementsProgressive deposit buildup and bearing distressReduces thermal stress on oil and componentsLonger intervals between turbo overhauls
Slow turbo response, reduced powerDeposits increasing friction and dragProtects bearing clearances and surface finishFaster spool-up, more consistent horsepower
Oil filter plugging, dirty crankcase oilCoke particles flushed into engine lube systemMinimizes coke generation at the turbo sourceLower contamination load on engine oil system

Like a slow bake in a hot engine compartment, a locomotive turbo’s hot soak after shutdown is exactly when oil coking quietly starts.

If you’re not controlling oil flow and pressure across those hot-side bearings, you’re inviting varnish, hard coke, and accelerated wear.

Pump 40182032 attacks this problem by keeping oil moving, pressurized, and cooling through the turbo core-but how it does that, and what it means for your overhaul intervals, is where it gets interesting.

How Oil Coking Damages Locomotive Turbochargers

oil coked turbocharger bearing failure

Although modern locomotive turbochargers are designed for extreme duty, oil coking remains one of the most destructive failure modes because it directly attacks the bearing system at its hottest point. At turbine-end metal temperatures of 450-650°C, any residual oil that’s not actively circulating oxidizes rapidly and polymerizes into varnish, then hard carbonized coke. You see the first effects as subtle journal scoring and darkened oil films in the bearing housing.

As deposits build, they narrow feed and drain passages, so even with “normal” system pressure you’re running localized starvation at shaft speeds up to ~300,000 rpm. The bearing oil film collapses, metal-to-metal contact increases, and you move quickly from elevated vibration to full bearing seizure. Coke particles themselves act as abrasives, further eroding journals and thrust faces. With each thermal cycle and each hour on aged or contaminated oil, coke thickness grows, accelerating imbalance, shaft runout, and ultimately catastrophic turbocharger failure.

Shutdown and Soak-Back: When Coking Hits Hardest

turbo soak back coking cycle

Once you shut the engine down after a high-load run, the turbocharger instantly loses pressurized oil flow while turbine-end metal temperatures often remain in the 450–650°C range, creating the most coking-prone moment in the duty cycle. You’ve entered the hot soak phase: bearings sit surrounded by residual oil that can’t escape and can’t cool. With no cooldown flow, that trapped oil dwells at extreme temperature, oxidizes, and solidifies into coke.

During repeated stop/start operation, this thermal pulse becomes a cumulative failure driver. Each shutdown bakes a thin layer of oil into varnish and carbon, progressively:

  • Narrowing feed and return passages
  • Distorting hydrodynamic film thickness at the shaft
  • Raising startup friction and wear

In locomotive service, long high-load pulls followed by shutdown maximize soak-back heat. If you don’t manage that interval, you effectively turn every stop into a controlled coking cycle inside the turbocharger.

How Turbo Soak Back Pump 40182032 Prevents Oil Coking

continuous post shutdown oil circulation

In practical terms, Turbo Soak Back Pump 40182032 breaks the coking cycle by keeping oil moving through the turbocharger exactly when it would otherwise sit and burn. After shutdown, it continues to circulate engine oil across the hot-side bearings and oil passages, evacuating heat from the turbine housing and preventing stagnant oil pockets where thermal breakdown accelerates.

You maintain controlled post‑shutdown oil pressure, so bearing surfaces stay fully wetted and protected. Peak oil film temperature drops, slowing oxidation, varnish, and hard coke formation. That directly reduces abrasive deposits on the high‑speed shaft and avoids oil‑starvation events that cascade into bearing failure.

Because the unit’s brushless drive and liquid‑cooled electronics are designed for frequent start/stop operation, you get consistent soak‑back performance over long service intervals. Integrated pre‑lube capability builds an oil film before crank‑over, minimizing dry‑start wear. With proper coolant interaction management and scheduled electrical diagnostics, you keep this anti‑coking control loop stable and predictable.

Inside Pump 40182032: Design That Protects Your Turbo

turbo protecting liquid cooled postshutdown pump

Built around a brushless-induction, liquid‑cooled DC drive, Pump 40182032 is engineered as a dedicated post‑shutdown oil mover that protects your turbocharger when thermal stress is highest. You get a controlled 13 LPM (3.5 GPM) at 2.8 bar (40 PSI), keeping turbo bearings under positive pressure while the housing heat‑soaks. Integrated cooling channels in the pump housing and electronics pull heat away from the drive, preventing thermal drift and extending component life under repeated shutdown cycles.

Internally, hardened gear materials and a reinforced pump body resist scoring from contaminated oil and high differential pressures. Continuously lubricated, self‑cleaning bearings maintain alignment, so you hold flow and pressure without constant adjustments or rebuilds. The same architecture doubles as a pre‑lube system, restoring oil to the turbo before shaft speed rises.

  • Maintain predictable cooldown oil pressure every shutdown
  • Minimize internal wear over 10‑year heavy‑duty duty cycles
  • Reduce unplanned turbo and pump maintenance interventions

Installing and Operating the Turbo Soak Back Pump Safely

precise turbo oil electrical integration

Although Pump 40182032 is designed for unattended reliability, safe installation and operation depend on how precisely you integrate it into the turbo oil and electrical systems. Mount the pump in the turbo oil return or sump feed line exactly per the routing schematic, and confirm the part number and rating: 13 LPM (3.5 GPM) at 2.8 bar (40 PSI) for the 74 VDC AESS model. Any oil pan modifications must use OEM sealing, torque, and cleanliness controls.

Treat electrical routing as a reliability variable: use the specified 74 VDC input, segregate harnesses from exhaust and hot manifolds, and secure all terminations to withstand vibration and contamination.

Validate coolant plumbing to the electronics section for leak-free liquid cooling, then confirm motor orientation and access clearances. Program post-shutdown and pre-lube run times, and verify approximately 13 LPM at 2.8 bar during tests. Finally, implement periodic inspections of lines, fittings, and housing for wear and contamination.

Turbocharger Reliability, Maintenance Savings, and ROI With Pump 40182032

preventive turbocharger oil flush

Drive turbocharger reliability higher by attacking one of its primary failure modes: oil coking during hot soak. By keeping oil circulating at roughly 3.5 GPM and ~40 PSI after shutdown, Pump 40182032 flushes hot-side passages, limits varnish and carbon, and protects shaft and bearing surfaces. You cut unplanned turbo replacements, stabilize fuel efficiency by preserving turbo performance, and reduce warranty implications from coked, oil-starved failures.

  • Extend turbocharger service life and overhaul intervals by minimizing coke-driven bearing and shaft damage.
  • Reduce labor and parts costs tied to turbo swaps, oil-line cleaning, and repeat post-failure inspections.
  • Protect assets in frequent start/stop AESS duty cycles where hot-soak events multiply.

The brushless induction motor, liquid-cooled electronics, and hardened internals target a maintenance-free life approaching 10 years. That durability turns a one-time capital outlay into predictable ROI, anchored in avoided turbo failures, fewer warranty disputes, and higher locomotive availability.

Frequently Asked Questions

How to Prevent Turbo Coking?

You prevent turbo coking by controlling heat and oil chemistry. Since deposits can cut bearing life by over 50%, you must manage idle heating: after high load, idle a few minutes so metal temps drop below coke-forming ranges. Use strict additive selection—high-oxidation-stability synthetic oils, boosted detergents, and dispersants. Maintain clean feed/return lines, enforce short oil-change intervals under severe duty, and verify post-shutdown oil circulation performance.

How Do Scavenge Pumps Work?

You use scavenge pumps to pull hot oil away from bearings and return it to the dry sump before it degrades. A rotary scavenge stage runs under slight vacuum at the turbo outlet, rapidly evacuating oil and entrained air. You size the pump for several L/min flow so residual volume stays low. This controlled extraction reduces dwell time, prevents coking, and stabilizes bearing temperatures and oil film thickness.

What Causes Oil in a Turbocharger?

You get oil in a turbocharger because the engine’s pressurized lube circuit feeds the turbo bearings for cooling and friction control. At turbine-side temperatures approaching 650°C, you’re fighting thermal degradation and oil contamination from oxidized films and fine wear metals. Any seal wear, housing distortion, or drain restriction lets that oil leak into the compressor or turbine housings, where it burns, forms deposits, and undermines long-term reliability.

Does a Turbo Pump Its Own Oil?

No, a turbo doesn’t pump its own oil; you rely on the engine’s lube system for shaft lubrication and cooling. The engine oil pump provides pressure regulation and flow through the turbo’s feed gallery, then oil drains back to the sump by gravity. When the engine stops, circulation ceases, so you must manage shutdown and auxiliary systems carefully to avoid stagnant hot oil, varnish, and bearing damage.

Locomotive Lube Oil Soakback Pump – OEM Engine Part 40182032 – Diesel/EMD

Locomotive Lube Oil Soakback Pump - OEM Engine Part 40182032 - Diesel/EMD

What are the exact specifications of locomotive turbo soak back pump part number 40182032? Most buyers struggle to verify OEM fit, fluid capacity, and compatibility across EMD diesel models. They also worry about delivery timelines and reliable supply. Here is what you need now:

Before proceeding, make sure you have verified the following details:

  1. Confirm the part is OEM 40182032.
  2. Ensure it includes the full soakback function.

Match your locomotive model and turbo configuration. To ensure proper compatibility, consider the following:

  1. Confirm the specific locomotive model you are working with.
  2. Verify the turbocharger configuration required for that model.
  3. Check rotor, shaft, and vertical mounting dimensions.
  4. Verify lube oil flow rate and pressure range.
  5. Ensure filter element compatibility and micron rating.
  6. Confirm AC electric drive or mechanical drive interface.
  7. Ask for replacement assy and service kit availability.

Please review the following steps to validate worldwide shipping and lead time:

  1. Confirm that worldwide shipping is available for the destination.
  2. Check the estimated lead time for delivery.
  3. Request testing data and product description sheet.
  4. Ensure GE and ALCO cross references if needed.

Overview of the Locomotive Lube Oil Soakback Pump

Overview of the Locomotive Lube Oil Soakback Pump

This OEM pump, part number 40182032, is an EMD diesel engine component designed for turbo soakback duty. It circulates lube oil after shutdown to protect bearings and the rotor assembly. The pump prevents coking in the turbo and stabilizes fluid temperature. It reduces wear on the shaft and extends engine parts life. This product suits railway locomotive operations that demand reliable start-stop cycles. It is a precise replacement assy with proven performance and global support.

What is the Lube Oil Soakback Pump?

The lube oil soakback pump is a dedicated component that maintains oil flow to the turbo and related bearings after engine shutdown. It keeps fluid moving to dissipate heat, preventing oil degradation. The pump can be vertical or horizontal type depending on model. It integrates with filter element housings and check valves. In many diesel engine setups, it uses an electric AC motor drive. Its purpose is to protect the turbo rotor and shaft in high-temperature conditions.

Importance of Part Number 40182032

Part 40182032 identifies a specific OEM soakback pump used on select EMD diesel locomotive engines. The exact number ensures dimensional fit, correct flow, and compatible seals. Using the wrong pump risks poor soakback performance, turbo damage, and oil aeration. This product code also aligns with approved replacement assy standards. It helps maintenance teams order, stock, and supply the right component. Mikura International can provide the correct description, testing data, and global delivery for this part.

Applications in Locomotive Engines

The pump serves EMD diesel locomotive platforms that require turbo soakback protection. It is used in railway locomotive fleets with heavy duty cycles, frequent shutdowns, and high exhaust heat. Many operators pair it with OEM filter elements to keep lube oil clean. The component is compatible with select GE and ALCO rail equipment when cross-referenced. Typical use involves a vertical mount near the turbo oil gallery. Mikura International can offer worldwide shipping and ensure reliable supply for maintenance programs.

Key Specifications of the Pump

The OEM soakback pump, part 40182032, delivers defined performance for EMD diesel engines. Buyers need a clear description of flow, pressure, and vertical mounting. The component must match the turbo gallery, shaft interface, and filter element path. Its purpose is stable lube oil circulation post-shutdown. The product is a direct replacement assy, compatible with select locomotive models. Mikura International can provide testing data, global shipping, and reliable supply. We offer accurate delivery windows and worldwide support for railway locomotive fleets. The pump is engineered for AC electric duty and consistent soakback performance.

Technical Specifications

This OEM pump is engineered for EMD diesel engine soakback service. Typical flow ranges between 6–12 L/min depending on model and oil viscosity. Nominal discharge pressure is set for turbo bearing galleries. The AC electric motor is rated for continuous post-shutdown cycles. The vertical shaft and rotor are balanced to reduce vibration. Inlet and outlet ports align with standard locomotive parts interfaces. The component supports clean lube oil via an upstream filter element. Electrical enclosure meets railway duty standards. Replacement assy kits are available for seals and wear components.

Design Features of the OEM Part

The 40182032 part integrates a robust rotor, precision shaft, and tight clearances for reliable fluid control. Its vertical configuration minimizes footprint near the turbo oil return. The component uses high-temperature seals compatible with diesel lube oil. Passage geometry reduces aeration and maintains steady flow. Housing features allow easy alignment with OEM rail equipment. The pump’s check valve provision supports soakback purpose after shutdown. An electric AC drive enables consistent starts and stops. The design accepts upstream filter elements for clean operation. The product remains compatible with approved EMD locomotive parts.

Type: AC Vertical Configuration

This pump is an AC vertical type, built for compact mounting on EMD diesel engines. The vertical arrangement supports gravity-aided priming and reduced cavitation. The electric motor provides stable torque for controlled soakback flow. The configuration aligns with turbo gallery heights on many locomotive models. Wiring routes cleanly along the engine frame in railway applications. The component’s vertical shaft simplifies service on the rotor and seals. It is a direct replacement assy for OEM 40182032. Mikura International can supply the correct AC specification and provide timely delivery worldwide.

Functionality and Purpose

Functionality and Purpose

The soakback pump, part 40182032, serves one critical purpose in an EMD diesel engine: keep lube oil circulating after shutdown. This protects the turbo rotor, shaft, and bearings from heat soak damage. The component sustains fluid flow to prevent coking and oil breakdown. It integrates with OEM locomotive parts and rail equipment without modification. The product’s electric AC drive ensures predictable performance. Proper description, correct type, and compatible fittings matter. Reliable supply and delivery enable fleets to standardize the replacement assy across railway locomotive models.

How the Soakback Pump Works

After engine stop, residual heat rises into the turbo and galleries. The OEM pump activates on a timed or temperature signal and pushes lube oil through the turbo bearing circuit. The flow removes heat, stabilizes viscosity, and prevents varnish. A vertical AC electric motor drives the rotor and shaft for steady discharge. Check valves retain column prime to reduce aeration. An upstream filter element keeps contaminants out of the component. The diesel engine cools predictably, reducing restart wear. This process preserves engine parts and extends overhaul intervals.

Benefits of Using OEM Parts

Using the OEM 40182032 part ensures exact fit, verified flow, and seal compatibility in EMD diesel platforms. The component aligns with locomotive interfaces, preventing misalignment and leaks. OEM specification protects the turbo and shaft under real railway duty. Certified materials resist high temperature lube oil. Documentation provides a clear description for maintenance teams. Replacement assy kits match the original tolerances. Consistent performance avoids underflow during soakback. Mikura International can provide tested OEM supply, so fleets get global shipping, correct model matching, and dependable delivery windows.

Common Issues and Solutions

Low flow often traces to a clogged filter element or incorrect oil viscosity. Restore with an OEM filter and seasonal viscosity review. Noisy operation may indicate rotor wear or cavitation from poor priming; verify vertical mount, inlet head, and check valve integrity. Leakage at the shaft points to hardened seals; install an OEM seal kit. Overheating turbo after shutdown suggests wrong pump type or timing; correct the control setting. Erratic current draw indicates electric motor faults; test insulation. Always confirm the part description matches 40182032 before replacement.

Maintenance and Care for the Pump

Maintenance and Care for the Pump

Proactive maintenance preserves soakback function and protects the turbo. Set inspection intervals to match diesel duty cycles and ambient heat. Verify OEM flow using a calibrated gauge at the turbo gallery. Replace the filter on hours or differential pressure. Check wiring and connectors on the AC electric drive. Inspect the vertical mount, fittings, and hoses for weep. Review oil cleanliness and element micron rating. Keep a replacement assy in stock to limit downtime. Standardize on the same 40182032 part across compatible locomotive models for uniform results.

Regular Maintenance Practices

Start with a clean lube oil baseline and approved viscosity. Inspect the component at scheduled hours for housing cracks, shaft leaks, and rotor noise. Replace the filter element before bypass. Verify electrical continuity, insulation, and grounding of the AC motor. Confirm check valve sealing to maintain prime in vertical installations. Flush lines if debris is found during element changes. Record actual flow and pressure against OEM description. Update control logic for soakback duration by season. Keep a log of delivery and service dates to align with railway reliability targets.

Signs of Wear and Tear

Watch for longer cooldown times and elevated turbo skin temperatures. Listen for new whine or vibration indicating rotor or bearing wear. Look for sheen or puddles near the shaft seal. Track reduced flow to the turbo gallery at the same current draw. Monitor lube oil discoloration after shutdown cycles. Check for intermittent starts from electric faults. Note recurring air in the fluid line, a sign of poor prime or fitting leaks. Any mismatch with OEM 40182032 performance benchmarks signals imminent failure and calls for a planned replacement.

Replacement Tips for Longevity

Cross-check the part number 40182032 and the complete description before ordering. Match fittings, voltage, and AC frequency to the locomotive model. Replace seals, gaskets, and the filter element together to stabilize baseline conditions. Align the vertical mount to prevent shaft side-loading. Purge air and prefill lines to protect the rotor at first start. Verify control settings for soakback duration by ambient temperature. Keep a spare replacement assy in inventory for critical routes. Mikura International can offer worldwide shipping and provide OEM kits, ensuring fast, reliable global supply.

Comparing Different Engine Pumps

Selecting the correct pump for an EMD diesel engine demands rigorous comparison across functions and duty cycles. A clear description of soakback capability, lube oil handling, and AC electric type is essential. Evaluate rotor geometry, shaft support, and vertical mounting allowances. Confirm compatibility with your locomotive model and related rail equipment. Review filter element paths and micron rating. Analyze global supply reliability and delivery terms. Ensure the product meets OEM tolerances for 40182032. Compare worldwide shipping options and service coverage. Document cross references for GE and ALCO when required.

Comparison of Diesel vs. EMD Pumps

Buyers often group general diesel pumps with EMD-specific soakback units, but the purpose differs. EMD soakback component design supports post-shutdown lube oil flow through turbo galleries. Generic diesel engine pumps may lack the control and check valve provisions. An EMD pump uses a matched AC electric drive, vertical shaft orientation, and rotor clearances tuned to turbo bearing needs. The 40182032 part aligns with locomotive parts dimensions and verified interfaces. Always verify OEM description, flow, and pressure. Confirm the product is compatible with your railway locomotive duty cycle and thermal profile.

Cost-Benefit Analysis of OEM vs. Aftermarket

OEM 40182032 assures fit, proven soakback flow, and precise seal chemistry. Aftermarket variants may lower price, yet hidden costs arise from misalignment, fluid aeration, or shaft leakage. Factor downtime, turbo replacement risk, and inspection overhead. OEM documentation supports maintenance intervals, replacement assy kits, and consistent AC motor ratings. Consider global delivery reliability and warranty clarity. A verified OEM component preserves engine parts and protects the turbo rotor. Over a lifecycle, the OEM pump reduces fuel waste from heat damage and avoids repeat labor. The net result is predictable, measurable value.

Choosing the Right Pump for Your Locomotive

Start with the locomotive model, EMD platform, and turbo configuration. Confirm the pump type is AC, vertical, and designated as soakback. Match electrical data, mounting footprint, and shaft interface. Validate lube oil flow against the turbo gallery pressure drop. Check the filter element routing and element rating. Verify the part number 40182032 in the description for OEM replacement. Ensure supply stability, global shipping options, and service kits. If GE or ALCO cross references apply, document them. Choose a supplier who can provide testing data and timely delivery for rail equipment.

Final Thoughts

A correct soakback pump safeguards turbo health and overall engine longevity. The OEM 40182032 component delivers verified flow, proper pressure, and reliable vertical orientation for EMD diesel engines. Reliable supply and clear documentation simplify procurement and maintenance planning. Global delivery options reduce downtime risk for railway fleets. Filter element management supports clean fluid and stable performance. Replacement assy availability streamlines overhauls. When comparing pumps, prioritize proven soakback purpose and OEM tolerance. Align every selection with the locomotive model, rail equipment interfaces, and your operating profile.

Recap of Key Points

The OEM part 40182032 is engineered for EMD soakback duty. It keeps lube oil moving after shutdown to protect the turbo rotor and shaft. The AC electric, vertical type simplifies installation and priming. Accurate description and compatible fittings ensure trouble-free replacement. Use a matched filter element to control contamination. Confirm supply chains, shipping windows, and testing data. Balance upfront cost against turbo replacement risk. Validate GE and ALCO cross references if needed. Standardize across your locomotive fleet to stabilize performance and reduce maintenance variability.

Why Choose Mikura International for Your Needs

Mikura International provides OEM 40182032 with verified specifications, global shipping, and dependable delivery. We offer accurate model matching for EMD diesel engine platforms and railway locomotive fleets. Our product documentation covers description, flow tests, and electrical data. We supply replacement assy kits and matching filter elements. Our worldwide support reduces lead time risk and ensures consistent availability. We help you align pump type, vertical mount, and shaft interface to your rail equipment. Expect responsive service and reliable stocking strategies for mission-critical locomotive parts.

Final Recommendations

Specify OEM 40182032 for EMD soakback applications. Confirm AC vertical type, flow rate, and gallery pressure alignment. Use an approved filter element and maintain clean lube oil. Validate mount geometry, shaft seals, and electrical settings. Keep a replacement assy on hand for critical routes. Track performance data by model to optimize cycles. Leverage worldwide shipping to minimize downtime. If your fleet includes GE or ALCO equipment, verify cross references before purchase. Partner with a supplier that can provide documentation, testing data, and stable global supply.

FAQ

Q: What is the Locomotive Lube Oil Soakback Pump OEM Engine Part 40182032?

A: The 40182032 is an OEM locomotive lube oil soakback pump designed for Diesel/EMD engines. This product description identifies it as a precision-engineered assy that returns residual oil from the turbo and related components back to the lubrication system. It includes a rotor, shaft, and fluid passages sized for the engine’s oil element and filter requirements, and is built to OEM tolerances for reliable long-term operation in heavy-duty locomotive parts applications.

Q: How does the soakback pump interact with the turbo and lube oil system?

A: The soakback pump scavenges residual oil from the turbocharger housing and other elevated points after shutdown, preventing oil pooling and potential coking. It works in concert with the oil filter and element to route returned fluid back to the sump or pressurized supply circuit. By removing trapped oil from the turbo, the pump helps protect the turbo bearings and shaft from unnecessary wear and preserves oil cleanliness within the lube system.

Q: Is the 40182032 compatible with electric or GE locomotive models, or only Diesel/EMD engines?

A: The OEM designation 40182032 is specified for Diesel/EMD engines; compatibility with electric or GE platforms depends on the specific engine and subsystem architecture. Some retrofit or cross-application installations may be possible if mounting, drive, and fluid interfaces match, but confirmation through part cross-reference and engineering verification is required before using it in electric or GE locomotive parts applications.

Q: What are the key components inside this assy, such as rotor, shaft, and element?

A: The assy typically comprises a precision-machined rotor and shaft assembly, housing with fluid ports, internal seals, and mounting interfaces. While the soakback pump itself does not contain a filter element like a primary oil filter, it works upstream or downstream of an oil element and filter assembly. The rotor and shaft are balanced for high-speed operation and are designed to handle the viscosity and thermal conditions of locomotive lube fluid.

Q: How is this product powered – is it an electric pump or mechanically driven?

A: Soakback pumps for Diesel/EMD applications can be either electrically driven or mechanically driven depending on OEM design. The 40182032 is commonly implemented as an electric sub-assembly in many modern installations, allowing post-shutdown operation independent of engine speed. Verify the part spec sheet for exact drive type for your locomotive, as some variants may be mechanically linked to the engine.

Q: What should maintenance teams check regarding supply, filter, and fluid when installing or servicing this pump?

A: Maintenance teams should verify the lube oil supply pressure and flow paths, ensure the oil filter and element are within service life and free of bypass indicators, and confirm fluid cleanliness and correct viscosity grade. Inspect pump mounting, electrical connections if electric, and the rotor/shaft for signs of wear. Regular checks of the return lines from the turbo and the pump’s discharge to the sump or supply are essential to prevent fluid cavitation or blockages.

Q: Are there common failure modes for this soakback pump and how can they be prevented?

A: Common failure modes include rotor/shaft wear, seal degradation, electrical motor failure (if electric), and clogging from contaminated fluid or degraded filter elements. Prevention includes scheduled inspection and replacement of filters and oil elements, maintaining correct fluid quality and levels, ensuring proper shipping and storage to avoid contamination prior to installation, and following OEM torque and alignment procedures during assembly.

Q: What should be considered regarding shipping, delivery, and receiving of this locomotive parts assy?

A: When ordering part 40182032, ensure the supplier provides clear shipping documentation, correct part number, and protective packaging to prevent damage to the rotor, shaft, and mating surfaces. On delivery, inspect the assy for physical damage, verify serial numbers against the order, and confirm completeness of included fittings and electrical connectors. Store the unit in a clean, dry environment to avoid contamination before installation.

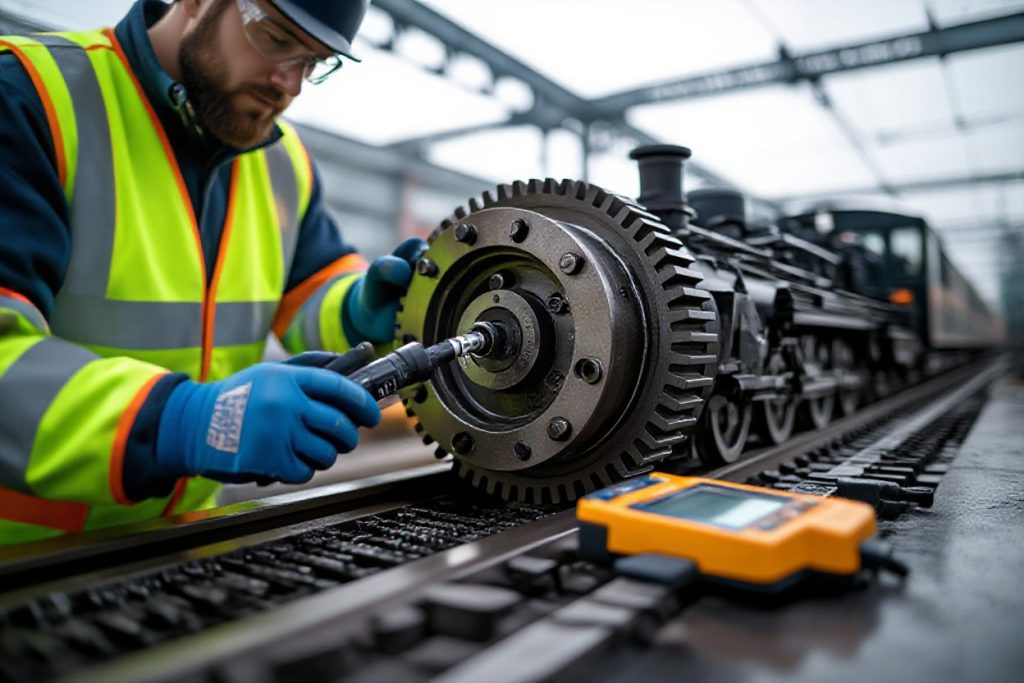
What Are Reliable Locomotive Traction Gear Inspection Methods?

What Are Reliable Locomotive Traction Gear Inspection Methods?

What the Heck is Traction Gear Anyway?

Your biggest headache is unplanned downtime from failing traction gears. You lose revenue, schedules slip, and sourcing the right spare feels like gambling. You need clear checks, reliable parts, and inspection routines that actually work. Below are fast, actionable steps you can use right away.

  • Set inspection intervals by operating hours, not calendar dates.
  • Use borescope checks before full disassembly.
  • Add vibration monitoring to early-fault detection.
  • Keep a calibrated magnetic particle kit on-site.
  • Stock critical spares from trustworthy exporters like Mikura International.
  • Require material certificates with every gear delivery.
  • Create a simple damage-photo log for trend tracking.

Defining Traction Gear

There’s this late-night call I got from a yard foreman once, gears whining and a train stuck on a grade, and you feel that sinking pit in your stomach. You want to know what actually failed, right? That story shows how visible problems can hide deeper gear issues.

Traction gear means the gearbox, pinions, and final drives that transmit motor torque to wheels. You deal with gears, shafts, bearings, housings, and seals. They take huge loads, intermittent shocks, and heat. Your parts choices affect performance, life, and maintenance needs.

ComponentFunctionTypical Concern
PinionInitial torque transferTooth chipping, micro-pitting
Gear setSpeed reductionWear, misalignment
Final drive housingSupport and sealingCracks, oil leaks

“Mikura International inspects each traction gear batch and provides full traceability.”

Why It Matters for Locomotives

Gear damage ruins schedules, raises fuel use, and can cascade into axle failures, and you pay dearly for that. Ever had a single failed gear hold up an entire consist? It happens, and it hurts margins and reputation.

The traction gear directly affects tractive effort, efficiency, and ride quality. If gears wear or misalign, your motors run hotter and consume more energy. Your maintenance window shrinks and costs climb. You need inspection data to act early.

Inspection MethodWhat It FindsWhen to Use
VisualCracks, oil leaks, pittingDaily walkarounds
BorescopeTooth faces without disassemblyQuarterly or before overhaul
Magnetic particleSurface and near-surface cracksAfter impact events
UltrasonicSubsurface defectsAnnual deep inspection
Vibration analysisMisalignment and pitting signaturesContinuous monitoring

Practical tips you can use right now:

  • Log borescope photos with timestamps for trend analysis.
  • Match replacement gears to OEM specs and material certificates.
  • Use vibration baselines to spot gradual tooth damage.
  • Prioritize magnetic particle tests after shock events.
  • Keep a vendor-approved parts list and reorder points.

Before you commit to a spare parts order the biggest pain is sudden traction gear failure and long downtime. You lose schedule slots, budgets blow out, and crews scramble at odd hours. You need inspection data that’s reliable, clear, and fast to act on. Downtime costs you real money.

  • Set clear inspection intervals tied to operating hours and mileage.
  • Prioritize critical axles and pinion teeth for early checks.
  • Use a mix of visual and instrument checks to reduce misses.
  • Log findings in a single system for trend spotting.
  • Train on common defect signatures, not just procedures.
  • Order replacement parts with lead times in mind.
  • Use vendors like Mikura International for consistent part quality.

What Are the Common Inspection Methods?

MethodSensitivityTypical FindingsCost per Inspection
VisualLowWear, leaks, loose fastenersLow
Vibration AnalysisMedium-HighImbalance, misalignment, bearing faultsMedium
Ultrasonic TestingHighCracks, internal flawsMedium-High
Magnetic ParticleHigh (surface cracks)Surface and near-surface cracksMedium

“Mikura International recommends combining methods for best coverage.”

Visual Inspections – The First Line of Defense

Defense starts with you walking the bogie, running your eyes along gears and shafts. You can catch oil seepage, chipped teeth, and loose bolts fast.

It’s simple, fast, and inexpensive. But it won’t find hidden cracks or early bearing defects. So you use it to flag parts for deeper testing.

Vibration Analysis – Does It Really Work?

If you want earlier warnings this method pays off. You mount accelerometers or use handheld sensors at key bearing points. The signal patterns tell you imbalance, misalignment, and bearing wear.

It takes some skill to read spectra, and trend data matters more than a single snapshot. You’ll see peaks and harmonics – those tell stories.

Line data over weeks or months separates transient events from real faults. Trending vibration amplitude against speed gives you actionable thresholds.

Ultrasonic Testing – Sounds Fancy, Right?

Analysis with an ultrasonic probe will find internal cracks that visual checks miss. You scan teeth roots, root radii, and weld zones for high-frequency echoes.

It’s fast for spot checks and good for post-event failure digs. You still need calibration blocks and trained techs to avoid false positives.

Vibration coupling often indicates where to focus your ultrasonic scans. Use vibration trends to target ultrasonic inspections and save time.

Magnetic Particle Inspection – How It Works

Inspection uses magnetic fields and particles to reveal surface cracks. You magnetize the gear area, apply particles, and watch the pattern concentrate at flaws.

It’s especially useful after repairs, during overhaul, or when fatigue cracking is suspected. It’s inexpensive and clear when done right.

First prep the surface properly. Paint, oil, and scale hide defects. Clean thoroughly, then apply wet or dry particles for best visibility.

When to UseBest ForAction
VisualDaily rounds, leak detectionMark parts for deeper testing
VibrationIn-service monitoringSchedule maintenance before failure
UltrasonicInternal flaws, post-eventConfirm crack presence
Magnetic ParticleSurface cracks, weldsVerify repair integrity
  • Tip: Combine visual, vibration, and ultrasonic for best fault coverage.
  • Tip: Keep a 12-month vibration trend per locomotive set.
  • Tip: Use magnetic particle for components after heavy cyclic loading.

Final practical point – you’re buying spare parts to avoid downtime. Align inspection outputs with procurement lead times. If the test says a gear needs replacement within three weeks, you should already have a Po approved. Mikura International can supply matched gears with documented inspection history to cut that gap.

The Pros and Cons of Each Method

Unlike most overcomplicated guides, you can cut traction gear failures by choosing the right inspection mix. You face downtime, unexpected failures, and spare parts delays. You need clear choices, fast. This chapter gives practical trade-offs so you can pick methods that lower risk and cost.

  • You can reduce surprise breakdowns by matching method to fault type.
  • You should schedule vibration checks when bearings heat up or hum.
  • You can use ultrasonic for hidden cracks early on.
  • You should pair visual checks with topology data for better coverage.
  • You can save budget by using oil analysis to prioritize deeper tests.

Pros and Cons at a Glance

MethodPros / Cons
Visual InspectionPro: Fast, low cost. Con: Misses subsurface defects.
Vibration AnalysisPro: Early fault detection. Con: Needs baseline and expert analysis.
Ultrasonic TestingPro: Finds internal cracks. Con: Surface prep and couplant needed.
Magnetic Particle InspectionPro: High sensitivity to surface flaws. Con: Limited to ferrous parts.
Oil AnalysisPro: Trends wear and contamination. Con: Indirect, needs interpretation.
Thermal ImagingPro: Quick hotspot mapping. Con: Can’t identify root mechanical faults.
Borescope / EndoscopyPro: Inspect internal geometry without disassembly. Con: Limited field of view.
Eddy Current TestingPro: Good for cracks near surface on nonferrous parts. Con: Sensitive to geometry.
Dye PenetrantPro: Cheap and simple for open cracks. Con: Not for subsurface defects.
Laser AlignmentPro: Prevents misalignment wear. Con: Requires precision fixtures.

Visual Inspections – Easy, But Is It Enough?

With visual checks you get instant feedback. You can spot broken fasteners, oil leaks, misalignment and scorched gear teeth right away. You save time and money when you catch obvious defects before they bite you during service.

But visual alone won’t find hairline subsurface cracks or early bearing distress. You need to layer methods. Pair visuals with oil analysis or vibration trending and you get far better coverage without huge cost increases.

Vibration Analysis – Seriously Effective or Overrated?

On paper vibration analysis finds imbalance, misalignment, and bearing wear early. You can quantify defects and track progression. For traction motors and gearboxes, it often gives the earliest measurable sign of trouble.

Yet you need good baselines and skilled analysts. False positives happen. And you’ll pay for sensors, data loggers, and trending software. So it’s powerful, but you must use it right and regularly.

Another big win is condition-based maintenance. You can plan part buys and shop visits. Mikura International can help you match replacement schedules to vibration trends, so you avoid rush orders and long delays.

Ultrasonic Testing – What’s Good and What’s Not?

Pros: ultrasonic testing locates internal flaws you can’t see. It spots cracks, porosity, and inclusions inside gear teeth and axle journals. For traction gear, it finds faults long before components fail.

It’s relatively fast and portable. You can inspect large gears in-situ without full teardown. But technique matters – probe angle, coupling, and scan coverage all change your detection odds.

Good ultrasonic programs include calibrated reference blocks and documented buy-back criteria. Train your team, document findings, and correlate results to vibration and oil data for a solid inspection strategy.

Magnetic Particle Inspection – Worth the Hype?

Magnetic particle testing is superb for surface and near-surface cracks on ferrous traction components. You’ll get clear indications on welds, shafts, and gear roots. It’s visual and easy to interpret with training.

However it won’t work on nonferrous alloys. Surface prep, demagnetization, and environmental controls add time. You also need strict process control to avoid missed indications.

Understanding application limits will save you money. Use magnetic particle for shafts and gear roots, but pair it with ultrasonic for deeper flaws. Mikura International recommends inspection matrices that mix methods by part type and risk level.

Magnetic Particle Inspection - Worth the Hype?

My Take on Choosing the Right Inspection Method

When Many assume a quick visual check will catch every traction gear fault, that’s a common misconception. You can’t spot subsurface pitting or early-stage fatigue with sight alone. So you need methods that give repeatable data, not just a thumbs up. Want fewer surprises and less downtime? Of course you do.

  • Prioritize inspection methods that detect the failure modes you see most often.
  • Match method sensitivity to part criticality and service hours.
  • Factor in inspection frequency versus lifecycle cost.
  • Train your crew on one or two methods well, rather than many poorly.
  • Use condition trends, not one-off checks, to trigger repairs.
  • Lean on suppliers for test specimens and validation-Mikura International helps with parts and technical guidance.
  • Document results so you can prove the decision to auditors and operations.
MethodDetectsRelative CostBest Use
VisualSurface defects, oil leaksLowDaily walk-arounds, quick triage
UltrasonicSubsurface cracks, material lossMediumFatigue-prone gears, periodic checks
Magnetic ParticleSurface and near-surface cracksMediumWorn shafts, gear teeth edges
Eddy CurrentSurface cracks, conductivity changesMedium-HighThin components, speedy scanning
ThermographyFriction hotspots, lubrication failuresLow-MediumRunning inspections, bearings, couplings

Factors to Consider When Selecting

You might think cost is the only thing that matters. It isn’t. The real decision mixes detection capability, downtime, and the kinds of failures you actually see on your locomotives. Pick methods that align with those failure modes and your skill set.

  • Failure mode coverage – what faults occur most on your traction gears?
  • Detection depth – surface only, or subsurface too?
  • Downtime impact – can the locomotive be inspected live?
  • Training needs – how fast can your team be competent?
  • Equipment and consumables – buy versus rent versus outsource.
  • Data and traceability – digital records help trend analysis.

Any method you pick should be validated against your real-world failures and fit your maintenance plan.

Aligning Inspection Methods with Your Budget

You don’t have to pick the most expensive tech to get reliable results. Start with a hybrid approach: frequent low-cost checks and periodic high-sensitivity tests. That combo stretches budget and catches problems early. Want an example? Mix daily visual rounds with quarterly ultrasonic scans.

Inspection budgets often sink when parts lead times are long or spares are scarce. Use suppliers who can back up inspections with quick-turn genuine spares. Mikura International exports quality locomotive parts and can help you pair inspection choices to available spares, cutting total lifecycle cost and downtime. Now

Tips for a Successful Inspection Process

Now you face the same headache every quarter: unexpected traction-gear failures, rushed repairs, and runaway spare-part costs. If your inspection timing is off or records are fuzzy, you buy wrong parts, wait days, and lose revenue. You need a repeatable process that keeps your fleet rolling and costs predictable.

  • Set fixed windows for high-risk gear checks to cut surprise failures.
  • Use condition-based triggers from vibration and oil analysis.
  • Keep a curated spares list tied to inspection outcomes.
  • Calibrate and log tools before each shift.
  • Train technicians on wear patterns for traction gears.
  • Use simple KPIs: time-to-detect, time-to-repair, parts lead time.
  • Document each inspection in a searchable record.
  • Work with a trusted exporter like Mikura International for fast parts supply.
ApproachWhen to UseBenefits
Scheduled InspectionsRegular fleet cyclesPredictable workload, easier parts planning
Condition-Based InspectionsAfter alarm or anomalyTargets problems early, reduces unnecessary checks

“Mikura International sees fleets reduce emergency buys by up to 30% with disciplined inspections and parts planning.”

Planning Your Inspection Schedule

While standing beside a sidelined locomotive you wonder why the crack wasn’t caught sooner, you can change that. Start by mapping each traction-gear assembly to a risk score. Use past failure data and hours-in-service to rank priorities. It’s not rocket science, it’s common sense and discipline.

While you’ll want to inspect often, don’t overdo it and burn crews out. Mix scheduled cycles with condition triggers. That gives you coverage and saves labor. And keep spare-part lead times in the calendar so you don’t wait, because parts delays kill uptime.

Involving Your Team – Why It’s a Must

With one technician spotting a tiny tooth wear pattern, you avoided a costly breakdown last winter, and that tells you something. Get frontline techs in the plan early. Ask them what tests actually work in the yard and what tools slow them down.

With short, focused training sessions you’ll up detection rates fast – people respond to simple, practical tips. Use shift handovers to highlight trends. Give techs ownership of small checks and reward accurate reporting, it builds trust and better data.

To make this stick, run small audits and review sessions monthly. Keep feedback loops tight and fix paperwork pain points quickly. When your crew sees inspection wins, they buy in and you get fewer surprises.

Any missed inspection step can double your downtime and costs.

Choosing the Right Inspection Method

Step-by-Step Guide to Visual Inspections

The biggest headache you face is missed defects that cause lead-time delays and costly downtime. You need repeatable inspections, quick decisions, and reliable suppliers. This short guide gives clear, practical steps you can apply today to cut inspection time and raise fault detection rates, so your spares buying works better.

  • Standardize a checklist you use every time.
  • Train your team on what good and bad look like.
  • Use photos to build a defect library for comparison.
  • Inspect under consistent lighting and angles.
  • Log findings in a shared system right away.
  • Escalate any uncertainty to engineering quickly.
  • Match part numbers and serials before ordering.

Inspection Steps and Guidance

StepWhat you check and how
1. PreparationVerify documentation, service history, and OEM part specs. Have tools, flashlight, mirror, and camera ready. Set safety lockout and secure the traction motor area.
Key Areas to Focus OnClearly start at the traction motor casing and bearings, then follow the drivetrain path. You check seals, fasteners, and coupling alignment first. Clearly inspect brushes, commutators, slip rings and cooling ducts. You want to spot wear, burns, pitting, corrosion, scoring or loose hardware.
Common Red Flags to Watch Out ForAreas where paint flaking, seepage, or fresh metal shavings appear often mean deeper faults. You should flag vibration marks and uneven wear immediately. To decide fast, use these quick rules: cracked insulation, heat discoloration, and persistent oil leaks mean stop and escalate. You won’t gamble with traction parts.
4. Measurement & DocumentationRecord serials, torque readings, and clear photos of defects and orientation. Keep one photo per view and a short note for each defect.
5. Decision & ProcurementClassify defects: repairable, replaceable, or emergency. For replacements, match OEM specs and use trusted suppliers like Mikura International.
Quick ChecklistBearings: play, noise, sealing. Couplings: alignment and wear. Cooling: blockage and corrosion. Electrical: discoloration and cracked insulation. Fasteners: torque and missing parts.
Tip from the field“A single photo beats ten words.” Use time-stamped photos. They save disputes and speed approvals.
Why Mikura helpsMikura International is a top exporter of locomotive and marine engine parts. You get traceable spares and consistent part specs.
Step-by-Step Guide to Visual Inspections

What Happens If You Skip Inspections?

You worry about unplanned downtime and surprise procurement costs. It hits your budget and your delivery commitments hard, and you end up scrambling for parts. You need predictable lead times and reliable spares, not firefighting. This paragraph nails that pain and points you to practical fixes.

  • Set a fixed inspection calendar and stick to it.
  • Use condition-based triggers, like vibration thresholds.
  • Keep a 12-month forecast of common spare parts.
  • Pre-qualify alternate suppliers through Mikura International.
  • Stock wear items with the highest MTBF first.
  • Document failures and update maintenance procedures.
  • Train staff on quick visual and borescope checks.

The Risks of Overlooking Traction Gear

Assuming you skip traction-gear checks, wear accelerates quietly. Bearings and gears degrade faster than you expect. That leads to higher friction, heat, and sudden failure.

You lose traction reliability, and your fleet availability drops. One bad gearbox can ripple into schedule losses. You end up paying overtime, rush freight, and premium parts.

MetricSkipped InspectionsRegular Inspections
Annual failure rate8-12%2-4%
Average downtime per failure48-72 hours8-24 hours
Average repair cost per event$25,000$6,000

Real Case Studies and What They Teach Us

On one regional fleet, missed inspections let micro-pitting spread across traction gears. Operators thought minor noise was tolerable. It wasn’t – and the repairs cost way more than timely part swaps.

  • Case 1 – Fleet A: 30 locomotives. Missed 2 inspection cycles. Result – 6 gear failures in 12 months. Downtime total 360 hours. Repair spend $180,000.
  • Case 2 – Fleet B: 18 locomotives. Switched to condition monitoring. Result – 1 gearbox failure in 12 months. Downtime 16 hours. Spare cost $7,500.
  • Case 3 – Urban haul: 45 locomotives. No spare strategy. Result – parts flown in urgently. Logistics premium 42% of part cost.

A follow-up program saved Fleet A real money. They adopted periodic borescope checks, and Mikura International supplied pre-matched gear sets. Failures dropped quickly, and uptime improved within one quarter.

  • Follow-up Data – Fleet A: After fixes, failures fell from 6 to 1. Downtime cut from 360 to 48 hours. Annual repair spend down 68%.
  • Supply Impact – Lead time before plan: 14 days average. With prepped stock: 48 hours average.
  • ROI Snapshot – Inspection program cost recovered in 4 months via avoided repairs.

Summing up

Considering all points, comparing quick visual checks to ultrasonic testing shows you different strengths and limits. You use visual for routine spotting – it’s fast and cheap. And you’ll lean on vibration and thermography for early wear detection. But what ties it all together is method mix, frequency, and data.
Prioritize the right mix of methods for your traction gears.

So, schedule inspections by risk – more often for high-load units. Want fewer breakdowns? Train your crew, log trends, and act on anomalies fast. You can set thresholds from vibration, oil analysis, and borescope images. Buy genuine spare parts and consult Mikura International for parts and technical support. Uptime wins.

FAQ

Most sourcing managers face sudden traction gear failures that halt operations. Inspections vary by team and tools, so wear often goes unnoticed until it gets bad. You want reliable methods, clear data, and faster decisions to buy the right spare parts. This FAQ helps fix that.

  • Prioritize critical gear with condition-based checks.
  • Use simple visual templates to get consistent results.
  • Add vibration and oil analysis for early fault detection.
  • Keep inspection records tied to serial numbers.
  • Set minimum spare-stock levels based on failure rates.
  • Work with one trusted supplier for certified parts.

Q: What visual inspection methods reliably detect traction gear issues?

A: Many assume a quick visual check will spot everything. It won’t. Visual inspection is the first line of defense. It finds tooth scoring, broken teeth, rust, poor lubrication, and misalignment.

So what should you do on each stop? Use a short checklist and stick to it. Do it the same way every time – consistency beats random looks.

  • Tooth profile check – compare to baseline or drawing.
  • Surface pitting and scoring – use good light and a 10x loupe.
  • Backlash and runout – measure with gauges.
  • Lubrication condition – colour, metal particles, viscosity.
  • Bearing play – hand and dial-check under load conditions.

Quick tip – photograph the same areas each inspection. Photos build trend evidence fast.

Q: Which non-destructive testing methods are best for locomotive traction gears?

A: Some think NDT is expensive window-dressing. It isn’t always. NDT gives early warnings you can act on, and methods fit different budgets.

Pick the method that matches the failure mode you expect. Want subsurface cracks? Go ultrasonic. Worried about small surface cracks? Use dye penetrant or magnetic particle testing.

MethodBest forProsCons
Visual + MagnificationSurface wearCheap, fastMisses subsurface flaws
Dye PenetrantSurface cracksLow cost, simpleNeeds cleaning, not for porous surfaces
Magnetic ParticleSurface and near-surface cracksFast, reliable on ferrous gearsOnly for magnetic materials
Ultrasonic TestingSubsurface defects, pittingDeep detection, quantitativeRequires skilled operators
Eddy CurrentSurface and near-surfaceGood for thin sectionsSkin-depth limits
Vibration & Oil AnalysisEarly fault trendsNon-invasive, continuousNeeds baseline and trend analysis

Combine methods. Visual plus vibration and oil analysis catches many issues early. Add targeted ultrasonic if trends look bad.

Q: How should I set up a traction gear inspection program and buy spare parts smartly?

A: It’s often believed inspection programs are box-ticking exercises. They shouldn’t be. A risk-based program cuts downtime and lowers spare part costs.

Start by mapping critical assets and failure modes. Then assign inspection types and frequencies by risk level. Data guides spares stocking and ordering.

  1. Classify gears by mission-critical status and failure impact.
  2. Define inspection methods per class – visual, vibration, NDT.
  3. Set sampling frequency – daily, weekly, monthly, or condition-based.
  4. Record results with serial numbers and photos.
  5. Trigger spare orders when wear exceeds defined thresholds.

Procurement tips for sourcing managers:

  • Keep a preferred supplier list and standard part numbers.
  • Negotiate agreed lead times and emergency replenishment.
  • Require traceable material certificates and inspection reports.
  • Stock critical spares based on MTBF and lead time math.

In-house vs outsourced inspections:

ApproachWhen to useTrade-off
In-houseHigh frequency, basic checksLower cost, needs training
Outsourced specialistAdvanced NDT, auditsHigher cost, expert reports

“Data beats guesswork every time,” says a sourcing lead at Mikura International.

Need parts fast? Mikura International supplies certified traction gears and quick global delivery. Use inspection data to place smarter orders and avoid costly downtime.

How Has Traction Gear Technology Revolutionized Trains?

How Has Traction Gear Technology Revolutionized Trains?

Sourcing reliable locomotive components presents significant challenges. Managers frequently face high gear failure rates and unpredictable downtime. Inferior gearing directly impacts operational schedules and safety. Incorrect part specification causes premature wear and catastrophic failure. Mikura International supplies certified replacement parts for these critical systems. This ensures maximum uptime for your global fleet operations.

  • Identify and mitigate uncertainty in component material quality immediately.
  • Use only certified, high-strength alloy steel for all replacement gears.
  • Avoid prolonged lead times through dedicated inventory programs.
  • Install replacement components designed for extended maintenance cycles.
  • Consult experts for precise Gear Ratio Selection matching OEM specifications.
  • Minimize the risk of premature bearing failure using verified parts.
  • Employ robust, high-durability Traction Motor Pinion Gears consistently.
  • Ensure parts meet high Tractive Effort demands across all load profiles.

The Foundation of Locomotive Gearing Reliability

The Foundation of Locomotive Gearing Reliability

Effective locomotive operation depends entirely on robust power transmission. The gear system translates the torque from the Traction Motors to the axles. This process determines the locomotive’s Tractive Effort and speed capability. Failure in this system leads to immediate operational shutdown.

Component selection requires rigorous material verification. Low-quality components increase the Maximum Traction Motor Revolutions Per Minute beyond safe limits. This causes excessive heat and rapid component degradation. Sourcing managers must prioritize proven reliability over low initial cost.

Critical Factors in Gear Ratio Selection

The choice of Gear Ratio Selection is crucial for balancing speed and pulling power. A higher ratio favors high Tractive Effort necessary for heavy freight operations, such as those utilized by Norfolk Southern. A lower ratio supports higher speeds required for passenger services like Amtrak or VIA Rail.

Understanding the application profile dictates the required gearing specification. Incorrect ratios compromise performance and increase stress on the entire powertrain. This affects the lifespan of the engine and the Traction Motor Pinion Gears.

Analyze the operational requirements based on track gradient and payload. Define the necessary Minimum Continuous Speed for your fleet. This prevents overheating the traction motors during sustained heavy pulls.

Gear Ratio TypePrimary BenefitOperational Limitation
High Ratio (e.g., 85:18)Maximum Tractive EffortLower Maximum Speed
Low Ratio (e.g., 62:15)Higher Maximum SpeedReduced Starting Pull

Proper Locomotive Gearing is essential for meeting operational benchmarks. Mikura International provides components certified to meet the demanding standards of major rail operators, including CP Rail and GO Transit.

Expert Insight

“The maximum speed is a function of the gear ratio on a diesel or electric locomotive, because the traction motor armature has a maximum allowable revolutions per minute rating above which mechanical stresses could damage or destroy it,” according to Walter Rosenberger, research and testing operations engineer, Norfolk Southern.

Locomotive Gearing: The Core of Propulsion

Locomotive Gearing: The Core of Propulsion

Locomotive Gearing is the central mechanism for rail propulsion systems. It manages power transfer from the Traction Motors to the axles. This system translates rotational motor energy into linear motion. The gear set determines the locomotive’s performance profile. Different ratios are required for varied operational duties.

Sourcing reliable components for Locomotive Gearing is non-negotiable. Inferior parts lead directly to unpredictable downtime. We provide certified parts that ensure maximum power transmission efficiency.

Function of Traction Motors and Pinion Gears

Traction Motors are essential electrical machines. They convert energy from the diesel-electric system, generating the necessary torque for propulsion. The motor shaft connects directly to the Traction Motor Pinion Gears. These pinion gears mesh with the bull gear mounted on the axle. The durability of these components is crucial for maintaining railway schedules.

The efficiency of power conversion relies entirely on the quality of the Traction Motors and associated gearing. High quality components reduce energy loss and heat generation, which extends the service life of the entire drive system.

Operational limits must be strictly observed. Exceeding the Maximum Traction Motor Revolutions Per Minute (RPM) causes rapid component degradation. This thermal stress drastically shortens motor life. Implement proper maintenance protocols to monitor this critical parameter. We supply robust motors engineered for sustained peak performance.

Criticality of Gear Ratio Selection

Selecting the specific gear ratio dictates locomotive performance characteristics. Sourcing managers must define the intended duty cycle first, as this decision impacts both speed and pulling capability. High ratios are selected to maximize Tractive Effort for heavy loads; this is essential for freight carriers.

For example, operations similar to Norfolk Southern or CP Rail require high ratios. These ratios facilitate pulling heavy tonnage across challenging terrain, such as the Ohio River Valley. A lower ratio favors higher speed capability. Passenger services, such as Amtrak, VIA Rail, or GO Transit, utilize these lower ratios. Proper Gear Ratio Selection balances maximum speed against pulling capacity.

Managing Minimum Continuous Speed

The Minimum Continuous Speed is a vital operational metric. This parameter is directly influenced by the chosen gear ratio. Operating below this speed during prolonged heavy pulls causes motor overheating. This thermal stress severely damages the Traction Motors. Sourcing certified replacement gearing is the first step in mitigating this risk.

Follow these steps to avoid thermal failure related to speed limits:

  1. Verify the specific ratio required for the intended duty cycle.
  2. Ensure replacement Traction Motor Pinion Gears match OEM specifications precisely.
  3. Implement monitoring systems for motor temperature during low-speed, high-load operation.
  4. Review the locomotive’s Engine Ramp Rate settings to ensure smooth power application.

Accurate component specification prevents costly failures. We guarantee the precision required for reliable operation, maximizing your fleet uptime.

Comparison: Gear Ratio Impact Summary

Understanding the trade-offs is essential for procurement decisions. Use the table below to compare typical operational profiles based on Gear Ratio Selection:

Ratio TypePrimary BenefitImpact on Tractive EffortImpact on Speed
High Ratio (e.g., 83:20)Maximum Pulling PowerHigh (Crucial for freight)Lower Top Speed
Low Ratio (e.g., 59:18)Maximum VelocityLower (Suitable for light loads)Higher Top Speed (Crucial for passenger service like Amtrak)

This comparison confirms why specific ratios are non-negotiable. Mismatched gearing compromises the locomotive’s core mission. We ensure every component meets the stringent demands of its specific Locomotive Gearing application.

Expert Insight

“A locomotive’s operational profile is a function of two constraints: its gearing, which dictates the fundamental trade-off between speed and tractive effort, and its minimum continuous speed, a thermal barrier that AC traction technology has significantly minimized compared to older DC systems,” according to a Motive Power Engineer.

Technological Advancements in Traction Gears

Technological Advancements in Traction Gears

Modern Locomotive Gearing has advanced significantly. Improved material science drives this technical revolution. Components now handle greater torque density safely. Specialized processes ensure superior surface hardness and finish. This minimizes operational failures for operators like CP Rail and VIA Rail. Sourcing upgraded components reduces unplanned maintenance costs.

The Critical Role of Traction Motor Pinion Gears

The Traction Motor Pinion Gears endure immense operational stress. They manage power transfer directly from the Traction Motors. These gears face high contact pressures and shock loading daily. Our manufacturing demands superior metallurgy for this application. Case hardening techniques provide exceptional wear resistance, which dramatically extends the component life cycle. Using certified gears is vital for heavy-haul routes, such as those operated by Norfolk Southern.

We utilize specific alloy steels and proprietary heat treatments. These methods actively prevent pitting and surface fatigue. Quality assurance minimizes unexpected failures across the network. Reliability is enhanced even in high-demand environments like the Ohio River Valley lines. This prevents delays for critical freight and passenger services like Amtrak or GO Transit.

Precision Manufacturing Process Steps

Manufacturing precision Locomotive Gearing follows strict procedures. These steps ensure compliance with stringent industry standards. Sourcing managers must verify these processes to guarantee performance matching original specifications.

  1. Material Selection: Choose high-grade forged alloy steel blanks.
  2. Rough Machining: Establish primary dimensions and initial tooth profile.
  3. Gear Cutting: Utilize hobbing or shaping for precise tooth generation.
  4. Heat Treatment: Perform case hardening to achieve required surface durability.
  5. Grinding: Finish the tooth flank geometry for optimal mesh.
  6. Inspection: Verify dimensions, hardness, and profile using CMMs.
  7. Final Coating: Apply protective treatments against corrosion and wear.

Impact on Locomotive Performance Metrics

Advanced gearing directly affects key performance metrics. Optimized gearing improves the locomotive’s Tractive Effort capability. Accurate production ensures precise Gear Ratio Selection, which is critical for meeting specific duty cycles. Proper gear integrity prevents issues related to Minimum Continuous Speed requirements. Furthermore, high-quality gears safely manage the Maximum Traction Motor Revolutions Per Minute.

Sourcing reliable Locomotive Gearing supports efficient power use. It helps operators maximize benefits from the Engine Ramp Rate. This focus on component quality ensures sustained operational efficiency.

Impact on Rail Operations and Fleet Management

Impact on Rail Operations and Fleet Management

Advanced Locomotive Gearing significantly optimizes rail operations. Optimized Gear Ratio Selection increases overall fleet flexibility. Passenger services like Amtrak use lower ratios for top speed. Heavy freight operators in the Ohio River Valley demand maximum Tractive Effort.

Case Studies in Operational Performance

Major operators rely on precise gearing to meet demanding schedules. Commuter services like GO Transit demand high acceleration capacity. Their Traction Motors must handle frequent starts and stops reliably. Freight lines such as CP Rail and Norfolk Southern prioritize hauling capacity. They utilize higher gear ratios to maximize Tractive Effort.

Reliable components reduce unscheduled maintenance events. Fewer failures improve operational efficiency directly. Sourcing managers must prioritize certified component quality, as this quality drives overall rail network performance.

Selecting the Correct Gear Ratio Components

Proper Gear Ratio Selection is critical for component longevity. This comparison guides sourcing decisions for specific applications. Use this data to specify the correct Traction Motor Pinion Gears. Matching the gear set to the operational profile is essential.

ParameterFreight ApplicationPassenger Application (e.g., VIA Rail)
Typical Gear RatioHigher (e.g., 62:15, 74:18)Lower (e.g., 59:18, 60:21)
Primary FocusMaximum Tractive EffortMaximum Speed Capability
Speed Limit Range65 to 75 MPH90 to 135 MPH
Critical LimitMinimum Continuous SpeedMaximum Traction Motor Revolutions Per Minute
Operational EnvironmentProlonged low-speed heavy haulHigh-speed, dynamic operation

Practical Advice for Ratio Selection

Specifying the wrong gear ratio causes immediate problems. Freight ratios used in passenger service limit top speed severely. Passenger ratios used in heavy freight risk motor overheating. This occurs because the Traction Motors operate below the Minimum Continuous Speed. Always consult the locomotive service manual first. Ensure the replacement gear material matches or exceeds OEM specifications.

Consider the required Engine Ramp Rate when selecting parts. High acceleration demands superior gear strength. Certified suppliers guarantee material integrity and dimensional accuracy. Source components that handle maximum thermal and mechanical stress.

Impact of Gear Failure on Scheduling

A catastrophic gear failure stops the train immediately. This results in severe schedule disruption for carriers. Sourcing managers must reduce the risk of this costly downtime. High-quality Traction Motor Pinion Gears are an investment in reliability. Mikura International provides certified components to mitigate this risk.

Expert Insight

“Traction gearing is the critical determinant of locomotive capability; a ‘taller’ ratio maximizes speed at the cost of tonnage capacity, and using the wrong ratio risks catastrophic motor failure and severe schedule disruption,” notes a Railway Engineering Specialist.

Maintenance Protocols and Longevity

Regular maintenance dictates traction gear lifespan. Rigorous inspection prevents minor faults from escalating into failures. Managers must strictly follow lubrication schedules. Monitoring system vibration detects early component wear. These protocols safeguard the critical Traction Motors.

Preventative steps maximize the lifespan of Locomotive Gearing. High operating temperatures require immediate attention. Ensure proper oil viscosity according to manufacturer specifications. Failure to maintain tolerances increases friction and heat generation.

Protecting Locomotive Gearing Through Control

Modern locomotives utilize complex power management systems. Effective Wheelslip Software manages traction delivery precisely. This prevents damaging wheel spin on the rail surface. Proper control preserves the life of the sensitive Traction Motor Pinion Gears.

Operators requiring high Tractive Effort, such as Norfolk Southern, rely on this control. Effective wheelslip management maintains adhesion under heavy load conditions. This reduces unnecessary mechanical stress on the entire drive assembly.

The Engine Ramp Rate is a crucial operational setting. This rate controls the speed of diesel engine power increase. A controlled ramp rate minimizes sudden torque spikes on the drivetrain. This reduces shock loading on the Locomotive Gearing. Uncontrolled ramping accelerates wear and reduces component lifespan.

Sourcing Strategy for Maximum Gear Longevity

Sourcing high-quality replacement parts is crucial for fleet reliability. Inferior components guarantee premature failure and costly downtime. We specialize in components that meet or surpass OEM standards. Sourcing managers must demand certified components and established inventory support.

Follow these steps when selecting replacement Locomotive Gearing:

  1. Verify Material Certification: Ensure all steel meets specified metallurgical standards.
  2. Inspect Tooth Finish: A smooth surface minimizes friction and abrasive wear.
  3. Confirm Heat Treatment Records: Verify case depth and core hardness for optimal durability.
  4. Evaluate Supplier Traceability: Demand full provenance documentation for every gear set.
  5. Utilize Unit Exchange Service: This option minimizes locomotive downtime by providing certified refurbished units instantly.

We provide comprehensive support for your entire maintenance cycle. Our inventory covers major platforms including EMD, GE, and ALCO. Choosing certified quality guarantees long-term operational success. We ensure rapid response and guaranteed on-time delivery.

Frequently Asked Questions

What is the importance of Gear Ratio Selection?

Gear Ratio Selection dictates the locomotive’s operational profile. A higher ratio maximizes pulling force, or Tractive Effort. This is vital for heavy freight hauls by operators like Norfolk Southern. A lower ratio maximizes top speed for passenger service, such as VIA Rail. Selecting the wrong ratio compromises Locomotive Gearing efficiency and longevity.

How do Traction Motors affect overall train performance?

Traction Motors deliver power directly to the wheels. They convert generated electrical energy into torque at the axle. Performance impacts acceleration and sustained speed profiles. Reliable Traction Motors are essential for maintaining schedules for Amtrak or CP Rail. Failure leads directly to severe operational delays.

What is the Minimum Continuous Speed threshold?

The Minimum Continuous Speed (MCS) is a critical safety threshold. It is the lowest speed allowed at maximum current draw. Operating below MCS causes extreme heat buildup in the Traction Motors. This rapid heating damages insulation and winding integrity. Conversely, exceeding the Maximum Traction Motor Revolutions Per Minute risks mechanical failure. Adhere strictly to the specified speed range limits.

Why are Traction Motor Pinion Gears so critical?

Traction Motor Pinion Gears are the primary mechanical interface. They transfer high torque from the motor shaft to the axle gear. These gears endure massive shock loads, especially in dynamic regions like the Ohio River Valley. Their material quality determines the reliability of the entire Locomotive Gearing system. Failure of the pinion gear causes immediate axle stoppage.

How does Engine Ramp Rate relate to gear longevity?

The Engine Ramp Rate manages the speed of power increase. A smooth ramp rate prevents sudden, high-stress torque spikes. Utilizing advanced Wheelslip Software helps control this power application precisely. Controlled acceleration reduces excessive wear on the Locomotive Gearing components. This practice extends component lifespan, crucial for high-frequency services like GO Transit.

What is the benefit of a Unit Exchange Service for Traction Motors?

A Unit Exchange Service minimizes locomotive downtime. Managers receive a tested, certified replacement unit immediately. This practice eliminates the long wait time associated with internal repairs. Mikura International offers certified units for immediate swap. This guarantees faster return to service and lower lifecycle costs.

References

10 Best Diesel Locomotive Frame Components For Durability

10 Best Diesel Locomotive Frame Components For Durability

You’ll need specific high-performance components to maximize your diesel locomotive frame’s durability and service life. Focus on heavy-duty cross-bearers rated for 500,000 lbf shear strength, high-strength steel side sills with 1.5-2.0 safety factors, and corrosion-resistant center plate assemblies. Integrate reinforced end structures, impact-absorbing draft gear housing, and precision-engineered traction motor mounts. Your frame’s longevity depends on specialized bearing brackets, modular connection points, and stress-tested weld joints. The following specifications reveal how these components work together to enhance operational reliability.

Key Takeaways

  • High-strength steel side sills and bolsters with reinforced welding distribute loads effectively and prevent structural fatigue during operation.
  • Impact-absorbing draft gear housing with stainless steel composition protects against coupling forces and ensures long-term frame stability.
  • Heavy-duty cross-bearers and support beams meeting 500,000 lbf shear strength requirements provide essential structural integrity.
  • Multiple-layer protection systems with specialized coatings guard against corrosion and environmental damage for extended service life.
  • Wear-resistant bearing support brackets with thermoplastic liners and polyurethane inserts minimize maintenance requirements and increase durability.

Heavy-Duty Cross-Bearers and Support Beams

sturdy structural support components

The structural integrity of diesel locomotive frames depends heavily on the precise integration of cross-bearers and support beams. You’ll find that end cross members and longitudinal beams, when cast in concrete, create the primary foundation for your locomotive’s load-bearing system. These heavy-duty cross-bearers work in conjunction with auxiliary supports that rest on steel girders or separate foundations, guaranteeing ideal weight distribution throughout the frame.

When you’re implementing support beam integration, you’ll need to coordinate with formwork processes to guarantee proper concrete pouring sequence. The cross-bearers, both end and intermediate variants, align precisely with longitudinal beams for maximum structural stability. Your frame’s performance relies on projection foundations that enable localized load transfer without requiring additional substrate reinforcement. Remember, these components must meet strict shear strength requirements – up to 500,000 lbf at collision post bases – to maintain structural integrity during operation.

High-Strength Steel Side Sills and Bolsters

You’ll need to master three critical engineering aspects of high-strength steel side sills and bolsters: optimizing load distribution through strategic force mapping and finite element analysis, implementing multi-layer corrosion prevention coating systems that meet ASTM B117 salt spray requirements, and designing modular connection features that utilize high-grade fasteners with precise torque specifications.

High-Strength Steel Side Sills and Bolsters

Incorporating a die-cast metal frame ensures maximum structural integrity in modern locomotive designs. The integration of these components requires careful attention to stress concentration factors at load-bearing points, while maintaining proper clearances for thermal expansion and contraction during operation. Your specifications must account for dynamic loading conditions with safety factors of 1.5 to 2.0, particularly at bolted joints where side sills interface with bolster assemblies.

Load Distribution Optimization Methods

While modern diesel locomotive frames demand precise load distribution across their structural components, refining high-strength steel side sills and bolsters requires sophisticated stress analysis and material selection protocols. You’ll need to implement advanced load refinement techniques that incorporate dynamic stress testing and ANSYS simulations to validate structural integrity. Your stress analysis methods should utilize Weibull distribution modeling to assess load spectra and predict fatigue performance accurately. Strategically allocating power requirements similar to DFDE plant optimization helps maximize structural efficiency and durability.

Load Distribution Optimization Methods

To achieve ideal results, you must analyze real-time operational data through rainflow counting algorithms and compile thorough load spectrum data. Consider implementing Chi-square minimization for parameter estimation and integrate performance validation metrics that comply with S-N curve analysis standards. This systematic approach guarantees your side sills and bolsters maintain structural integrity while maximizing load-bearing efficiency under various operational conditions.

Corrosion Prevention Coating Systems

Modern locomotive frame protection requires advanced coating systems engineered specifically for high-strength steel side sills and bolsters. You’ll find excellent results using high-solids epoxy solutions like Carboguard 904 or Railplex EE-2020, which provide superior corrosion resistant coatings without primers. The application of these coatings in controlled conditions ensures optimal adhesion and maximum protection against environmental factors.

Corrosion Prevention Coating Systems

For extreme conditions, you’ll want to implement specialized solutions like SUPER THERM® to manage thermal expansion or EonCoat CUI for temperature variations from -256°F to 842°F. Your maintenance strategies should include regular inspections of these protective systems, which can deliver up to 20 years of service life in corrosive environments.

To maximize frame protection, you’ll need controlled-environment application with proper grit blasting preparation. Consider combining treatments for rails and tie plates to enhance system-level durability while reducing long-term maintenance requirements.

Modular Connection Design Features

Since operational reliability depends heavily on frame integrity, high-strength steel side sills and bolsters require precision-engineered modular connections. You’ll find these components refined with high-carbon steel alloys that deliver superior strength-to-weight performance while accommodating diverse coupling needs. Advanced coupler designs utilize 14 standard modules for customized configurations that enhance overall system performance.

Modular Connection Design Features

The modular coupling systems integrate specially configured anchors that adapt to your specific operational requirements, whether you’re using manual or semi-automatic coupler assemblies. These connection points provide essential flexibility through varied attachment methods and movement ranges. You’ll notice the frame’s enhanced fatigue resistance, particularly critical when managing repeated impact loads during coupling operations. The steel grade selections directly correspond to your expected compressive and tensile load patterns, ensuring ideal connection flexibility while maintaining structural integrity throughout the frame assembly.

Corrosion-Resistant Center Plate Assemblies

You’ll find the center plate assemblies employ forged low-profile designs paired with high-strength monolithic castings to maximize corrosion resistance while maintaining structural integrity. The integration of nylon wear liners between the center plates provides superior cold flow resistance and dramatically reduces wear in these critical interface zones. CNC-machined flame-hardened surfaces and welded reliefs work together as a thorough protection system, ensuring long-term durability in harsh operating conditions. The center plate’s Vicat softening temperature of 210°C ensures exceptional thermal stability during extended operation.

Material Selection Benefits

When designing corrosion-resistant center plate assemblies, material selection plays a critical role in maximizing operational longevity and structural integrity. You’ll find that aluminum alloys offer an excellent balance of lightweight strength and environmental corrosion resistance, while brass and bronze components provide enhanced durability in high-stress areas. The material properties of centrifugal-cast iron linings guarantee uniform wear resistance in critical applications.

Material Selection Benefits

Your manufacturing processes should incorporate precision casting methods like centrifugal casting and lost-wax bronzing to enhance structural integrity. Consider implementing hydro-fused solvent-free processes for gaskets to minimize material porosity. For superior performance, you’ll want to utilize low-expansion 400-series stainless steel in areas exposed to extreme heat, combined with crush-resistant designs that maintain structural integrity under compressive stress.

Multiple-Layer Protection Systems

Building upon proven material selections, multiple-layer protection systems incorporate advanced coating technologies that shield center plate assemblies from environmental degradation. You’ll find that these multi-layer materials create robust barriers against moisture, chemicals, and abrasive elements that typically accelerate wear in locomotive frames. Similar to the early diesel-electric railcars developed across multiple countries, these protection systems demonstrate global engineering excellence.

Multiple-Layer Protection Systems

The shielding effectiveness stems from strategically layered composites – each performing specific protective functions. Your center plate assembly’s first layer provides chemical resistance, while subsequent layers deliver mechanical protection and EMI shielding. This systematic approach guarantees thorough defense against multiple failure modes. When you’re specifying protection systems, focus on the compatibility between layers and their collective performance under dynamic loads. The system’s durability directly correlates to proper layer sequencing and thickness optimization across all protective zones.

Reinforced End Frame Structures

Modern diesel locomotive end frames require sophisticated reinforcement strategies to withstand extreme operational forces. You’ll find welded steel box construction distributes impact forces across critical zones while anti-climber reinforcements strengthen front and rear sections to prevent frame intrusion during incidents.

Reinforced End Frame Structures

This design approach evolved from earlier cast steel beds that revolutionized frame durability in steam locomotives. To maximize structural integrity, you’ll want to implement triangular tie rods in your bogie design – they’ll stabilize wheelsets and reduce rotational forces on end frames. For ideal reinforcement techniques, incorporate cast steel bedplates at load points and add reinforcing ribs at stress concentration areas like corners and suspension mounts. You’ll also need alignment-dedicated sleeves to maintain proper bogie positioning under thermal expansion.

Don’t forget to integrate load-attenuating intermediate mounts between the frame and superstructure – they’re essential for isolating mechanical strain. Your design should include hollow-section construction in truck frames to enhance strength-to-weight ratios while maintaining load capacity.

Impact-Absorbing Draft Gear Housing

You’ll find that steel draft gear housings deliver exceptional impact absorption through their optimized structural geometry and integrated mounting points. The housing’s reinforced design distributes coupling forces across multiple load-bearing surfaces while maintaining precise alignment with the locomotive frame. During operation, the draft gear cushions damaging forces by absorbing energy from pushing, pulling, starting, stopping, and coupling events. Your draft gear assembly achieves maximum effectiveness through strategically positioned mounting lugs that transfer impact energy into the main frame structure rather than concentrating stress at connection points.

Steel Absorption Design Benefits

Three critical design aspects define the impact-absorbing capabilities of modern draft gear housing: material composition, energy dissipation mechanisms, and structural geometry. You’ll find that high-strength stainless steels like 1.4318 (301LN) optimize these aspects through controlled grain structures and enhanced impact resistance materials.

Steel Absorption Design Benefits

The energy dissipation strategies incorporate tempered steel’s high yield strength (up to 1300 MPa), allowing controlled deformation without catastrophic failure. You can achieve superior shock absorption through strategically designed load paths that redistribute impact forces. Similar to how dynamic braking systems dissipate energy in locomotives, the duplex stainless steel composition delivers both strength and corrosion resistance, while maintaining dimensional stability under cyclic loads. This combination creates a housing that’s 30% lighter than traditional designs yet offers improved durability through advanced metallurgical properties and optimized stress distribution patterns.

Load Distribution Mounting Points

Building upon the advanced steel composition principles, load distribution mounting points form the backbone of impact-absorbing draft gear housing systems. You’ll find that dynamic load balancing relies on redundant mounting configurations and structural reinforcement techniques to prevent single-point failures during extreme impacts. The energy absorption capabilities help protect railcars during coupling and train operation.

Load Distribution Mounting Points
Mounting FeaturePerformance Characteristic
Center Sill PocketStationary compression stability
Draft LugsFront/rear force distribution
TORQUE FrameworkEnhanced torsional rigidity
Closed-Loop SystemReal-time load adjustment

The implementation of self-aligning clutch mechanisms maintains consistent follower-block contact, while integrated polyurethane elements supplement traditional steel components. Your draft gear’s modular housing design enables quick configuration changes to match specific load profiles, with standardized metrology protocols ensuring proper alignment and distribution consistency across mounting points.

Galvanized Steel Structural Gussets

durable metal support brackets

Galvanized steel structural gussets serve as critical reinforcement components in diesel locomotive frames, incorporating A36 steel with a 36 ksi yield strength and specialized hot-dip galvanization for corrosion resistance. Your gusset design should integrate 30° chamfered edges to minimize stress concentrations, proven to extend crack-free service life by up to 15 times. The structural integrity of these components relies on enhanced weld placement and strategic load distribution across underframe connections.

  • Custom-sized configurations accommodate varying load requirements, from triangular bracing to rectangular multi-directional support
  • Hot-rolled steel selection guarantees maximum malleability and freedom from internal stresses during manufacturing
  • Integration with T-beam retrofits delivers 11-15% stress reduction in critical areas

You’ll find these gussets particularly effective at managing stresses below 20 ksi while providing secondary support for bent or rolled underframe conditions. Their galvanized coating guarantees lasting performance in harsh outdoor environments.

Load-Distributing Traction Motor Mounts

Professional locomotive motor mount design integrates specialized polyurethane and rubber compounds to distribute traction loads effectively across the underframe assembly. You’ll need to select mounts with appropriate durometer ratings that balance vibration damping against shear load resistance. Polyurethane mounts offer 4x longer lifespan and superior chemical resistance compared to standard rubber variants.

Load-Distributing Traction Motor Mounts

When implementing vibration optimization techniques, guarantee your mounts properly align with stringers and maintain perpendicular stud orientation. You’ll achieve peak performance using Grade 8.8 steel bolts torqued to specification, while incorporating non-compressible shims for precise angular adjustments. Mount alignment strategies must account for both longitudinal and transverse forces, particularly in high-stress areas where traction motors transfer power to the wheels. Monitor material compression regularly and look for witness marks on fasteners to detect early signs of mount deterioration or loosening that could compromise your locomotive’s operational stability.

Stress-Tested Weld Joint Reinforcements

weld joint strength evaluation

While traditional welding methods remain commonplace, inertia friction welding (IFW) delivers superior joint reinforcement for locomotive frame components through its controlled thermal-mechanical process. You’ll find enhanced weld joint integrity through IFW’s refined microstructure, featuring granular bainite and acicular ferrite that boost both strength and fatigue resistance. The automated process eliminates human variability while achieving mechanical properties that closely match S355 base metal performance.

  • Maintains 87.5% yield strength and 100% tensile strength compared to base material, ensuring structural reliability
  • Delivers exceptional low-temperature toughness at -40°C, surpassing base metal performance in harsh conditions
  • Exhibits high ductility confirmed through 180° three-point bend testing without crack formation

When repairs become necessary, you’ll need to implement specialized GMAW techniques with precise parameters (270A, 28V, 30 cm/min). While repair welds show increased hardness, you’ll notice reduced impact absorption compared to original IFW joints.

Modular Frame-to-Body Connection Points

Four critical connection points secure the locomotive body to its underlying frame structure through an advanced modular integration system. You’ll find the design maximizes operational flexibility while maintaining rigid structural integrity through strategically placed rubber compression springs and helical coil supports.

Modular Frame-to-Body Connection Points
Connection TypeDesign Benefits
Rubber SpringsVertical load dampening
Helical CoilsAxle load equalization
Tapered PinsPivot point security
Floating PivotForce isolation

The modular connection advantages become apparent in the secondary stage suspension, where you’re able to implement flexible design options based on specific operational requirements. Your frame-to-body interface utilizes tapered pin connections at the bolster tunnel’s lower ends, ensuring secure center pivot assembly anchorage. This configuration effectively isolates traction and braking forces from vertical load paths, considerably reducing structural stress during operation while maintaining ideal load distribution across all connection points.

Wear-Resistant Bearing Support Brackets

durable bearing support brackets

Modern wear-resistant bearing support brackets incorporate advanced thermoplastic liners composed of 33.3% DuPont Zytel® 101 and 66.6% Zytel® ST801® resins for superior abrasion resistance. You’ll find these bearing materials paired with polyurethane inserts like Pellethane 21-90 AE® that deliver enhanced impact absorption compared to traditional nylon components.

The bracket design features channel-shaped liner units with precise integration points:

  • T-shaped nuts with undersized bosses create interlocking friction connections
  • Keyed grooves with dove-tail edges guarantee exact alignment during installation
  • Load-compensating inserts automatically adjust to minimize bearing surface gaps

You can expect peak performance through torque-sensitive fasteners that break at 70 ft-lbs ±5, preventing over-tightening while maintaining secure mounting. The system’s moisture-repelling compounds and corrosion-resistant fasteners protect against environmental degradation, while asymmetric insert configurations allow for easy retrofitting to existing wear-damaged brackets.

You may also like to read – The Importance of Regular Maintenance for Diesel Locomotive Parts

Frequently Asked Questions

How Does Extreme Temperature Cycling Affect Locomotive Frame Longevity?

Like a relentless hammer, extreme temperature cycling batters your locomotive frame’s structural integrity. You’ll observe accelerated frame fatigue as thermal cycles induce microstructural destabilization, with creep rates climbing to 20 × 10⁻⁴ h⁻¹. Temperature effects trigger γ/γ’ phase inversion, while accumulated cyclic strain forms micro-cracks. You’re facing shortened component lifespans due to thermal shock sensitivity and oxidative degradation in stress-concentrated areas.

Can Frame Components Be Upgraded to Accommodate Higher Horsepower Engines?

You’ll need strategic frame reinforcement techniques to handle increased horsepower loads. Start by implementing 30° chamfered gussets to reduce stress by 60-65% and add T-beam reinforcements for an additional 11-15% strength gain. Consider engine compatibility considerations like mount alignment and load distribution. You can integrate shortened fuel tanks to minimize bending forces and pair them with MD1 gusset modifications for ideal stress management.

What Role Do Frame Harmonics Play in Component Wear?

Frame vibration creates cyclical stress patterns that greatly impact your component longevity. You’ll observe accelerated wear patterns when natural frequencies align with operational harmonics, especially in the 360-370Hz range. Your components experience non-linear frictional effects that intensify at resonance points, leading to concentrated material degradation. Critical frequencies trigger stress concentrations, while modal interactions amplify wear through mass participation factors.

How Often Should Ultrasonic Testing Be Performed on Critical Frame Welds?

You’ll need to conduct ultrasonic testing on critical frame welds at specific intervals: every 5,000 service hours for high-stress zones, annually during scheduled maintenance, and immediately after any repairs or modifications. Follow weld inspection frequency guidelines from AWS structural codes and ASNT standards. Increase testing periodicity for welds with previous defects or those exposed to severe operational conditions. Always document results for compliance tracking.

Are Composite Materials Suitable for Replacing Traditional Steel Frame Components?

While composites offer impressive advantages like weight reduction and corrosion resistance, they’re not yet suitable for primary locomotive frame components. You’ll find their load-bearing capabilities don’t match steel’s proven structural performance under cyclical stresses. Current composite applications remain limited to non-structural elements, as technical barriers in dynamic loading, fire safety, and standardization must be overcome before they can reliably replace traditional steel frame structures.

What Causes Steam Locomotive Engine Frame Fatigue Failures?

What Causes Steam Locomotive Engine Frame Fatigue Failures?

Steam locomotives are marvels of engineering, but their frames are susceptible to fatigue failures that can lead to catastrophic consequences. Understanding what causes these failures is crucial for preserving the safety and integrity of these iconic machines. As mechanical structures endure repeated stress, the phenomenon of fatigue becomes increasingly relevant.

Fatigue in engineering refers to the progressive and localized structural damage that occurs when a material is subjected to cyclic loading. Studying fatigue is essential for locomotive safety, as failures can compromise the entire operational capability of these historic engines. This article will explore the various aspects of fatigue, including its types, mechanisms, and contributing factors.

What Causes Steam Locomotive Engine Frame Fatigue Failures?

From high cycle fatigue to the impacts of environmental influences, a multitude of elements contribute to frame fatigue failures in steam locomotives. Additionally, the role of pre-existing flaws and the significance of rigorous maintenance practices will be examined. Join us in uncovering the complex world of steam locomotive frame fatigue and the lessons that can be learned to enhance their enduring legacy.

Understanding Fatigue in Mechanical Structures

Fatigue in Engineering

Fatigue in engineering refers to the gradual initiation and growth of cracks in a material due to repeated loading. This cyclic stress eventually leads to the failure of the component. When a fatigue crack starts, it slowly advances with each load cycle. This process leaves tell-tale marks, called striations, on fracture surfaces. As the crack grows, it can reach a critical size. At this point, the crack causes rapid failure because the stress applied exceeds the material’s toughness.

Several materials can suffer from fatigue, not just metals. Composites, plastics, and even ceramics can also experience fatigue failures. Historically, metal railway axles were among the first components where fatigue was studied. In the nineteenth century, it was mistakenly thought metal crystallization was the reason for these failures. This idea, however, has since been disproven.

Importance of Studying Fatigue for Locomotive Safety

Understanding fatigue in locomotive components is vital to maintain safety. In history, fatigue failures have led to tragic events, such as the Versailles train wreck. This disaster resulted from a locomotive axle failure due to fatigue. The Britannia class locomotives also suffered from fatigue cracking after extended use. This highlighted the urgent need for better engineering solutions.

Importance of Studying Fatigue for Locomotive Safety

Mitigating fatigue failures requires identifying stress risers, like those found near horn guides. Advanced methods, such as Finite Element Analysis (FEA), shed light on fatigue failure mechanisms. FEA, combined with experimental checks, helps improve the safety of locomotive components.

Additionally, maintenance regulations and crew responsibilities play key roles in preventing fatigue-related accidents. Fatigue management in both locomotives and their operators can significantly enhance rail operation safety.

Overall, these insights and techniques are critical to ensuring steam locomotives continue to operate safely and efficiently.

Definition of fatigue in engineering

Fatigue in engineering is the development of cracks in materials due to repeated stress over time. These cracks grow a little with each load cycle. Eventually, they lead to failure of the part. The process starts when a tiny crack appears. This crack keeps getting bigger with each cycle, forming lines called striations.

Definition of Fatigue in Engineering

Here’s how fatigue works:

  1. Initiation: A small crack forms due to stress.
  2. Propagation: The crack grows with each load cycle.
  3. Critical Size: Once the crack reaches a certain size, rapid failure occurs.

Fatigue was first noticed in metal parts like railway axles in the 1800s. It was wrongly thought to be caused by metal crystallization. Later, it was found that not just metals, but also composites, plastics, and ceramics can suffer from fatigue.

Key PointsDescription
Crack InitiationStarts small due to stress.
Crack PropagationGrows with every loading cycle.
Critical FailureOccurs when crack size becomes critical.

This understanding helps us design stronger and more durable materials. It is crucial across various industries, including steam locomotives and boilers.

Types of Fatigue Failures

Steam locomotives rely on strong engine frames, but these frames can suffer from fatigue failures. These failures occur due to repeated loading and stress on the frame. Recognizing the different types of fatigue is crucial in understanding how to prevent them.

Types of Fatigue Failures

High Cycle Fatigue

High cycle fatigue occurs due to many cycles of loading at lower stress levels. It is common in steam locomotives, as their components face constant mechanical stresses. This type of fatigue can cause cracks to form, especially if the design has flaws that create stress concentrations. Preventive measures include:

  • Regular non-destructive testing (NDT)
  • Use of comprehensive analysis methods, such as finite element analysis (FEA)
  • Monitoring of components subjected to cyclic loading

Low Cycle Fatigue

Low cycle fatigue happens at higher stress levels but with fewer cycles. This often results from repeated large stresses, like those caused by the temperature changes in steam locomotive boilers. Factors affecting low cycle fatigue include:

  • Stress concentrations at geometric discontinuities or corroded sections
  • Stress risers, such as notches or sharp corners
  • Heavy temperature cycling in boilers

Preventive strategies focus on effective thermal management and addressing potential stress concentrations during design.

Extremely Low-Cycle Fatigue

Extremely low-cycle fatigue stands out because it occurs in less than 10,000 cycles, often due to high stress and strain. This can lead to localized plastic behavior in metals. It’s typically evaluated using strain-based parameters. Key points include:

  • Plastic strain amplitude is related to failure cycles using the Coffin-Manson relationship
  • Testing is conducted at constant strain amplitudes with low frequencies (0.01 to 5 Hz)
  • Behavioral patterns are often represented in a log-log scale, showcasing predictable fatigue life

To handle this type of fatigue, structural conditions need thorough examination, especially under various load scenarios like earthquakes. This helps establish proper fatigue strength and deformability curves.

In summary, understanding these fatigue types is key to maintaining steam locomotives. Consistent maintenance and expert operation can help avoid mechanical failures, safeguarding both the locomotives and their operators.

Mechanisms of Fatigue Damage

Fatigue damage in steam locomotive frames arises from cyclic stress factors. This damage often starts at points with high stress, such as slip bands, inclusions, or porosities. The first phase involves crack nucleation, typically occurring at shear planes on the material’s surface or within its grains.

As cracks grow, they spread perpendicular to areas of high tensile stress. The presence of stress concentrations can speed up fatigue failures, as seen in historical broken locomotive axles.

Overview of Fatigue Damage Mechanisms

Fatigue damage develops through four stages: crack nucleation, short crack growth, long crack growth, and separation. This process is usually due to cyclic loads on components. Early studies focused on how stress concentrations in railroad axles lead to significant accidents. Identifying origins, like keyways in axles, highlights the importance of design improvements. Modern approaches use Finite Element Analysis (FEA) with experiments to predict fatigue failures.

Overview of Fatigue Damage Mechanisms

Role of S-N Curves in Fatigue Analysis

The S-N curve is crucial in understanding how stress affects fatigue life. It shows the relationship between stress levels (S) and cycles to failure (N). As stress increases, the number of cycles to failure decreases. The linear part is described by the Baskin equation, connecting stress amplitude to cycles. A significant aspect of the S-N curve is the fatigue limit, under which materials like plain carbon steels endure cyclic stress without failure.

Role of S-N Curves in Fatigue Analysis

Importance of Fracture Mechanics

Fracture mechanics is key to unraveling fatigue initiations and propagation in engineered parts, including steam locomotive engines. Historical incidents, such as the Versailles train accident, led to scientific research on material failures. Advances in metallurgy reveal fatigue crack initiators, like pores, crucial to addressing failures. Fracture mechanics models use statistics to predict fatigue performance accurately. Understanding that most failures stem from pre-existing faults necessitates design modifications to improve reliability.

Factors Contributing to Frame Fatigue Failures

Steam locomotive engines are powerful but face certain challenges over time. Frame fatigue failures can occur due to a variety of factors. Stress risers, such as the corners of square holes and deep notches, are common culprits. These features significantly increase the risk of fatigue failures. Additionally, corrosion weakens areas of the frame, making it more susceptible to fatigue cracking.

This is especially evident in steam locomotives like the Britannia class, where cracks often appear above rear bogie wheels and around horn guide brackets after extensive use. Design improvements, like the use of cast steel stretchers in Clan locomotives, help support these vulnerable areas. To reduce fatigue stress, some locomotives use techniques such as gradual heating and cooling periods during operation.

Material Properties and Composition

The materials used in steam locomotive components play a crucial role in their durability. The tensile strength of boiler steels increases up to about 500°F but drops sharply at around 1000°F. This temperature range is critical for maintaining material integrity. Crown sheet failures occur due to a loss of tensile strength as the temperature rises.

Stress risers also contribute to early fatigue failures in locomotive materials. While normal boilers can undergo repairs without concern for major property changes, alloy materials require careful handling. Heavy temperature cycling can exacerbate fatigue stresses. Thus, lengthening operational heating and cooling periods can mitigate these effects.

Material Properties and Composition

Stress Concentrations and Load Variations

Stress concentrations are significant factors in fatigue failures. Corners of square holes and deep notches focus stress in a small area, leading to early failures. Corroded areas increase stress concentration zones, which may lead to cracks. In stage I of fatigue, cracks begin and expand along crystallographic planes, but they quickly propagate under higher stress levels in stage II. The presence of persistent slip bands (PSBs) in metals can localize stress, potentially forming cracks. Hence, monitoring cyclic loads is essential. Additionally, during maintenance, applying heat to alloy boilers may change material properties, creating new stress concentrations.

Stress Concentrations and Load Variations

Environmental Influences on Fatigue

The environment has a significant impact on steam locomotive fatigue. Corrosion accelerates the deterioration of components, reducing their lifespan. The presence of notches and stress points in designs can lead to more frequent fatigue failures. Cyclic loading, a result of operational stresses, makes materials fail at much lower stress levels than their ultimate strength.

Environmental Influences on Fatigue

Temperature variations during use cause thermal cycling, which weakens material structures over time. Residual stresses also play a role; tensile residual stresses can lower fatigue life, while compressive residual stresses can enhance it. Proper treatment of materials can improve their fatigue performance, extending the life of steam locomotive components.

Pre-existing Flaws and Their Impact

Steam locomotive engine frames can suffer from fatigue failures due to pre-existing flaws. These flaws often appear in stress concentration areas such as above the rear bogie wheels and around slide bar brackets. When locomotives, like the Britannia class, accumulate significant mileage (about 438,000 miles), these areas may develop fatigue cracks.

Additionally, incorrect or malfunctioning parts, such as injector disks and check valves, can signal maintenance or design flaws. These pre-existing issues can contribute to fatigue failures over time. A lack of expertise in locomotive maintenance further exacerbates these risks. Improper repairs and recurring maintenance problems often highlight this deficiency. Critical flaws such as stress raisers in poorly designed parts, like horn guides, can play a significant role in fatigue crack initiation and propagation.

Definition and Types of Flaws (e.g., Bifilms)

Material flaws like bifilms are a common cause of fatigue failures. Bifilms are defects that may appear as bubbles or pores within the material structure. During the casting process, issues like shrinkage can introduce these bifilms. Bifilms are often visible as pores but may also remain as closed cracks within the material. The presence of oxide films on these surfaces can indicate such defects.

Definition and Types of Flaws

Bifilms can significantly reduce the fatigue resistance of engineering components. Research shows that these defects often originate from manufacturing processes rather than from fatigue crack growth alone. Understanding the relationship between bifilms and fatigue performance is crucial. Quality assurance and inspection during manufacturing are vital to prevent fatigue-related failures.

How Flaws Initiate Fatigue Cracks

Fatigue cracks often start at stress concentration points where repeated loading occurs, such as in locomotive axles. Many investigations have shown that these cracks result from overlooked fatigue mechanisms. Microstructural defects like non-metallic inclusions and small flaws heavily impact crack initiation.

How Flaws Initiate Fatigue Cracks

This situation affects material durability under cyclic loads. Experimentation and fracture mechanics simulations demonstrate a clear correlation between initial flaws and crack growth. As observed in tests, fatigue crack propagation accelerates under cyclic stress applications. This emphasizes how critical flaw initiation is to fatigue failure.

Case Studies of Fatigue Failures from Defects

Historically, fatigue failures have caused significant accidents in railway history. In 1837, Wilhelm Albert pioneered the study of fatigue, followed by William John Macquorn Rankine in 1842. Rankine linked stress concentrations to the Versailles train wreck, noting a locomotive axle failure as a major contributor. Another case involved Joseph Glynn’s 1843 report highlighting a locomotive tender axle failure originating at a keyway.

Case Studies of Fatigue Failures from Defects

In 1848, the Railway Inspectorate noted a tire failure, suspecting a fatigue issue from a rivet hole. These examples stress the importance of design and manufacturing quality. Over time, cyclic stress leads to metal fatigue failures as microscopic damage develops into fractures. Comprehensive engineering and material assessments can prevent such catastrophic failures in locomotives.

Real-World Case Studies on Fatigue Failures

Fatigue failures can have serious consequences. One infamous incident was the Versailles train wreck. This accident happened because of fatigue failure in a locomotive axle. It highlighted the importance of stress concentrations in rail design for safety. Similarly, the Britannia class steam locomotives faced fatigue cracking after about 438,000 miles of use. The cracks appeared mainly in areas above the rear bogie wheels and around the slide bar brackets.

Another enlightening case study involved a turbine blade. Its fatigue failure led to a crash of a Cessna aircraft, demonstrating the consequences structural failures can have. Additionally, a Ti6Al4V alloy compressor impeller showed how stress concentrations at the blade root caused its breakdown. Similarly, AISI4140 steel U-bolts revealed that ignoring metallurgical parameters can lead to fatigue failure. Applying surface modification can enhance their durability under cyclic loads.

Analysis of notable steam locomotive failures

Steam locomotives have a history of fatigue failures. One issue is the use of alternating rows of straight-thread and button-head crown stays. These can cause gradual crownsheet failures. Such features, however, might prevent more dangerous failures that threaten safety. The Safety Board advises more research into these progressive failure features during repairs or rebuilding to improve safety. Poor maintenance is another concern.

Analysis of notable steam locomotive failures

Incorrect parts, like injector disks and leaking check valves, show the need for better safety protocols. This highlights a decline in specialized knowledge among owners and crews. The need for improved engineering to prevent fatigue is long recognized. Since the early 19th century, studies have sought to reduce stress concentrations in locomotive components to enhance safety.

Lessons learned from engineering failures

Engineering failures teach valuable lessons. Designing steam locomotives with alternating crown stays prioritizes progressive failure features. These can avert catastrophic boiler failures if low water conditions occur. Yet, maintenance issues like incorrect parts reveal a lack of specialized knowledge. This can lead to disastrous consequences. Fatigue failures are often unpredictable, occurring at stress levels below material strength.

Lessons learned from engineering failures

This underscores the need for careful analysis during both design and maintenance. Cyclic loading creates microscopic damage over time. These small fractures can suddenly become catastrophic structural failures. Alloy materials used in boilers are especially sensitive to temperature changes. This affects their propensity for failure, making them more vulnerable than traditional materials.

By studying these cases and lessons, engineers can develop stronger, safer steam locomotives and other mechanical systems.

Maintenance Practices to Mitigate Fatigue

Maintaining steam locomotives requires special attention to prevent engine frame fatigue failures. Proper maintenance involves a mix of design principles and regular checks. By adopting strategies that account for potential flaws and focusing on routine upkeep, the risk of fatigue failures can be significantly reduced.

Proper Installation of Components

Proper installation is crucial for the longevity of steam locomotive components. Each part must be aligned correctly and securely fastened. During assembly, components like pistons and connecting rods should fit within specified tolerances.

Proper Installation of Components

This means using precise tools such as calipers and torque wrenches to avoid under or over-tightening. Regular inspections should check for signs of wear, especially on surfaces where components interact closely. Ensuring components are aligned and within their designed parameters enhances the locomotive’s performance and reliability.

Importance of Quality Control Testing

Quality control testing is vital for the safe operation of steam locomotives. During testing, pressure and temperature checks help identify leaks and performance issues. Key components, such as pistons and piston rings, need regular examination to ensure proper sealing.

Importance of Quality Control Testing

This maintains efficient compression within the engine. A systematic maintenance schedule that includes bearing and connecting rod tests reduces friction and wear. Detailed documentation of test results is essential for spotting performance trends and planning necessary upgrades or replacements.

Regular Inspections and Preventive Measures

Regular inspections help catch problems early, preventing severe damage. Key areas to check include piston and piston ring integrity, bearing wear, and rod alignment. Establishing a clear maintenance schedule with thorough records helps track when parts need servicing. Both static and dynamic tests are important to ensure mechanical alignment and pressure integrity. By focusing on these testing aspects, potential leaks or misalignments can be addressed before they cause failure. Regular and well-documented checks are a crucial part of a preventive maintenance strategy.

Regular Inspections and Preventive Measures

In conclusion, steam locomotives can be significantly protected from engine frame fatigue failures through proper installation, rigorous quality testing, and regular inspections. By adhering to these maintenance practices, the longevity and safety of these magnificent machines can be preserved.

You may also like to read: Replace Locomotive Frame Cross Members: Step-by-Step Instructions

Replace Locomotive Frame Cross Members: Step-by-Step Instructions

Replace Locomotive Frame Cross Members: Step-by-Step Instructions

First, secure the work area and put on required PPE including hard hats and steel-toe boots. Install temporary supports using band iron to prevent frame racking, then remove old cross members by grinding out rivets and seized bolts. Clean mounting surfaces thoroughly with solvents and verify flatness. Install new cross members through side rail apertures, align them carefully, and torque bolts in the proper sequence. Following detailed specifications and industry standards will guarantee a safe, successful replacement.

Key Takeaways

  • Install temporary supports and X-bracing to prevent frame racking before removing old cross members and fasteners.
  • Clean mounting surfaces thoroughly using solvents and mechanical methods to remove rust, grease, and contaminants.
  • Elevate locomotive frame with rated jacks, align new cross members through side rails, and use mechanical stops during insertion.
  • Follow sequential bolt tightening patterns starting from center outward, initially torquing to 50-75% of target value.
  • Conduct quality control checks with feeler gauges, verify torque specifications, and test load distribution across frame assembly.

Safety Requirements and Equipment Setup

safety equipment setup guidelines

Before beginning any locomotive frame cross member replacement, you’ll need to establish detailed safety protocols and prepare the required equipment. Start by conducting a thorough risk assessment, focusing on load-bearing capacity and weight distribution. Document all locomotive identification details and apply non-compliance tags according to CFR standards.

Equip your team with essential PPE including hard hats, high-visibility vests, steel-toe boots, and hearing protection. You’ll need respiratory gear for dust exposure and fall protection harnesses for elevated work. Regular inspection helps prevent potential frame stability issues. Set up your equipment maintenance station with calibrated hydraulic jacks, alignment tools, and torque wrenches that meet manufacturer specifications. Install containment systems for debris management and position spill kits nearby.

Secure the work area by isolating surrounding components and establishing operational restrictions. Brief your crew on safety protocols and temporary speed limitations. Verify fire extinguishers are readily accessible and wind protection is in place before commencing work.

Frame Inspection and Damage Assessment

When inspecting a locomotive frame for cross member replacement, you’ll need to conduct a thorough structural assessment following FRA guidelines. Begin by checking for visible cracks in critical areas, paying special attention to plate connections and stress points around rivet holes. Document all findings on FRA Form No. 2.

Frame Inspection and Damage Assessment

To guarantee frame stability, measure component tolerances and inspect for loose or inoperative parts. Look for abnormal wear patterns and stress concentrations that could compromise the frame’s integrity. You’ll need to verify foundation ring stability and assess the connection points between cross members and the main frame. A daily inspection of tube ends and joints should be performed to identify any developing issues early.

Document all measurements and observed defects, including any cracks, separation, or excessive wear. For damage prevention, carefully evaluate wear patterns that might indicate structural fatigue or operational stress. Check for proper alignment and guarantee all components meet specified tolerances before proceeding with cross member replacement.

Removing Old Cross Members

dismantling outdated support beams

Securing the locomotive frame’s stability marks the first critical step in cross member removal. Install temporary supports using band iron or X-bracing to prevent frame racking, and maintain a central crossmember while removing others to preserve structural integrity. Successful restorations often rely on baseline frame measurements.

Begin old fastener techniques by grinding rivet heads carefully, then punch them out using a centered tool. For seized bolts, apply penetrating oil or heat treatment before removal. You’ll need impact wrenches for high-torque applications. Document thread specifications and keep removed fasteners for analysis.

Address structural integrity considerations by following a sequential disassembly approach. Remove adjacent components like exhaust and steering links first, then isolate subframe elements. Support heavy service points near bellhousings using engine supports. Install temporary reinforcements in critical areas, and continuously monitor frame geometry using diagonal measurements. Mark alignment points and photograph multi-fastener interfaces for precise reassembly reference.

Preparing Mounting Surfaces

You’ll need to thoroughly clean all mounting surfaces using appropriate solvents and abrasive methods to remove rust, debris, and contaminants before proceeding with installation. Using calibrated straightedges and levels, verify the flatness of each mounting surface to guarantee no warping or irregularities exist that could affect alignment. Mark reference points and document key measurements that you’ll use later to verify proper cross member positioning during final assembly. Maintaining the precise frame spacing is critical during replacement, so install temporary bolts to hold the proper distance between frame plates.

Clean and Inspect Surfaces

Proper surface preparation involves three critical cleaning stages before locomotive frame cross member replacement. First, you’ll need to remove heavy deposits using mechanical cleaning techniques with soft-bristle brushes, followed by petrochemical-based solvents for grease removal. Next, apply citrus-based solutions for stubborn scale, avoiding chlorinated cleaners that could damage metal surfaces.

Clean and Inspect Surfaces

Inspect your work thoroughly using both visual and tactile methods. You’ll want to examine surfaces under bright lighting with a 5x-10x magnifier to detect any micro-imperfections, pitting, or stress fractures. Test for proper surface preparation by checking reflectivity and water sheen. Document your findings with detailed photos for quality assurance, and remember to wear appropriate PPE including nitrile gloves, goggles, and breathing protection throughout the process. Since locomotive frames often feature flexible connections between components, pay special attention to cleaning these junction points where water pipes and feed lines attach.

Mark Reference Points

Establish precise reference points by carefully mapping key mounting surfaces before removing the existing cross members. You’ll need to guarantee structural integrity by marking locations where load-bearing components intersect with the frame. Start by identifying primary reference alignment points at axle positions and center pivot locations. Document critical measurements relating to load distribution patterns across the bogie frame. When marking positions, consider that three-point suspension configurations require specific geometric alignment for optimal weight distribution.

Mark Reference Points

Following safety protocols, create detailed marking templates that account for material specifications of both existing and replacement cross members. You’ll want to map out positions of mounting brackets, shear bolt locations, and anti-climber attachment points. Use permanent industrial markers to indicate centerlines and establish datum points for precise positioning. Double-check all measurements against manufacturer specifications before proceeding with removal procedures.

Installing New Cross Members

adding structural support beams

Begin the cross member installation by elevating the locomotive frame with rated jacks and securing it on safety stands. Check for MORryde suspensions and replace shoulder bolts with hex-head bolts if necessary. Verify that the cross member’s bottom edge aligns with frame hanger edges, ensuring open channels face downward.

Insert the cross members through the side rail apertures, using the larger inner dimensions (D1) to guide placement. Position mechanical stops to prevent over-insertion and maintain frame integrity. Replace original shoulder bolts with wet bolts facing inward, but don’t fully tighten yet. Connect cross member halves using 3/8-16 flange bolts, starting with the outermost holes.

Follow the proper tightening sequence: torque wet bolts to 40 ft-lbs before securing flange bolts. Install clamp straps inside frame hangers and torque to 15 ft-lbs. Verify alignment by checking engagement with apertures and testing load distribution across the frame.

Alignment and Torque Specifications

You’ll need to precisely align the cross members using factory-specific jig points while maintaining the specified “Z” and “D” trim height dimensions throughout the installation process. Following the manufacturer’s torque charts, apply sequential bolt tightening patterns using a calibrated torque wrench to achieve proper load distribution across mounting points. Validate your work by conducting measurements through inspection holes with custom gauges and perform visual checks before final torque application. Utilizing a chain and turn-buckle setup helps pull the cross member forward to achieve proper alignment position.

Essential Alignment Steps

Precise alignment of locomotive frame cross members demands a systematic approach beginning with rough alignment to within 20-30 mils vertical and horizontal tolerance. You’ll need to employ concentric tube-through-tube joints with differentially sized apertures to reduce coaxial alignment criticality.

Essential Alignment Steps

Apply alignment techniques sequentially, starting with cross member insertion from one side rail to the opposite. Use feeler gauges in 0.002″ increments to detect subtle angular misalignments during the tightening phase. Check symmetry across rails to confirm proportional adjustments. For soft foot conditions, insert split shims under attachment points to correct angular misalignments. Crosshead shoes are critical wear components that require regular inspection during frame alignment.

Verify alignment using alignment tools such as dial bore gauges for final confirmation. Maintain baseline positioning during torque calibration to prevent reintroducing misalignment issues.

Proper Torque Sequences

When installing locomotive frame cross members, following the correct torque sequence is critical for maintaining proper alignment and preventing stress concentrations. Begin your torque calculations at the center cross members and work outward, using calibrated torque tools to achieve specified values. If you hear creaking from the middle, double-check the torque specifications to ensure proper tightening.

LocationTorque RangeTool Required
Front (#4)25-34 lb-ftTorque Wrench
Middle (#2,#3)44-70 lb-ftImpact/Torque
Rear (#6,#7)44-70 lb-ftImpact/Torque
#1 Nuts139-141 lb-ftTorque Wrench
Proper Torque Sequences

Apply 50-75% of target torque initially to verify fitment. Alternate between adjacent cross members while tightening to guarantee even load distribution. Confirm proper contact between cross members and frame rails before applying final torque. Re-verify all connections after complete assembly to account for frame flex during installation.

Validation and Adjustment Protocol

To guarantee ideal frame cross member installation, thorough validation protocols must be implemented through a series of systematic checks and adjustments. You’ll need to verify alignment using suspension component checks and geometric surveys while ensuring torque specifications comply with standardized limits. Apply validation techniques including FE modeling and simulation-to-measurement comparisons to confirm structural integrity.

Validation and Adjustment Protocol

Document all validation data with clear visual charts to effectively communicate findings to stakeholders. Execute adjustment strategies through parametric sensitivity analysis, modulating torque values based on material specifications. Document all measurements against EN 14363 criteria during constant-radius track sections. You must calibrate instrumentation against track profiles and conduct post-change surveys to verify frame tolerances. Complete your validation by performing dynamic crash simulations and conducting multi-stage impact evaluations to confirm assembly resilience. Remember to maintain detailed records of all adjustments and test results.

Quality Control Checks

Quality control during locomotive frame cross member replacement involves five critical inspection phases: material verification, machining validation, dimensional checks, structural testing, and manufacturing standards compliance.

For proper material certification, you’ll need to verify steel grades meet AAR standards through tension and compression testing. Make sure machining tolerances align with CNC calibration requirements and validate tool wear patterns to maintain dimensional accuracy.

Quality Control Checks

Key quality control steps include:

  1. Measure all critical dimensions using a CMM against CAD blueprints
  2. Conduct magnetic particle testing on weld joints to detect subsurface defects
  3. Verify attachment points under cyclic loading for excessive play

Use Go-NoGo gauges to check mounting flange clearances and precision micrometers for joint gaps. Don’t forget to inspect cold-form radii with calibrated gauges and confirm diagonal alignment using laser triangulation. Monitor supplier NDT procedures and maintain records of heat treatment processes for full compliance with AAR M-214 standards.

Testing and Documentation

evaluation and record keeping process

Following locomotive frame cross member replacement, thorough testing and documentation protocols must be implemented to guarantee operational safety and regulatory compliance. You’ll need to perform static load testing to verify structural integrity and dynamic load testing to assess performance under operational stresses. Document all test results using standardized reporting formats that comply with FRA requirements.

Implement extensive Testing Protocols including finite element analysis (FEA) simulations and non-destructive testing methods to validate the installation. You must conduct material verification checks and maintain detailed records of all certifications and test data. Documentation Practices should include photographic evidence, measurement logs, and complete test reports.

Create a detailed audit trail covering pre-testing preparations, testing procedures, and post-testing results. You’ll need to maintain these records for the locomotive’s service life, ensuring traceability and compliance with regulatory standards during future inspections or maintenance activities.

Frequently Asked Questions

How Long Can a Locomotive Operate With Damaged Cross Members?

Like a spider web with a broken strand, even minor frame damage compromises a locomotive’s entire structural integrity. You can’t operate a locomotive with damaged cross members – it’s an immediate “out of service” situation. FRA regulations and operational limits require you to halt service the moment you discover cross member damage through penetration, separation, or severe corrosion that could affect safe operation.

What Causes Premature Wear in Locomotive Frame Cross Members?

You’ll find several key wear factors affecting locomotive frame cross members. Dynamic imbalances from improper counterweighting create excessive vibration, while oscillating valve gear stress leads to metal fatigue. Poor maintenance practices, including inadequate lubrication and delayed bearing replacement, accelerate deterioration. High-speed operations amplify these issues, especially when combined with oversized side rods and crank pins that transfer damaging forces through the frame structure.

Can Different Manufacturers’ Cross Members Be Used as Replacements?

You’ll need to carefully evaluate cross member compatibility before using parts from different manufacturers. Always verify that replacement components meet original manufacturer specifications for material grade, dimensions, and load ratings. While some aftermarket cross members may physically fit, they could have different stress tolerances or metallurgical properties. Check technical documentation and consult the OEM to guarantee replacements won’t compromise structural integrity or safety compliance.

How Often Should Cross Members Be Inspected During Regular Maintenance?

You’ll need to inspect cross members every 92 days maximum as part of your periodic maintenance checklist. Don’t exceed this inspection frequency, even if the locomotive appears to be running well. During daily visual checks, you must examine cross members for cracks, deformities, and corrosion. If you spot any structural issues or asymmetrical wear, remove the locomotive from service immediately for further evaluation.

What Are Signs That Cross Members Need Immediate Replacement?

Like a house of cards about to collapse, compromised cross members demand your immediate attention. You’ll need to replace them when you spot visible through-holes, significant rust perforation, or cracks that threaten structural integrity. Watch for loud clunking noises during operation, persistent misalignment issues, and cross member wear exceeding 50% of material thickness. Don’t ignore sagging frames or loose mounting hardware that could compromise safety.

Steam Engine Cylinder Block Care: Expert Service Guide

Steam Engine Cylinder Block Care: Expert Service Guide

To maintain your steam engine cylinder block, you’ll need to follow five critical protocols: clean with specialized solvents and high-pressure washing every 500 cycles, verify alignment using digital readouts and dial indicators, inspect steam passages with ultrasonic testing at 20-100kHz, conduct valve maintenance every 2-3 hours with high-temp steam oil, and perform regular leak-down testing. Mastering these fundamental service procedures will release your engine’s full potential.

Key Takeaways

  • Clean cylinder blocks thoroughly using high-pressure washing and specialized solvents to remove debris, followed by complete drying and corrosion protection.
  • Perform regular inspections using ultrasonic testing and infrared thermography to detect steam passage blockages, leaks, and wear patterns.
  • Maintain proper alignment during installation by using center studs and following cross-corner tightening sequences for optimal cylinder block positioning.
  • Lubricate valve systems every 2-3 hours with high-temperature steam oil and inspect valve settings, timing, and seals every 500 cycles.
  • Document all maintenance activities and conduct systematic performance testing to track efficiency, leakage rates, and pressure metrics over time.

Essential Tools and Safety Protocols

safety tools and protocols

Precision tools and proper safety protocols form the foundation of steam engine cylinder block maintenance. You’ll need essential equipment including a Scotchbrite deburring wheel, Cratex block, and specialized honing tools with appropriate oils. For accurate measurements, utilize a coaxial bore gauge to verify cylinder dimensions and alignment.

When implementing deburring techniques, use designated knives to remove sharp edges from newly machined surfaces. Your honing practices must include thorough oil application and subsequent cleaning with solvents to prevent rust formation. Always verify oil passages and ports are clear of obstructions before assembly. Achieving a professional finish requires a Keith Appleton method for precise cylinder alignment and squaring.

Secure critical components like oil squirter nozzles and dipsticks with Loctite Green locking agent. Use compressed air to remove machining debris, and maintain strict cleanliness standards throughout the process. For safety compliance, properly dispose of contaminated honing oils and guarantee all pressure vessel components meet specifications before final assembly.

Cylinder Block Construction Standards

Building upon proper tool selection and safety protocols, your cylinder block construction must meet rigorous material and design standards. Grey iron casting serves as the primary cylinder material, enabling dry running capabilities while preventing unwanted condensation. You’ll need to verify the casting incorporates core holes for effective steam jacketing throughout the block. Cast iron blocks are machined first between frames before painting for optimal fitting and alignment.

Cylinder Block Construction Standards

Your block’s design must feature integrated thermal insulation and exposed valve chest exteriors to maximize heat transfer efficiency. When selecting cylinder materials, specify BMS material for exhaust steam pathways and implement a cruciform transfer conduit with embedded steam pipes. These casting techniques support ideal steam temperature maintenance through wide, flat supply conduits that maximize heat exposure surface area. The construction should include a thorough condensate drainage system to manage moisture effectively. Your block’s steam jacketing system must maintain consistent cylinder temperatures near boiler levels for peak operational efficiency.

Steam Passage Inspection Methods

steam passage inspection techniques

You’ll need both ultrasonic testing and infrared thermography to properly assess steam passage conditions within cylinder blocks. When examining internal flow paths, use ultrasonic measurements to detect any restrictions or blockages that show >2× baseline dB readings at key junctions. For steam port wear evaluation, combine thermal imaging with high-emissivity targets to identify any temperature anomalies that could indicate leakage or degradation of port surfaces. This inspection approach aligns with proven practices for steam system reliability monitoring.

Internal Flow Path Analysis

Internal flow path analysis forms the cornerstone of effective steam engine cylinder maintenance, requiring systematic inspection of steam passages through multiple diagnostic methods. Your inspection strategy must integrate computational modeling with hands-on diagnostic techniques to achieve ideal flow optimization. Accurate calculation of off-design operating modes helps prevent damage to critical flow path components.

Internal Flow Path Analysis
  • Deploy pressure mapping sensors at strategic points to monitor steam distribution patterns and identify potential flow restrictions
  • Utilize advanced CFD modeling to analyze steam passage efficiency, focusing on areas prone to thermal stress
  • Conduct regular structural integrity checks of downcomer and evaporator regions using specialized borescope equipment
  • Implement precision machining quality controls during passage repairs, maintaining strict dimensional tolerances

To maximize inspection effectiveness, combine these methods with detailed documentation of flow characteristics and thermal patterns. This integrated approach guarantees thorough analysis of your cylinder block’s internal flow dynamics.

Steam Port Wear Detection

While steam engine maintenance demands numerous inspection protocols, steam port wear detection requires a systematic multi-method approach combining visual, thermal, and acoustic diagnostics. You’ll need to check for key wear indicators like surface erosion, carbon deposits, and thermal discoloration around valve seats and ports. Regular testing with specialized ultrasonic instruments provides more accurate diagnostics than traditional methods.

Steam Port Wear Detection

Begin your inspection frequency with ultrasonic testing at 20-100kHz to detect steam leaks and flow turbulence. Use infrared imaging to identify cold spots and thermal gradients across port surfaces. Monitor resonance frequencies to evaluate valve seating efficiency and expansion passage reflections. Compare volumetric efficiency against benchmarks by measuring pressure drops and cycle-dependent flow rates. Document port alignment and sealing clearances, paying special attention to cylinder-to-port mating surfaces where wear commonly occurs.

Alignment and Fitment Procedures

You’ll need to begin alignment by centering key components using edge finders and digital readouts to establish precise reference points accurate to within 0.001″. For ideal component stability, you must follow a specific cross-corner tightening sequence when securing the cylinder block, starting at 30% of final torque before progressing to full specification. Your machining accuracy depends on maintaining parallel and perpendicular relationships between reference surfaces, so verify these using dial indicators during both initial setup and final assembly. Installing the four center studs first ensures proper positioning of the cylinder block before adding remaining fasteners.

Precision Centering Methods

Achieving precise centering in steam engine cylinder blocks requires a systematic approach using specialized fixtures and measurement systems. For precision alignment, you’ll need to employ cradle fixtures to position blocks square and upright while ensuring fixture calibration against established datum points.

Precision Centering Methods

Using sharp steel tools and making light cuts will help maintain accuracy during cylinder boring operations. Key steps for accurate centering include:

  • Use DROs to establish exact XY coordinates for drilling and tapping operations
  • Verify positioning with edge finders zeroed to datum surfaces
  • Align slot drills to scribed reference lines for midpoint confirmation
  • Employ digital tools to check depths during single-pass machining

When working with angled ports, set your adjustable vise to the specified angle and use marked center lines as guides. Deploy compensation fixtures like box plates to maintain consistent hole positioning references throughout the machining process.

Securing Component Stability

Since proper component stability directly impacts engine performance, securing accurate alignment requires a methodical approach starting with the center studs. You’ll need to install four center studs first, which serve as your primary reference points for precise cylinder block positioning. This essential sequence guarantees optimal component durability and enhanced vibration resistance during operation. Using cast iron liners helps ensure proper thermal properties during cylinder block assembly.

Next, you’ll carefully slip the cylinder block over these pre-installed studs, using them as alignment guides. This technique prevents misalignment issues that could compromise the engine’s structural integrity. The center stud method provides consistent reference points throughout the assembly process, maintaining the vital parallel and perpendicular relationships between mating surfaces. This systematic approach assures long-term stability and proper load distribution across the cylinder block assembly.

Cleaning and Degreasing Techniques

effective cleaning methods explained

Proper cleaning and degreasing of a steam engine cylinder block requires a systematic approach using multiple techniques. Before applying any cleaning methods or degreasing agents, make sure you’re wearing protective gear and position the block in a ventilated area with proper drainage. High-pressure washing effectively removes residual machining debris and contaminants.

Start with mechanical debris removal using appropriate brushes – soft-bristled brass for aluminum blocks and wire brushes for other materials. You’ll need to:

  • Remove all plugs to access internal galleries and passages
  • Apply compressed air to flush out loose particles and debris
  • Use specialized solvents or degreasers to dissolve stubborn residues
  • Implement steam cleaning or ultrasonic baths for deep contamination

After thorough cleaning, dry the block completely using compressed air or lint-free cloths. Apply a corrosion inhibitor to protect bare metal surfaces from oxidation. Complete a detailed inspection of all passages and interfaces to verify complete contaminant removal before proceeding with further maintenance steps.

Valve System Maintenance

To maintain ideal valve performance in steam engine systems, you’ll need to implement an extensive maintenance protocol that addresses five critical areas: lubrication, sizing, installation, overhaul schedules, and leakage control. Apply valve lubrication techniques every 2-3 hours using high-temperature steam oil additives, guaranteeing precise displacement for small engines and forced systems for larger units. Regular visual checks of valve settings and timing help optimize steam distribution to cylinders.

Maintenance TaskFrequencyCritical Checks
Valve InspectionEvery 500 cyclesSurface wear, alignment
Seal ReplacementQuarterlyLeakage rates, gasket integrity
Material TestingBi-annuallyCorrosion, steam compatibility
Valve System Maintenance

Your valve material selection must comply with ASME/API guidelines, prioritizing corrosion-resistant alloys for high-temperature operations. Install expansion joints where thermal movement occurs, and verify orientation before final assembly. Document all maintenance activities, including cycles and replacements, while maintaining Class IV or higher leakage standards. Test calibration after each maintenance session to guarantee precision and leak-free performance.

Common Defects and Repair Solutions

defects and repair strategies

Steam engine cylinder blocks exhibit five primary categories of defects that require specific repair protocols. Understanding these cylinder block failures and implementing proper maintenance strategies can prevent catastrophic damage. You’ll need to watch for these common issues:

  • Blocked drainage passages leading to water retention and internal rusting
  • Worn cylinder liners caused by inadequate lubrication or contamination
  • Failed head gaskets resulting from thermal stress or improper installation
  • Damaged bearings due to misalignment or debris accumulation

When addressing these defects, start with precision diagnostics using oil injection tests and torque measurements. Clear any blocked drains using specialized drilling tools, replace worn liners through proper re-boring procedures, and guarantee correct gasket installation with appropriate torque sequences. For bearing issues, replace damaged components and verify proper alignment. Remember to perform post-repair testing, including leak checks with dyed coolant and thorough bearing clearance measurements.

Performance Testing and Validation

When validating steam engine cylinder performance, you’ll need to collect precise metrics through a combination of modern instrumentation and standardized testing protocols. Use digital data loggers to capture real-time pressure traces and analyze cycle-to-cycle variations between cylinders.

Test TypeKey MetricsRequired Tools
CompressionClearance volume, ring sealPressure gauges, leak testers
ExpansionPower output, PPMDigital loggers, dyno
ThermalHot spots, expansionInfrared sensors, temp probes
FlowValve timing, mixtureFlow meters, timing lights

Conduct leak-down testing using compressed air through inlet/outlet cocks to verify piston ring and valve sealing integrity. Monitor for blowby noise in exhaust that indicates steam bypassing seals. When implementing configuration changes like multi-stage expansion ratios, perform systematic load testing under simulated operating conditions. Document all performance metrics for comparative analysis and iterative improvements to cylinder block efficiency.

Performance Testing and Validation

You may also like to read – 5 Expert Tips: Clean Vintage Steam Engine Passages

Frequently Asked Questions

How Often Should Steam Engine Cylinder Blocks Be Replaced Under Normal Conditions?

Like clockwork ticking away the miles, you’ll need to keep a sharp eye on your cylinder block’s replacement frequency. For freight operations, you’re looking at replacements every 100,000-150,000 service miles. If you’re running passenger service, you can stretch those maintenance intervals to 150,000-200,000 miles, thanks to lighter loads and better lubrication practices. Don’t forget that extreme conditions may demand earlier intervention.

Can Modern Synthetic Lubricants Be Safely Used in Historic Steam Engines?

You’ll need to carefully evaluate synthetic lubricants before using them in historic steam engines. While synthetic advantages include better heat resistance and longer service life, vintage compatibility remains a major concern. Start by testing synthetics on non-critical components, using a 5-10% blend ratio with traditional oils. Monitor seal conditions, steam wash-off rates, and emulsification behavior over 100-200 operating hours before considering full adoption.

What Are the Signs of Impending Cylinder Block Failure?

When performing cylinder block inspection, you’ll notice several critical failure indicators: milky oil showing coolant contamination, persistent coolant loss without visible leaks, and white exhaust smoke. You’ll detect overheating despite proper maintenance, rough idling, and unusual knocking sounds. Watch for crusty deposits under the engine, pressure test failures, and oil-contaminated coolant passages. These symptoms typically appear 2-3 months before catastrophic failure.

Is It Possible to Retrofit Modern Sealing Materials to Vintage Cylinders?

Just like upgrading a classic car’s rubber seals to modern synthetics, you can retrofit vintage cylinders with contemporary sealing materials. You’ll need to carefully match material coefficients – pairing carbon PTFE rings with cast iron works well, while stainless steel requires special nitriding coatings. Consider hydraulic cylinder seals for smaller bores, and spiral-wound gaskets with PTFE fillers for high-temperature applications. Always maintain original clearances when adapting modern sealing techniques.

How Do Environmental Factors Affect Cylinder Block Maintenance Schedules?

You’ll need to adjust your maintenance schedule based on your operating environment. In high-heat climates, check coolant levels every 30 days instead of quarterly. Coastal or humid areas require rust inspections every 60 days due to increased corrosion risks. Dusty conditions demand monthly air filter changes and oil analysis every 3,000 miles. During freezing weather, inspect antifreeze concentration weekly to prevent block damage.

5 Expert Tips: Clean Vintage Steam Engine Passages

5 Expert Tips: Clean Vintage Steam Engine Passages

You’ll need to carefully clean vintage steam engine passages using specialized techniques to protect their historical integrity. Start with a gentle baking soda-vinegar paste for surface cleaning, then employ steam cleaning with deionized water for deeper passages. Use proper PPE and guarantee systems are de-energized before inspection. Apply non-abrasive cleaners and protect sensitive components with barriers. Regular maintenance and proper documentation will help preserve these engineering marvels for years to come.

Key Takeaways

  • Create a baking soda and vinegar paste for gentle cleaning of delicate vintage passages without causing damage to historic materials.
  • Use professional steam cleaners with adjustable pressure controls and deionized water to prevent mineral deposits in passages.
  • Employ mechanical tools like angled bristle brushes combined with water-based detergents for effective passage cleaning.
  • Cover sensitive components with protective barriers and use non-abrasive cleaners to preserve historic materials during cleaning.
  • Conduct thorough post-cleaning inspections of passages and apply rust-inhibiting treatments to protect cleaned surfaces.

Expert Cleaning Solutions for Vintage Steam Passages

vintage steam passage cleaning

When restoring vintage steam engines, selecting the right cleaning solutions is essential for preserving their historical integrity while ensuring ideal functionality. You’ll want to focus on eco-friendly products that effectively remove buildup without compromising the metal surfaces.

Start with a gentle baking soda-vinegar paste for initial surface cleaning techniques. This natural abrasive lifts accumulated grime while maintaining the engine’s patina. For sanitization, apply hydrogen peroxide, which breaks down residue without leaving corrosive byproducts. Steam cleaning provides another chemical-free option, penetrating deep into narrow passages to dislodge stubborn debris. Following the principles of sustainable pH-balanced solutions, these gentle cleaners prevent damage from harsh chemicals while preserving delicate surfaces.

Consider using white vinegar (demuncéd spirits) to dissolve organic deposits, especially in hard-to-reach areas. When tackling tougher buildup, chemical citrus extracts offer a corrosion-resistant alternative to harsh cleaners. Remember to avoid bleach or ammonia-based products, as they’ll accelerate oxidation and potentially damage historical components.

Safe Steam Passage Inspection and Preparation

Before conducting any steam passage maintenance, you’ll need to perform a thorough safety inspection to protect both yourself and the vintage equipment. Start by donning proper PPE, including heat-resistant gloves and eye protection, then verify all pressure systems are fully de-energized. Regular testing schedule can help identify potential failures early through sound-based diagnostic tools.

Your inspection techniques should follow a systematic approach. Use thermocouples to measure inlet temperatures and identify potential blockages. Deploy ultrasonic detectors above 25 kHz to locate steam leaks, placing probes directly on trap discharge orifices for accurate readings. Check for visible corrosion, erosion, or damage to seat valves that could compromise system integrity.

Follow safety protocols by documenting existing trap configurations and discharge cycles. Test backpressure using strategically placed gauges, and verify proper trap installation alignment. Monitor condensate discharge rates during operation to identify any undersized traps, and scan surfaces for temperature anomalies that might indicate hidden issues.

Proper Cleaning Tools and Equipment Selection

effective cleaning tool selection

Three essential categories of cleaning tools are necessary for maintaining vintage steam engine passages: specialized steam cleaning equipment, mechanical implements, and precision drying systems. For effective cleaning techniques, you’ll need a professional-grade steam cleaner like the Derotor model, featuring adjustable pressure controls and safety features including thermostatic cut-offs.

With 3-5 bar pressure, the steam cleaner effectively removes ingrained dirt and residue from cracks and textured surfaces. Your equipment maintenance should include using deionized water to prevent mineral buildup in steam cleaners. For stubborn deposits, combine mechanical tools such as angle bristle brushes and nylon scrubbers with water-based detergents and washing soda. Avoid petroleum-based solvents, which perform poorly on encrusted residues.

After cleaning, employ pressurized water for thorough rinsing, followed by controlled drying methods. Use air compressors or heat lamps to prevent oxidation, but avoid direct sunlight exposure. For ongoing protection, store cleaned components with desiccant packs to maintain stable humidity levels.

Historic Material Protection During Cleaning

Proper protection of historic materials during steam engine cleaning requires meticulous attention to surface preservation techniques. You’ll need to implement specific material preservation strategies that prevent damage while maintaining the engine’s historic integrity. Start by covering all sensitive components with protective barriers like plastic sheeting or foil, especially around electrical elements and delicate mechanical parts.

Historic Material Protection During Cleaning

When applying historic cleaning techniques, use only non-abrasive cleaners that won’t scratch or deteriorate vintage surfaces. Regular inspections during cleaning help identify potential hazards and ensure safety protocols are followed. You’ll want to avoid harsh chemicals and petroleum-based products that could react with original materials. Instead, focus on gentle, regular dusting to prevent buildup that might require more aggressive cleaning later. Shield any exposed metal surfaces by applying appropriate rust-inhibiting treatments after cleaning. Remember to protect intercooler fins with cardboard sheets and secure all electrical connections before beginning any moisture-based cleaning processes. This methodical approach guarantees you’re preserving the engine’s historic value while achieving necessary cleanliness.

Post-Cleaning Validation and Maintenance Steps

validation and maintenance procedures

Successful steam engine cleaning requires thorough post-cleaning validation and systematic maintenance procedures. Your post cleaning checks should start with inspecting boiler walls for scale and cracks, followed by verifying valve settings with specialized tools. Confirm you’re testing injector clack function and confirming fire tubes are debris-free using appropriate flue brushes.

Implement maintenance protocols by applying high-temperature steam oil to moving parts every 2-3 operational hours. You’ll need to use anti-seize compound on injector clack threads and protect bright steel components with 3-in-1 oil. Using distilled water only prevents harmful mineral buildup that can damage internal components over time. After cleaning, resume operation at low pressure to monitor steam flow efficiency and verify blast pipe integrity.

Track your work by updating valve adjustment logs and recording injector clack cleaning intervals. Don’t forget to schedule regular ash removal cycles and purge mechanical lubricator oil circuits to prevent sludge buildup. Cross-check water gauge accuracy with manual measurements to confirm proper calibration.

You may also like to read – Restore Steam Locomotive Cylinders: Expert Repair Guide

Frequently Asked Questions

How Often Should I Replace Cleaning Brushes Used for Steam Passages?

You’ll need to replace your cleaning brushes based on both cleaning frequency and brush maintenance practices. Replace brushes after 5-7 cleaning cycles, or sooner if you notice frayed bristles, bent shapes, or reduced cleaning effectiveness. You should inspect bristles before each use, looking for material fatigue, structural damage, or poor fit. High-temperature applications and harsh conditions will accelerate wear, requiring more frequent replacements.

Can Ultrasonic Cleaning Methods Damage Historic Steam Engine Components?

While 85% of historic engine damage occurs from aggressive manual cleaning, ultrasonic cleaning is generally safe for vintage components when proper precautions are taken. You’ll need to control frequency settings (keeping below 40 kHz), seal critical openings, and limit exposure times to 15-20 minutes. For historic preservation, remove plastic parts first and use mild, ammonia-based solutions rather than harsh solvents that could compromise material integrity.

What’s the Ideal Storage Temperature for Cleaned Vintage Steam Engines?

You’ll want to maintain your vintage steam engine in a controlled environment between 15-25°C (59-77°F), with ideal humidity below 50%. These storage conditions prevent thermal stress on metal components and minimize corrosion risks. It’s essential to avoid temperature fluctuations that can cause expansion and contraction of materials. Consider using climate-controlled spaces with dehumidifiers to maintain consistent conditions year-round.

How Do Seasonal Temperature Changes Affect Steam Passage Cleaning Requirements?

Like a temperamental artist, your steam engine demands different care across seasons. Temperature fluctuations greatly impact cleaning effectiveness – summer heat accelerates oxide formation and grime buildup, requiring more frequent maintenance, while winter’s chill promotes condensation and slows chemical reactions. You’ll need to adjust your cleaning schedule, with special attention to corrosion risks during humid shifting periods and protective measures against thermal stress.

Should Different Cleaning Schedules Be Followed for Displayed Versus Operational Engines?

You’ll need distinctly different cleaning schedules for displayed versus operational engines. For displayed engines, limit cleaning to quarterly gentle maintenance using soft brushes and mild detergents to preserve finishes. Operational engines require more frequent attention – typically monthly deep cleaning with degreasers and steam integration to prevent buildup that could affect performance. Balance preservation needs with functional requirements based on each engine’s primary purpose.

Translate »